With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Food-grade salt powder conveying systems are specialized industrial equipment designed to handle and transport salt in its powdered form. These systems are crucial in various industries, including food processing, chemical manufacturing, and pharmaceuticals, where the integrity and purity of the salt are paramount. The equipment must adhere to strict sanitary standards to ensure that the salt remains free from contaminants and maintains its quality throughout the conveying process. This article will explore the components, operational principles, and design considerations of such systems, providing a comprehensive understanding of their functionality and importance in industrial applications. Systems like these are often engineered by companies such as Shandong HeadPowder Engineering Co., Ltd., which focuses on creating solutions that meet the rigorous demands of the food industry.
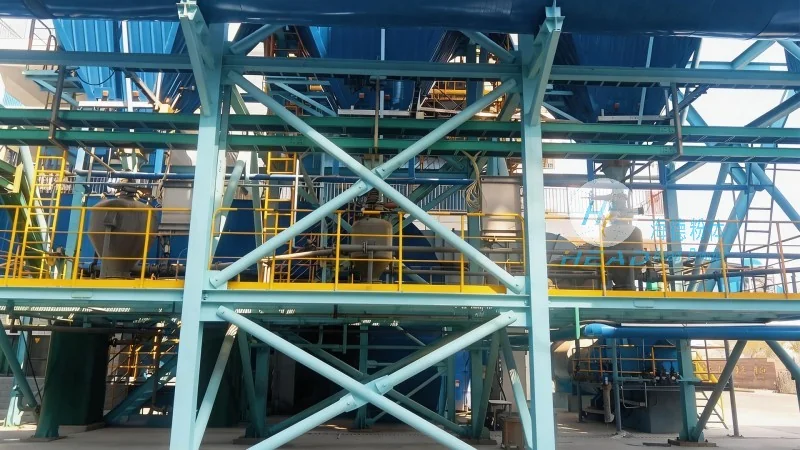
The core components of a food-grade salt powder conveying system typically include a hopper for material storage, a feeder to control the flow rate, a conveyor mechanism (such as a screw conveyor, pneumatic conveyor, or bucket elevator), and a control system to regulate the operation. The hopper is designed with smooth, non-porous surfaces to prevent material buildup and contamination. The feeder, often a rotary valve or a vibratory feeder, ensures a consistent and controlled discharge of the salt powder. The conveyor mechanism is the heart of the system, responsible for transporting the salt from the hopper to the processing or packaging area. For food-grade applications, materials like stainless steel (grade 304 or 316) are commonly used for all components to meet hygiene and safety requirements. This is a standard practice in equipment manufactured by companies like Shandong HeadPowder Engineering Co., Ltd., which prioritizes material quality and durability in its products.
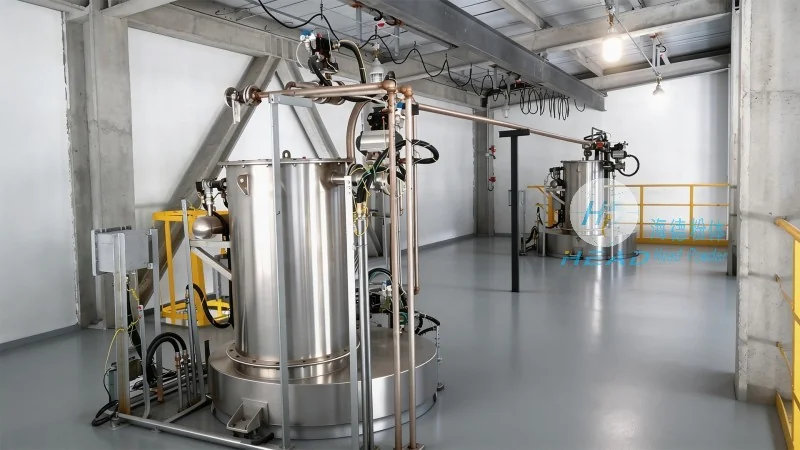
The design of a food-grade salt powder conveying system is guided by several key principles aimed at maximizing efficiency, minimizing product degradation, and ensuring compliance with regulatory standards. One of the primary design considerations is the prevention of material bridging and agglomeration in the hopper. This is achieved through the use of hopper designs with sloped walls and sometimes internal agitators or vibrators that help break up clumps and ensure uniform material flow. The feeder is designed to provide a consistent flow rate, which is critical for maintaining the performance of downstream equipment, such as mixers or packaging machines. The conveyor mechanism must be capable of handling the specific characteristics of salt powder, including its density, flowability, and potential for dust generation. For example, pneumatic conveying systems use air to transport the powder, which can be more efficient for long-distance transport but requires careful control of air pressure and flow to prevent product degradation or loss. Mechanical conveyors, like screw conveyors, are often preferred for short-distance transport within a facility due to their simplicity and reliability.
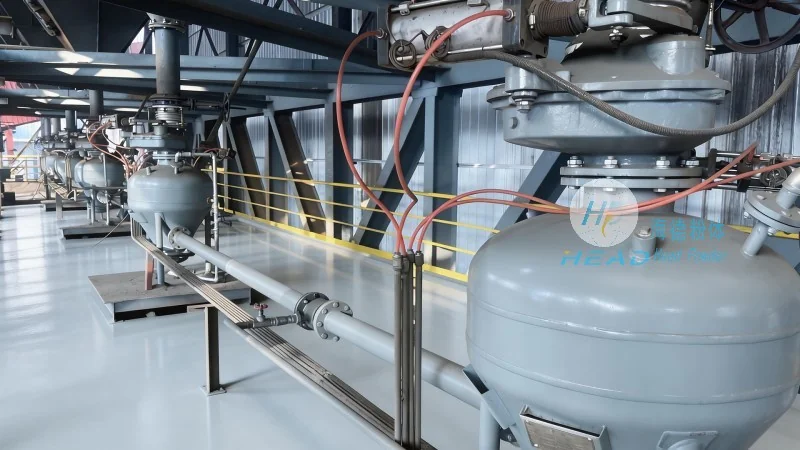
Modern food-grade salt powder conveying systems incorporate advanced control and monitoring systems to ensure optimal performance and compliance with industry standards. These systems typically include sensors for level measurement in the hopper, flow rate monitoring at the feeder, and pressure monitoring in pneumatic conveyors. The control system may be a programmable logic controller (PLC) that automates the operation of the feeder and conveyor, adjusting the flow rate based on real-time demand. This automation helps maintain consistent product quality and reduces the risk of overfilling or underfilling, which can affect downstream processes. Additionally, the system may include alarms and safety interlocks to prevent accidents, such as overpressure or material blockages. The control panel is usually located in a clean, easily accessible area, allowing operators to monitor the system's status and make adjustments as needed. Regular maintenance of these control systems is essential to ensure their reliability and longevity.
In the context of food processing, the efficient handling of salt powder is critical for maintaining product quality and operational efficiency. The conveying system must be integrated with other processing equipment, such as mixers, granulators, or packaging machines, to ensure a seamless flow of materials. The design of the system must consider the compatibility with these downstream processes, including the required flow rates, particle size distribution, and moisture content of the salt. For example, if the salt is to be used in a food product that requires a specific particle size, the conveying system must be designed to maintain that size distribution without causing further breakdown or agglomeration. The system may also include features like dust collection and filtration to prevent airborne contamination and protect the environment and personnel. These features are essential for meeting environmental regulations and maintaining a safe working environment.
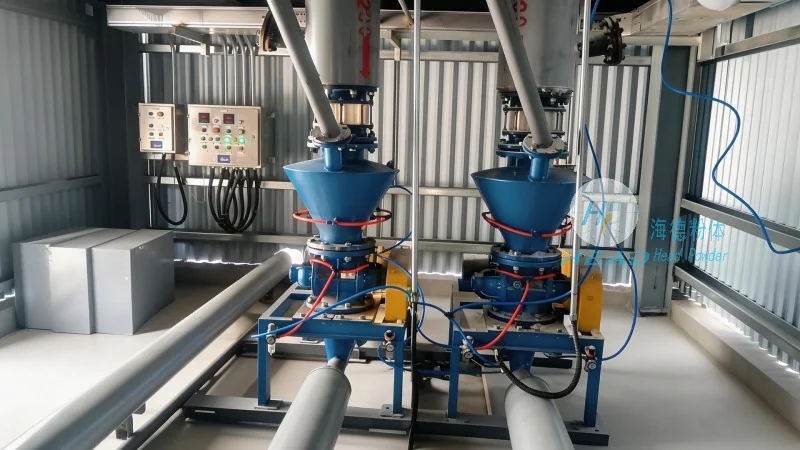
Food-grade salt powder conveying systems are essential equipment in industries where the quality and purity of salt are critical. The design of these systems must prioritize hygiene, efficiency, and compliance with regulatory standards. By incorporating specialized components, such as stainless steel construction, controlled feeding mechanisms, and advanced control systems, manufacturers can ensure that the salt is transported safely and effectively. The choice of conveyor type (pneumatic or mechanical) depends on the specific application requirements, including distance, flow rate, and material characteristics. Overall, a well-designed food-grade salt powder conveying system is a vital component of any industrial process that involves the handling of salt powder, contributing to product quality, operational efficiency, and regulatory compliance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top