With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
When it comes to handling and transporting bulk materials like sulfamyl ammonium, specialized equipment is essential to ensure efficiency, safety, and reliability in industrial operations. A sulfamyl ammonium powder conveying system equipment is a critical component in processes where this chemical is used, offering a solution to the challenges of moving fine powders over long distances or within complex production lines.
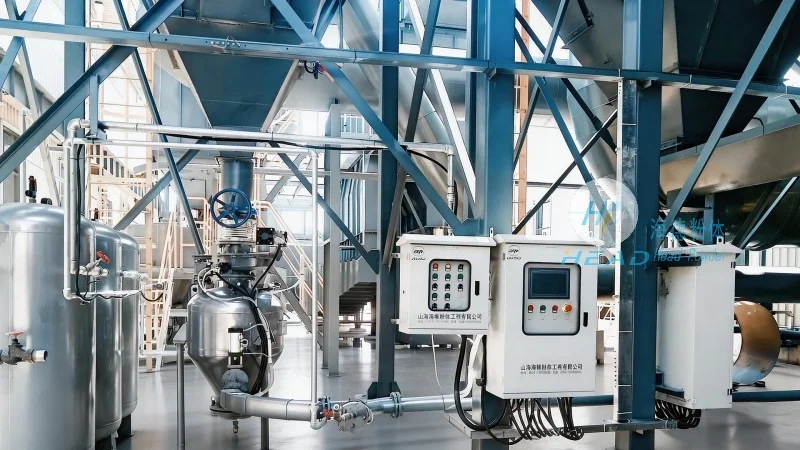
The sulfamyl ammonium powder conveying system equipment is designed to handle the unique properties of sulfamyl ammonium, a white crystalline powder commonly used in agriculture and industry. This system is engineered to address issues such as dust generation, material segregation, and the need for gentle handling to prevent product degradation. By integrating various components, the system ensures that the material is transported smoothly from the source to the destination without compromising quality or safety.
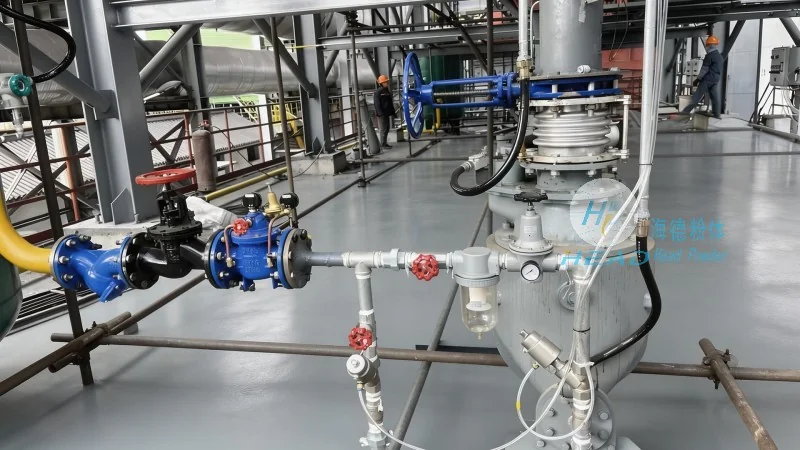
The core of a sulfamyl ammonium powder conveying system typically includes several key components that work in tandem to achieve efficient material transport. These components may include a hopper for material storage, a feeder to control the flow rate, a conveyor system (such as a screw conveyor or pneumatic conveyor) to move the powder, and a control system to monitor and adjust the operation. Each component plays a vital role in maintaining the integrity of the sulfamyl ammonium and ensuring the system operates within safe parameters.
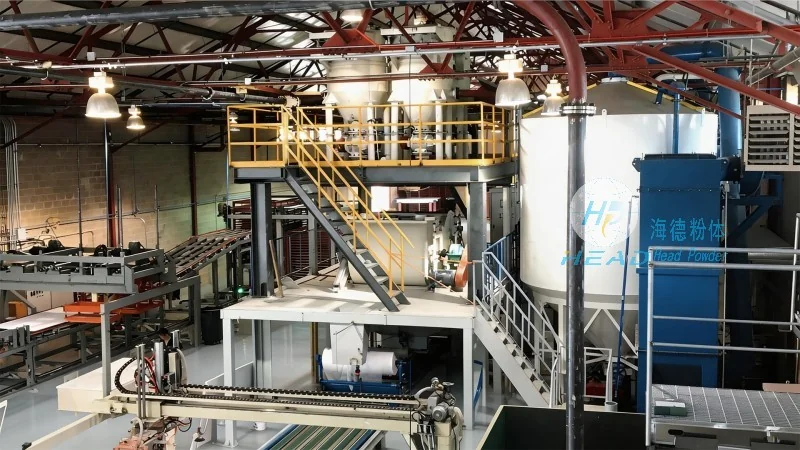
The design principles of a sulfamyl ammonium powder conveying system are centered on several key factors that address the specific requirements of handling this material. Firstly, the system must minimize dust generation to comply with environmental regulations and ensure worker safety. This is often achieved through sealed housing and proper ventilation systems. Secondly, the equipment is designed to prevent material segregation, which can occur when different particle sizes or densities are present. By using consistent flow rates and gentle handling mechanisms, the system maintains the uniformity of the sulfamyl ammonium. Thirdly, the design prioritizes energy efficiency and low maintenance to reduce operational costs and downtime. The use of durable materials and robust construction ensures the system can withstand the abrasive nature of the powder and operate reliably over extended periods.
Sulfamyl ammonium powder conveying systems are widely used in various industries, including agriculture, chemical manufacturing, and food processing. The primary benefits of these systems include improved process efficiency, reduced labor costs, and enhanced safety. By automating the material handling process, companies can increase production throughput while minimizing the risk of accidents or product contamination. Additionally, the systems help maintain the quality of the sulfamyl ammonium by preventing exposure to moisture, air, or other contaminants during transport.
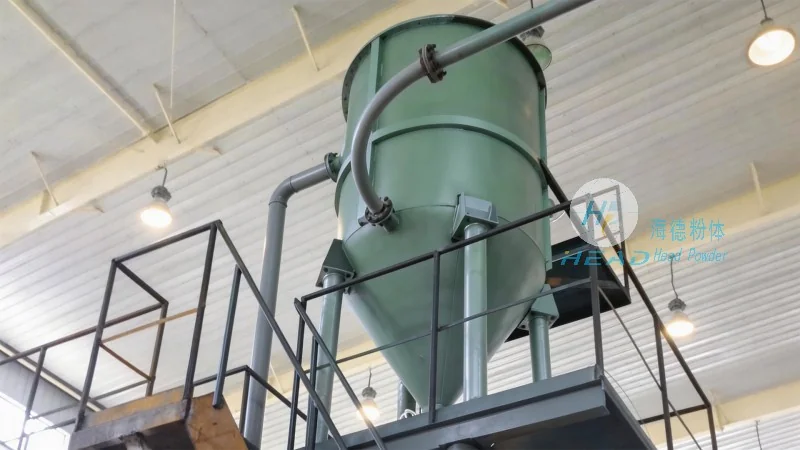
As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and producing high-quality sulfamyl ammonium powder conveying systems. With years of experience and a commitment to innovation, the company has developed advanced solutions tailored to the specific needs of its clients. HeadPowder's systems are known for their reliability, efficiency, and adherence to industry standards. The company's headquarters is located in Shandong, China, where it continues to invest in research and development to stay at the forefront of powder handling technology.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top