

Working Principle and Features of Dust-Free Metering Pneumatic Conveying Systems
The dust-free metering pneumatic conveying system is a sophisticated industrial solution designed to transport bulk materials with high precision and minimal contamination. This technology is crucial in industries where material purity and consistent flow control are paramount, such as pharmaceuticals, food processing, and chemical manufacturing. The system operates by combining air flow with a metering mechanism to ensure accurate material delivery while maintaining a clean environment.
Working Principle of the Dust-Free Metering Pneumatic Conveying System
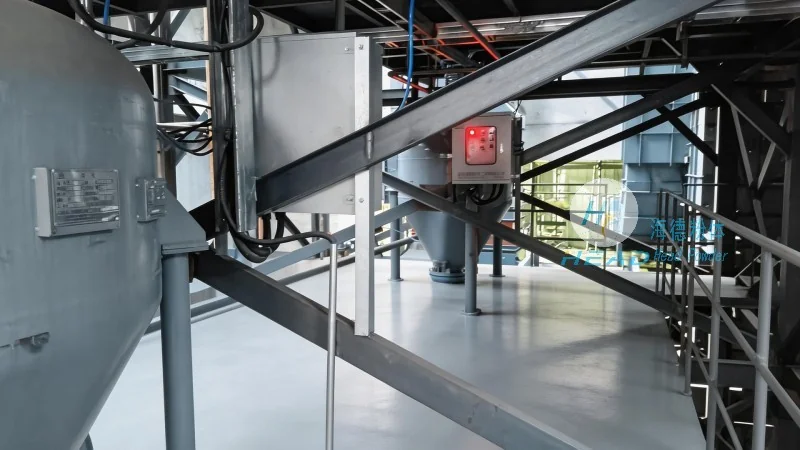
The core working principle of the dust-free metering pneumatic conveying system involves the use of a controlled air stream to transport dry bulk materials through a sealed pipeline. The system typically consists of a hopper for material storage, a metering device (often a rotary valve or screw feeder) to regulate the material flow rate, and a pneumatic conveyor that uses compressed air to move the material. The metering device ensures that the material is fed at a consistent rate, preventing overloading or underfeeding, which could lead to uneven flow or contamination. The air flow is managed by a blower or compressor, providing the necessary pressure to move the material through the system. The sealed design of the pipeline and components prevents dust and particles from escaping into the environment, maintaining a clean and safe working area. The system operates in a closed loop, ensuring that all material and air are contained within the system, preventing any leakage or contamination. The metering device, typically a rotary valve or a screw feeder, is integrated with the hopper to control the rate at which material is fed into the conveyor. This device is calibrated to deliver a precise amount of material per unit time, which is crucial for applications that require exact measurement, such as in the pharmaceutical industry where dosage accuracy can impact product efficacy.
Key Features and Advantages of the System
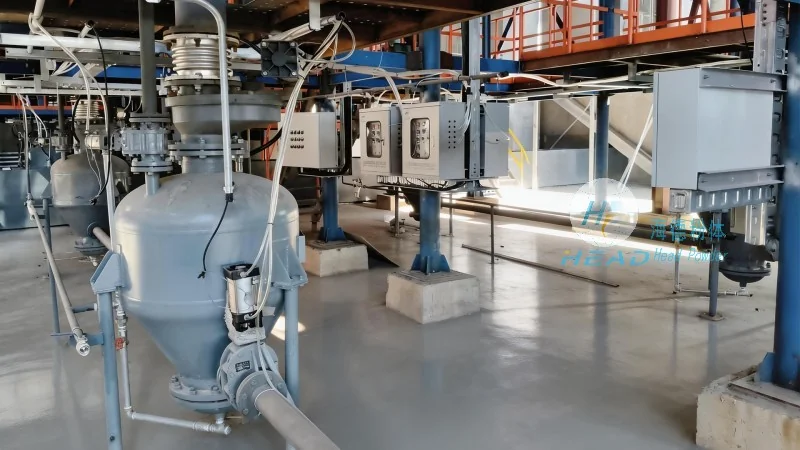
Key features of this system include high precision in material measurement, which is essential for applications requiring exact dosing, such as in pharmaceutical production where dosage accuracy is critical. The dust-free design minimizes the risk of product contamination, making it suitable for industries with strict hygiene standards. Additionally, the system offers flexibility in material handling, as it can transport various types of dry bulk materials, including powders, granules, and fine particles. The metering mechanism allows for adjustable flow rates, enabling users to control the amount of material being conveyed in real-time. Another advantage is the reduced maintenance requirements compared to traditional mechanical conveyors, as the system has fewer moving parts and is less prone to wear and tear. The system also offers energy efficiency, as the air flow is optimized to minimize energy consumption while maintaining the required conveying speed. The sealed pipeline and components are constructed from materials that are resistant to corrosion and wear, ensuring long-term performance and reliability.
Application Scenarios and Benefits
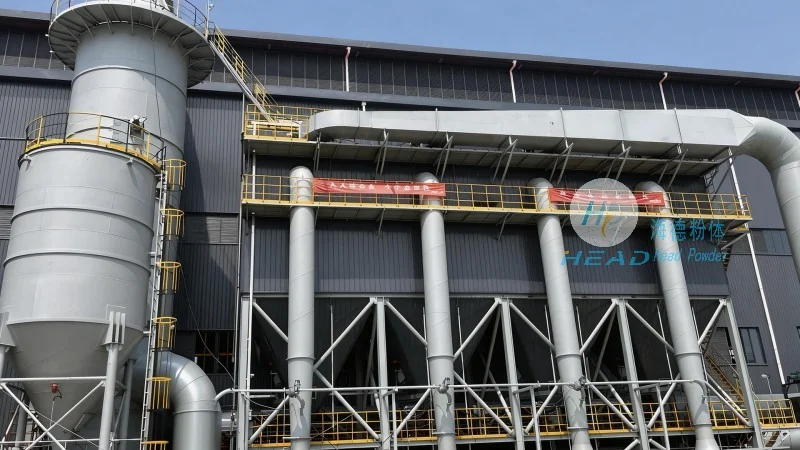
The dust-free metering pneumatic conveying system is widely used in various industries due to its ability to handle sensitive materials without contamination. In the pharmaceutical industry, it is used to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the final dosage is accurate and consistent. In the food processing industry, it is used to convey ingredients like flour, sugar, and spices, maintaining the purity and quality of the products. In the chemical manufacturing industry, it is used to transport powders and granules, preventing dust and chemical exposure to the environment and personnel. The benefits of using this system include improved product quality, reduced waste, and enhanced operational efficiency. The system's ability to maintain a clean environment also helps in meeting regulatory requirements and maintaining compliance with industry standards.
About Shandong HeadPowder Engineering Co., Ltd.
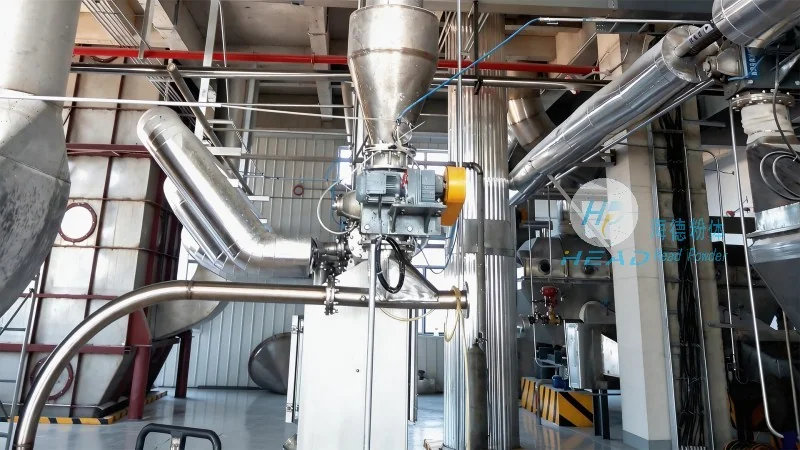
As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in developing and supplying advanced dust-free metering pneumatic conveying systems. With years of experience in the industry, the company has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. The company's headquarters is located in Shandong, China, where its team of engineers and technicians work tirelessly to innovate and improve their products. HeadPowder's commitment to quality and customer satisfaction is reflected in the robust design and durability of their systems, which are built to withstand the demands of various industrial environments. The company's products are manufactured using advanced production techniques and quality control measures, ensuring that each system meets the highest standards of performance and durability. HeadPowder's after-sales service and technical support are also a key part of its customer-centric approach, providing clients with the necessary assistance to operate their systems effectively and efficiently.