

Working Principle and Features of Warehouse Bottom Air Conveying Lines
Warehouse bottom air conveying lines represent a sophisticated solution for material handling in industrial and logistics environments. These systems are designed to efficiently transport bulk materials from storage areas to processing or packaging stations, leveraging air pressure to move items through a network of pipes and ducts. The technology is particularly valuable in settings where traditional conveyor systems may be impractical due to space constraints or the nature of the materials being handled.
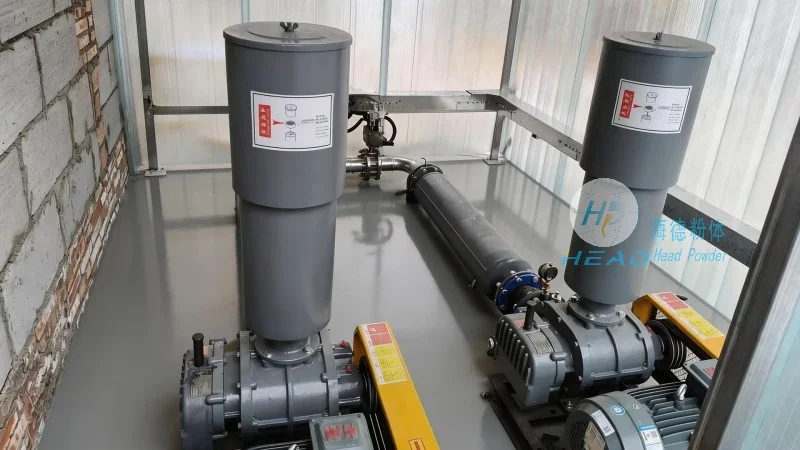
Working Principle of Warehouse Bottom Air Conveying Lines
The core mechanism of warehouse bottom air conveying lines revolves around the use of a positive pressure system. A blower or fan generates compressed air, which is then distributed through a network of pipes embedded in the floor or ceiling of the warehouse. As air flows through the system, it creates a pressure differential that propels materials, such as powders, granules, or small parts, from the loading point to the discharge point. The system typically includes components like airlocks, filters, and control valves to regulate airflow and ensure consistent material transport. The bottom air design allows for seamless integration with existing warehouse infrastructure, minimizing the need for extensive modifications to the facility layout.
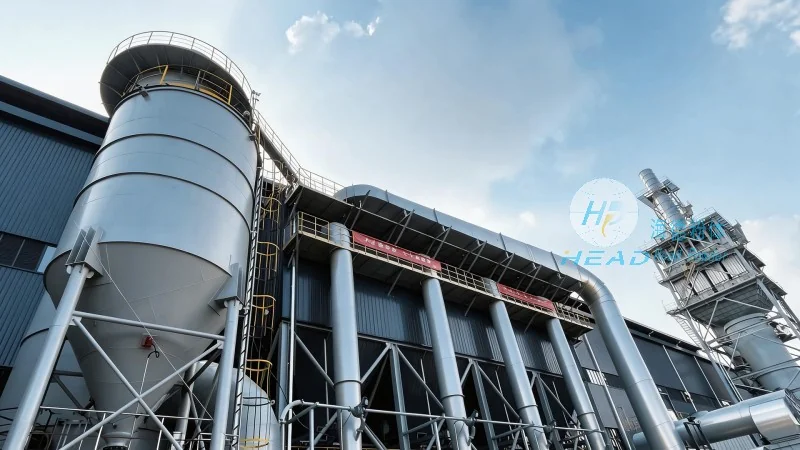
Key Features of Warehouse Bottom Air Conveying Lines
Several distinctive features make warehouse bottom air conveying lines an attractive option for material handling applications. First, the system offers high flexibility in terms of layout and expansion. Since the conveying lines are often installed in the floor or under the ceiling, they can be easily reconfigured or extended without disrupting ongoing operations. This adaptability is crucial for businesses that experience changes in production volume or product lines. Second, the technology provides excellent material handling capabilities for a wide range of products, including fine powders, granules, and even small, irregularly shaped items. The air pressure ensures that materials are transported gently, reducing the risk of product degradation or damage. Third, the system is energy-efficient compared to traditional mechanical conveyors. By using compressed air, the system minimizes energy consumption while maintaining high throughput rates. Additionally, the bottom air design allows for low noise operation, which is beneficial in environments where noise control is a priority.
Applications and Benefits in Industrial Settings
Warehouse bottom air conveying lines are widely used in various industries, including pharmaceuticals, food processing, chemical manufacturing, and automotive parts production. In pharmaceutical facilities, for example, the system ensures that sensitive powders are handled hygienically and efficiently, meeting stringent regulatory requirements. In food processing plants, the technology allows for the safe and rapid transport of ingredients and finished products, maintaining product quality and freshness. The benefits of these systems extend beyond efficiency and flexibility; they also contribute to improved workplace safety by reducing the need for manual material handling, which can be physically demanding and prone to accidents. Furthermore, the compact design of the bottom air system helps to optimize warehouse space utilization, allowing for more efficient use of vertical and horizontal areas.
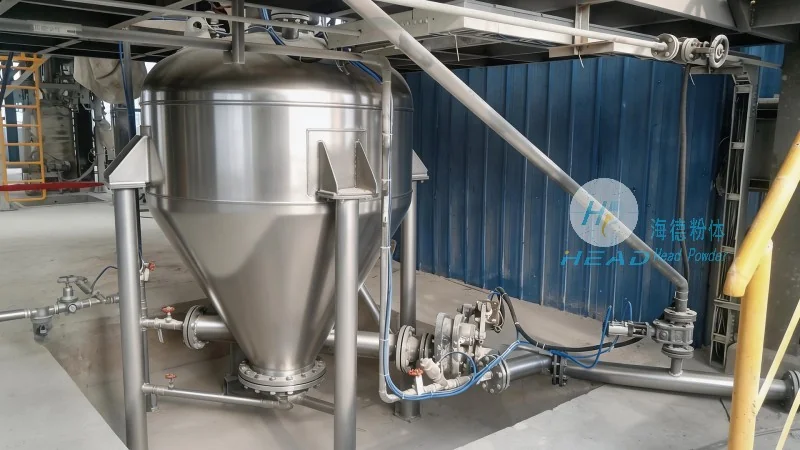
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of advanced material handling solutions. With a focus on innovation and customer-centric design, the company specializes in developing and manufacturing high-quality air conveying systems tailored to the specific needs of industrial clients. HeadPowder's expertise lies in integrating cutting-edge technology with practical application, ensuring that their products deliver reliable performance and long-term value. The company's commitment to quality is reflected in its adherence to international standards and rigorous testing protocols, which guarantee the durability and efficiency of its warehouse bottom air conveying lines. HeadPowder's team of engineers and technicians work closely with clients to understand their operational challenges and provide customized solutions that enhance productivity and reduce operational costs. Based in Shandong, China, the company leverages its local presence to offer timely support and service to its customers, reinforcing its reputation as a trusted partner in the material handling industry.