With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Water-in-powder pneumatic conveying equipment has become an essential solution in modern material handling, particularly for industries dealing with fine powders and granular materials. This technology offers a reliable and efficient method to transport bulk materials over long distances or within complex processing systems, ensuring minimal product degradation and operational safety.
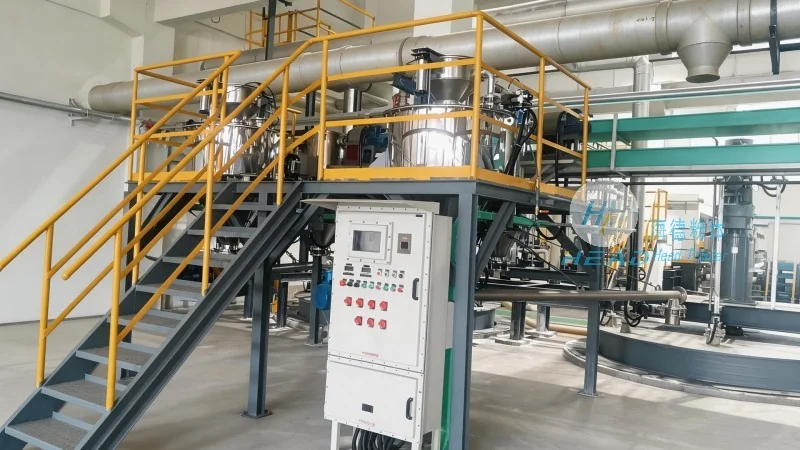
The fundamental principle of water-in-powder pneumatic conveying involves the integration of water and dry powder to create a slurry that is then transported through a pipeline using air pressure. This approach, also known as slurry pneumatic conveying, leverages the fluid properties of the slurry to enhance the conveying efficiency and reduce the risk of material segregation or caking. The process typically starts with the dry powder being mixed with water in a proportion that maintains the slurry's viscosity and flowability. The resulting mixture is then introduced into a high-pressure air stream, which propels the slurry through the conveying line. As the slurry travels, the air and water separate from the powder at the destination, allowing for the recovery of water for reuse and the collection of the dry powder in a controlled manner. This method is particularly effective for materials that are prone to dusting or clumping when handled dry, as the moisture content helps maintain particle integrity and prevents blockages in the pipeline.
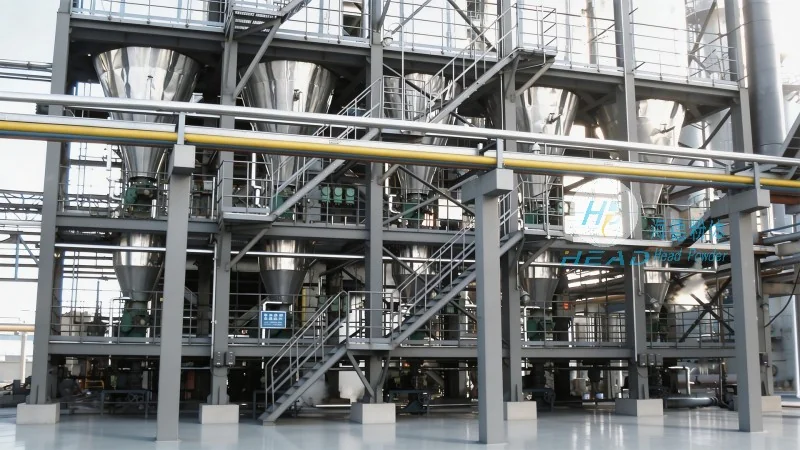
Water-in-powder pneumatic conveying equipment is widely used in various industrial applications, each presenting unique operational requirements that the technology addresses effectively. For instance, in the food and pharmaceutical industries, where product purity and hygiene are paramount, this equipment ensures that powders are transported without contamination or cross-contamination. The closed system design minimizes exposure to external elements, while the water recovery system allows for the reuse of water, reducing operational costs and environmental impact. In the chemical industry, it is commonly employed for transporting reactive powders or those that require controlled moisture levels to prevent chemical reactions during transport. The ability to adjust the water-to-powder ratio allows operators to tailor the conveying process to the specific characteristics of the material, ensuring optimal performance and product quality. Additionally, in the agricultural sector, this technology is used for handling fertilizers or animal feed, where the need to prevent dust dispersion and maintain material consistency is critical. The equipment's adaptability to different material types and processing conditions makes it a versatile solution across multiple sectors.
One of the primary advantages of water-in-powder pneumatic conveying is its ability to handle a wide range of materials, from fine powders to granules, with minimal maintenance and operational complexity. Unlike traditional dry pneumatic conveying systems, which may struggle with fine powders that tend to cause blockages or degrade over time, the slurry method provides a more stable and consistent flow. This leads to higher conveying efficiency and lower energy consumption, as the air pressure required to move the slurry is generally lower than that needed for dry powders. Furthermore, the closed-loop water system contributes to environmental sustainability by reducing water waste and enabling the recycling of water, which is especially beneficial in regions with water scarcity. The equipment also offers improved safety features, as the enclosed system prevents dust emissions and reduces the risk of explosions in areas where combustible materials are handled. Operators can easily monitor and control the conveying process through integrated sensors and control panels, ensuring precise management of the water-to-powder ratio and air pressure. This level of control not only enhances operational efficiency but also extends the lifespan of the equipment by minimizing wear and tear on components.
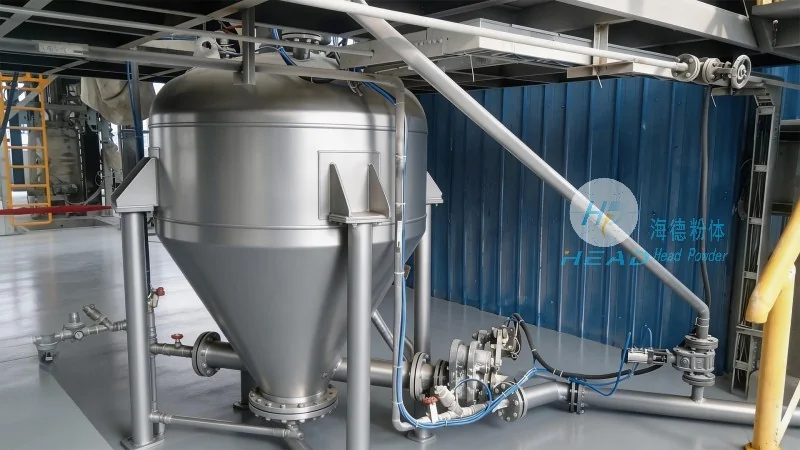
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer specializing in the design, development, and supply of advanced material handling solutions, including water-in-powder pneumatic conveying equipment. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for industries seeking reliable and efficient material transport systems. Headpowder's products are engineered to meet the diverse needs of various applications, ensuring compatibility with different material types and processing environments. The company's team of experts leverages extensive industry experience to provide customized solutions that enhance operational performance and reduce costs for clients. Headpowder's facilities, located in Shandong, China, are equipped with state-of-the-art technology and rigorous quality control measures, ensuring that each product meets the highest standards of performance and durability. The company's dedication to customer satisfaction and technological advancement has earned it a reputation for excellence in the material handling industry, making it a preferred choice for businesses looking to optimize their material transport processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top