With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding the sugar material handling system is crucial for optimizing operations in the sugar processing industry. Such systems are engineered to efficiently transport, store, and manage raw and processed sugar, ensuring smooth workflow and high productivity. This article explores the fundamental aspects of these systems, focusing on their design principles and the key components that contribute to their effectiveness.
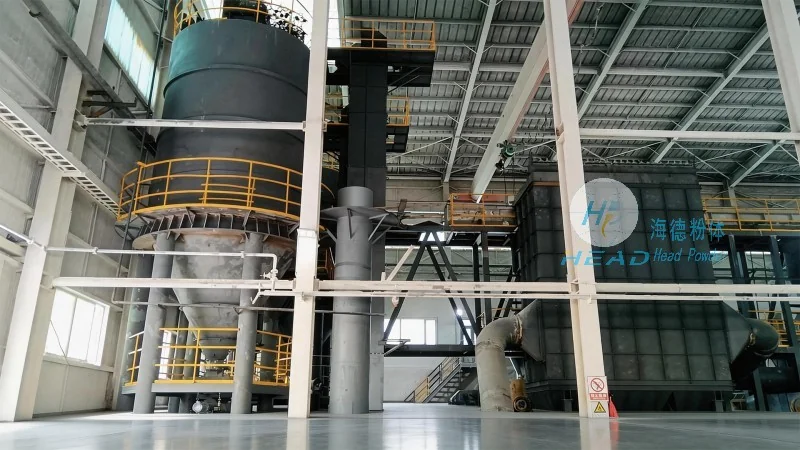
A sugar material handling system encompasses a range of equipment and processes designed to handle sugar from its raw form through various stages of processing and packaging. These systems are integral to sugar mills and refineries, where the efficient movement of sugar is essential to maintain production rates and quality standards. The system typically includes conveyors, elevators, storage silos, and control mechanisms that work in tandem to manage the flow of material.
The core components of a sugar material handling system are tailored to the specific needs of sugar processing. Conveyors, such as belt conveyors or screw conveyors, are commonly used to transport sugar horizontally or vertically. Elevators, including bucket elevators or chain conveyors, are employed to lift sugar from lower to higher levels, facilitating vertical movement within the facility. Storage silos or hoppers are used to store bulk sugar, ensuring a steady supply for processing. Additionally, control systems, including sensors and automation, monitor and regulate the flow of material to prevent bottlenecks and ensure safety.
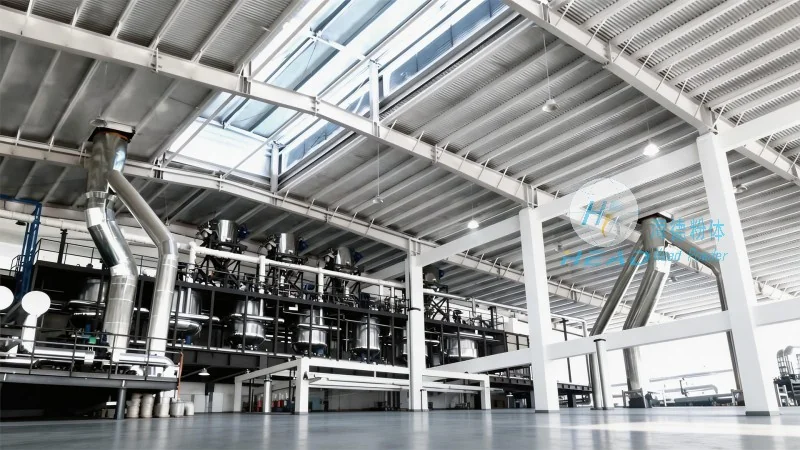
The design of a sugar material handling system is guided by several key principles aimed at maximizing efficiency, safety, and durability. First, the system must be designed to handle the specific physical properties of sugar, such as its granular nature and potential for caking. This involves selecting appropriate materials for conveyor belts and components that resist wear and tear from sugar particles. Second, the system should be modular and scalable, allowing for easy expansion or modification as production needs change. Third, safety is a paramount consideration, with features like emergency stop buttons, protective guards, and dust suppression systems integrated into the design.

Shandong HeadPowder Engineering Co., Ltd. specializes in providing comprehensive solutions for sugar material handling systems. With years of experience in the industry, HeadPowder understands the unique challenges of sugar processing and designs systems that meet the specific requirements of each client. The company’s approach focuses on integrating advanced technology with practical engineering to deliver reliable and efficient solutions. By leveraging their expertise, HeadPowder helps sugar mills improve operational efficiency, reduce downtime, and enhance overall productivity.
In conclusion, a sugar material handling system is a critical component of modern sugar processing operations. Its design, incorporating key principles of efficiency, safety, and adaptability, ensures that sugar can be handled effectively from raw material to final product. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in developing and implementing these systems, contributing to the success of sugar production worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top