

What is a Manganese Sulfate Material Handling System? What are its Design Principles?
For industrial operations dealing with manganese sulfate, an efficient material handling system is crucial for maintaining productivity and safety. This article explores the components and design principles of a manganese sulfate material handling system, highlighting how such systems are engineered to meet the specific demands of this chemical material.
Understanding Manganese Sulfate and Its Handling Requirements
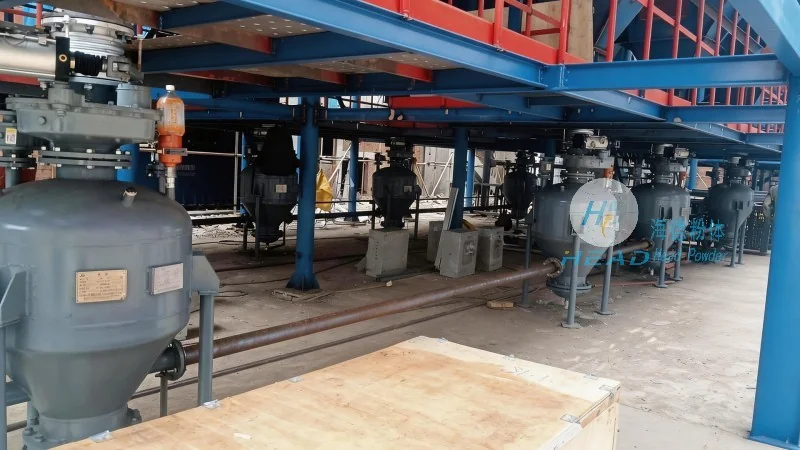
Manganese sulfate is a widely used chemical compound in various industries, including battery manufacturing, agriculture, and water treatment. Due to its granular or powder form, handling this material requires specialized equipment to ensure minimal dust generation, prevent material degradation, and maintain a safe working environment. The design of a material handling system for manganese sulfate must account for its physical properties, such as particle size, moisture content, and flow characteristics, to optimize the handling process.
Key Components of a Manganese Sulfate Material Handling System
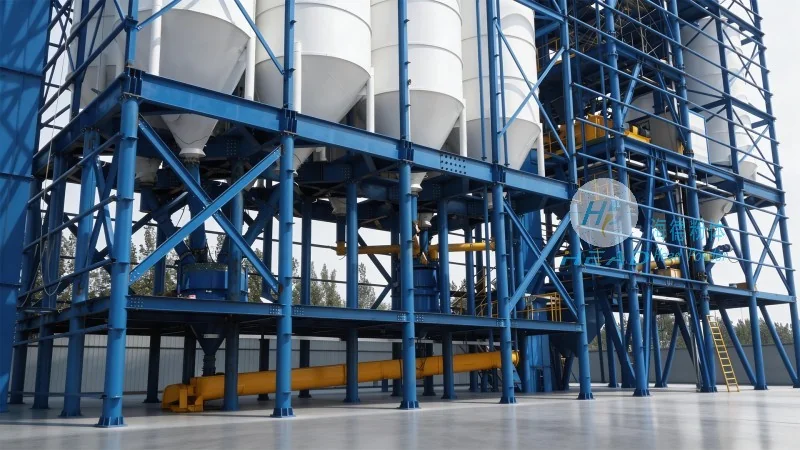
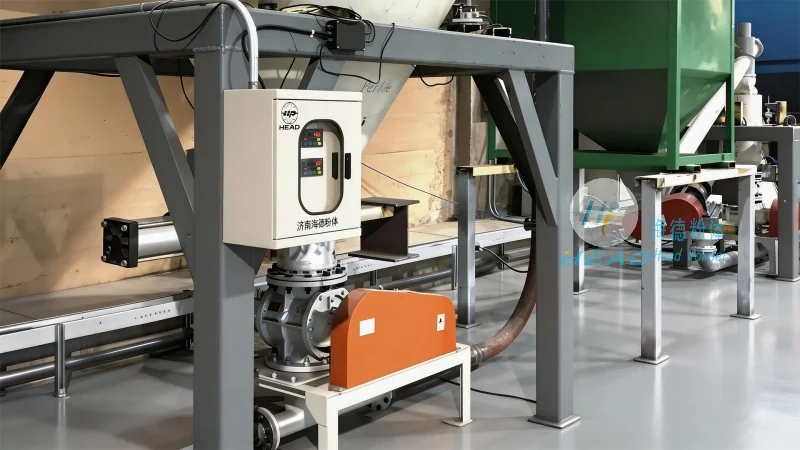
The core components of a manganese sulfate material handling system typically include feeders, conveyors, storage silos, and processing equipment. Each component plays a vital role in the seamless transfer of material from one stage to another. For instance, feeders are used to regulate the flow of material from storage silos to conveyors, ensuring consistent and controlled feeding. Conveyors, such as belt conveyors or pneumatic systems, transport the material to processing units or storage areas. Storage silos are designed to hold large quantities of manganese sulfate, providing a stable and controlled environment to prevent caking or segregation of the material.
Design Principles for Efficient Material Handling
The design of a manganese sulfate material handling system follows several key principles to ensure efficiency, safety, and durability. One of the primary principles is the minimization of material degradation. This is achieved through the use of appropriate equipment that reduces friction and impact during material transfer. For example, using flexible hoses or enclosed conveyor systems can prevent dust contamination and maintain the quality of the material. Another critical principle is the prevention of dust and fume generation. Manganese sulfate is a fine powder, and excessive dust can pose health risks and affect the performance of downstream processes. Therefore, dust collection systems and enclosed handling equipment are essential components of the design.
HeadPowder's Expertise in Manganese Sulfate Material Handling Systems
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing customized systems for handling manganese sulfate and other chemical materials. With years of experience in the industry, HeadPowder understands the unique challenges associated with handling manganese sulfate and has developed innovative solutions to address them. The company's team of engineers and technicians work closely with clients to assess their specific needs and develop tailored systems that meet their operational requirements. HeadPowder's systems are designed to be durable, efficient, and safe, ensuring that clients can handle manganese sulfate with minimal downtime and maximum productivity.
Conclusion: The Importance of a Well-Designed Material Handling System
In conclusion, a well-designed material handling system is essential for the efficient and safe handling of manganese sulfate. The system must be tailored to the material's properties and the specific requirements of the industrial process. By incorporating appropriate components and following sound design principles, such as minimizing material degradation and preventing dust generation, industrial operations can achieve optimal performance and maintain a safe working environment. For businesses seeking reliable material handling solutions for manganese sulfate, Shandong HeadPowder Engineering Co., Ltd. offers expert guidance and customized systems that meet the highest standards of quality and efficiency.