With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industries involved in sorghum-based distillation processes, the efficient handling and transportation of distiller's residue—commonly known as sorghum distiller's residue—present critical operational challenges. This residue, a byproduct of alcohol production from sorghum, requires specialized equipment to manage its bulk, moisture content, and handling characteristics. The sorghum distiller's residue powder conveying system equipment addresses these challenges by providing a reliable, efficient solution for moving this material through various stages of processing and disposal.
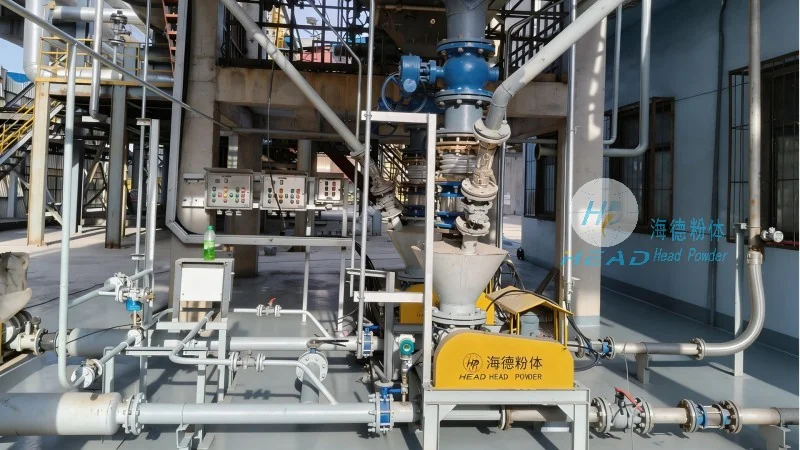
The sorghum distiller's residue powder conveying system is a specialized piece of industrial equipment designed to transport dry or semi-dry powders, such as sorghum distiller's residue, from one location to another within a facility. This system is essential for optimizing workflow in distilleries, as it reduces labor costs, minimizes material loss, and enhances overall operational safety. The equipment typically includes components like hoppers, conveyors (e.g., screw conveyors, pneumatic conveyors), and control systems to ensure smooth and continuous material movement.
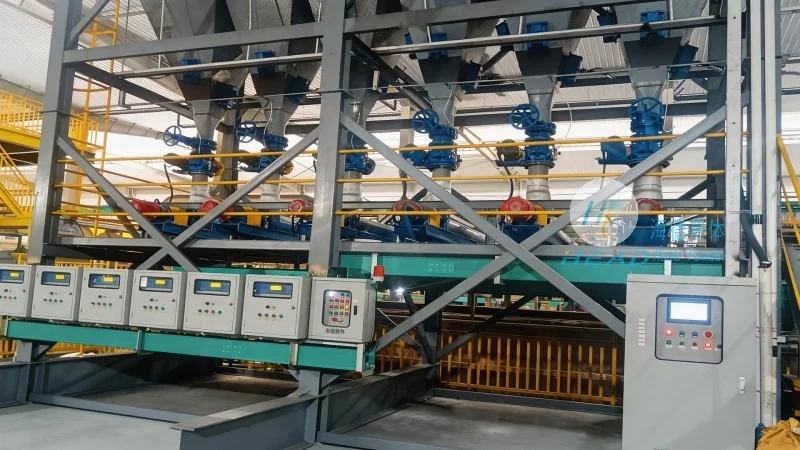
The effectiveness of the sorghum distiller's residue powder conveying system relies on several key components, each playing a vital role in the overall operation. First, the hopper serves as the storage and feeding unit, where the residue is collected and fed into the conveyor system. Hoppers are designed with appropriate dimensions and material (often stainless steel or corrosion-resistant alloys) to handle the abrasive nature of the residue and prevent clogging. Next, the conveyor is the core of the system, responsible for transporting the material. Common types include screw conveyors, which use a rotating screw to move material along a tube, and pneumatic conveyors, which utilize air pressure to propel the powder through a pipeline. The choice of conveyor type depends on factors such as the residue's moisture content, particle size, and the distance it needs to be transported. Additionally, control systems are integrated to regulate the flow rate, speed, and direction of the material, ensuring precise and safe operation. These systems may include sensors, valves, and programmable logic controllers (PLCs) to monitor and adjust the conveying process in real time.
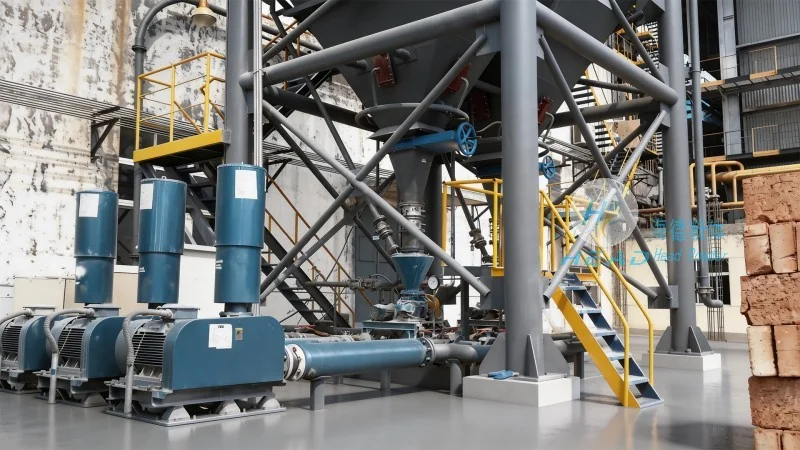
The design of the sorghum distiller's residue powder conveying system is guided by several fundamental principles aimed at maximizing efficiency, reliability, and safety. One key principle is material compatibility. Since sorghum distiller's residue can be abrasive and may contain moisture, the equipment must be constructed from materials that resist wear and corrosion. Stainless steel, high-chrome alloys, and food-grade plastics are commonly used for components that come into direct contact with the residue. Another critical principle is hygiene and sanitation. In food and beverage processing industries, where sorghum is used for alcohol production, maintaining a clean and sanitary environment is paramount. The conveying system is designed with smooth surfaces, minimal dead zones, and easy-to-clean components to prevent contamination and ensure compliance with regulatory standards. Furthermore, energy efficiency is a key consideration in modern design. The system is engineered to minimize energy consumption while maintaining high conveying rates. This is achieved through optimized conveyor speeds, efficient motor selection, and the use of variable frequency drives (VFDs) to adjust power usage based on the load. Finally, flexibility and adaptability are important design aspects. The system is often modular, allowing for easy expansion or modification to accommodate changes in production volume or residue characteristics. This flexibility ensures that the equipment can evolve with the needs of the distillery over time.
The implementation of a sorghum distiller's residue powder conveying system offers numerous benefits to distilleries. Firstly, it significantly improves operational efficiency by automating the material handling process. Manual handling of residue is labor-intensive and can lead to accidents or material loss. The automated system reduces the need for manual labor, lowers labor costs, and minimizes the risk of injury. Secondly, it enhances product quality by ensuring consistent and uniform material flow. This consistency is crucial for downstream processes, such as drying or composting, where the quality of the residue directly impacts the final product. Thirdly, the system improves safety by eliminating the need for workers to handle heavy or abrasive materials. By automating the conveying process, the risk of dust exposure, material spills, and mechanical injuries is reduced. Fourthly, it enhances environmental sustainability. The efficient handling of residue reduces the likelihood of spills or leaks, which can contaminate the environment. Additionally, the system may be integrated with waste management systems to facilitate the recycling or disposal of the residue in an environmentally responsible manner.
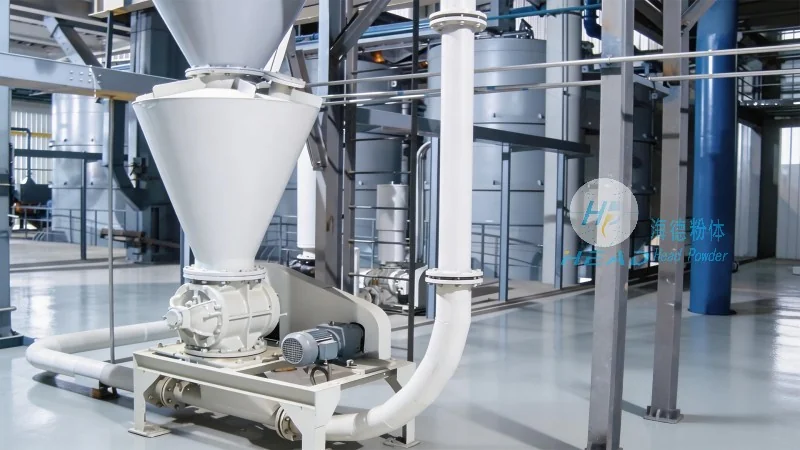
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of specialized powder handling equipment. With a focus on innovation and customer-centric solutions, HeadPowder has established itself as a trusted partner for industries requiring reliable and efficient material conveying systems. The company's expertise lies in designing and manufacturing equipment tailored to the unique needs of each client, ensuring that the final product meets the highest standards of performance, durability, and safety. HeadPowder's commitment to quality and customer satisfaction has earned it a reputation for excellence in the industry, making it a preferred choice for distilleries and other processing facilities seeking advanced powder handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top