With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
High-pressure bin pump systems represent a sophisticated solution for material handling and transportation in various industrial applications. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-efficiency pneumatic conveying equipment that meets the diverse needs of modern industries. This article delves into the working principle and key features of high-pressure bin pump material pneumatic conveying systems, offering insights into their operational efficiency and practical applications.
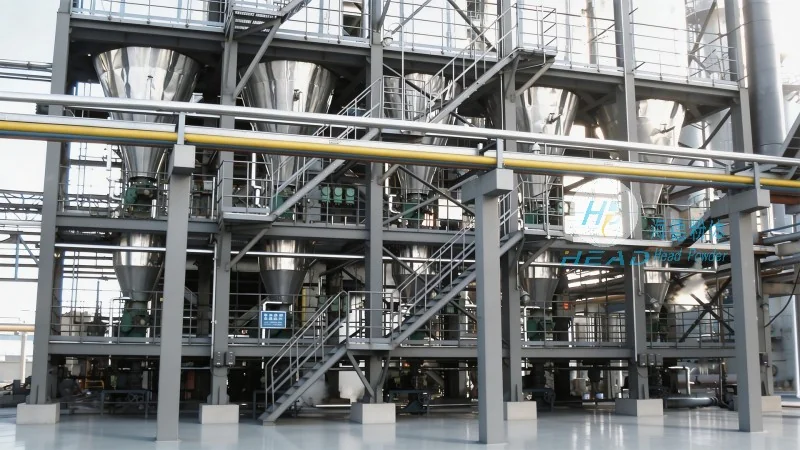
At the core of high-pressure bin pump systems is the bin pump, which operates by creating a high-pressure air flow to transport bulk materials from a storage bin to the discharge point. The process begins with the material being fed into the storage bin, where it accumulates until the system is activated. When the pump is started, compressed air is introduced into the bin, creating a pressure differential that forces the material to move through the conveying line. The high-pressure air acts as the driving force, carrying the material in a dense phase, which minimizes particle degradation and ensures a consistent flow rate. The system typically includes a hopper, a pump unit, and a discharge valve, all working in tandem to maintain optimal pressure and flow. The bin pump's ability to handle a wide range of materials, from powders to granules, makes it a versatile choice for industries such as chemical, food, and pharmaceutical processing.
High-pressure bin pump systems are distinguished by several key features that enhance their performance and reliability. Firstly, their ability to operate at high pressures (typically 5-10 bar) allows for long-distance and high-rise material transport without the need for intermediate boosters. This reduces installation complexity and maintenance costs. Secondly, the dense phase conveying mode ensures minimal particle segregation and attrition, preserving the quality of the material being transported. This is particularly important for sensitive materials like food or pharmaceuticals, where contamination or degradation could impact product quality. Thirdly, the system's compact design and modular components enable easy integration into existing production lines, making it suitable for both new and retrofit applications. Additionally, the high-pressure bin pump offers excellent control over flow rates, allowing operators to adjust the conveying speed according to production requirements. The system also features advanced safety mechanisms, such as pressure relief valves and overload protection, to prevent accidents and ensure safe operation.
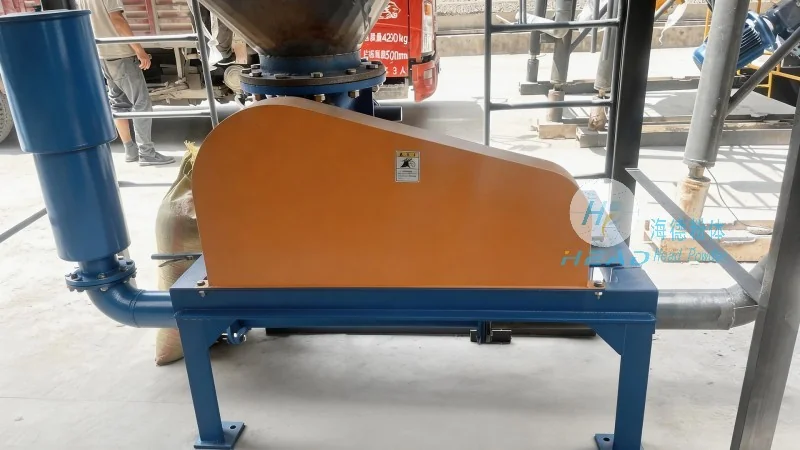
High-pressure bin pump systems find extensive applications in various industrial sectors, including chemical manufacturing, food processing, pharmaceutical production, and mining. In chemical plants, they are used to transport powders like cement, limestone, and plastic resins, ensuring efficient material movement between reactors and storage tanks. In food processing facilities, the system's ability to handle hygienic materials without contamination makes it ideal for conveying flour, sugar, and other food products. Pharmaceutical manufacturers benefit from the system's precision and cleanliness, as it can transport active pharmaceutical ingredients (APIs) and other sensitive materials without compromising purity. The mining industry also utilizes high-pressure bin pumps to transport bulk materials like coal, ore, and sand from mines to processing plants. The primary advantages of these systems in industrial settings include increased productivity, reduced labor costs, and improved material quality. By eliminating the need for manual handling and traditional conveyor belts, the high-pressure bin pump streamlines operations and enhances overall efficiency.
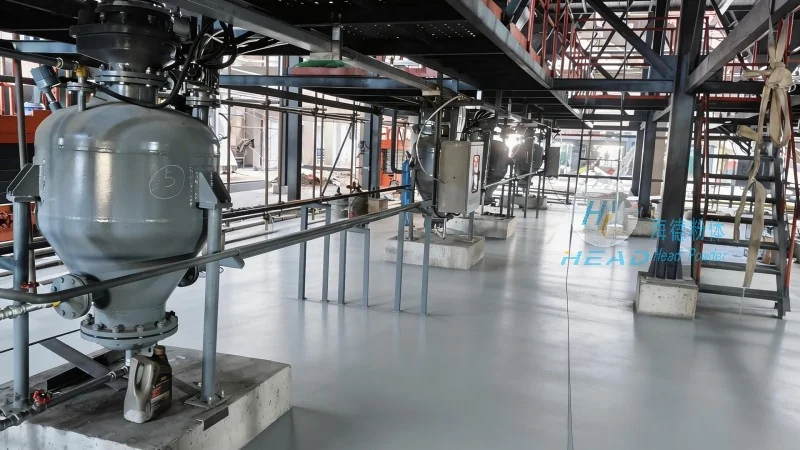
Shandong HeadPowder Engineering Co., Ltd. offers a range of high-pressure bin pump systems with customizable specifications to meet specific industrial requirements. The company's products are designed to handle materials with varying particle sizes, densities, and flow characteristics. Technical specifications typically include conveying distances of up to 200 meters, vertical lifts of 50 meters or more, and flow rates ranging from 0.5 to 10 cubic meters per hour. The bin pump units are constructed from high-quality materials, such as stainless steel or carbon steel, depending on the material being conveyed and the operating environment. The system's control panel allows for easy monitoring and adjustment of pressure, flow, and other parameters, ensuring optimal performance. Customization options include different hopper sizes, conveying line diameters, and discharge configurations to fit specific plant layouts. The company also provides comprehensive technical support and after-sales services, including installation, maintenance, and troubleshooting, to ensure long-term system reliability.
As a reputable manufacturer in the material handling industry, Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted partner for businesses seeking reliable and efficient pneumatic conveying solutions. The company is committed to delivering high-quality products that meet international standards and customer expectations. With a team of experienced engineers and technicians, HeadPowder provides tailored solutions that address the unique challenges of each client's operation. The company's focus on innovation and customer satisfaction has earned it a strong reputation in the market. HeadPowder's service commitment includes providing detailed technical documentation, on-site training for operators, and prompt technical support to resolve any issues that may arise. By partnering with HeadPowder, industries can enhance their operational efficiency, reduce costs, and improve product quality, ensuring long-term success in their respective markets.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top