With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Efficient and reliable dust collector ash material conveying lines are crucial components in industrial settings where dust and particulate matter are managed. These systems are designed to transport collected ash or other fine materials from dust collection equipment to storage or processing facilities, ensuring a smooth and controlled operation. The performance of such lines directly impacts the overall efficiency and environmental compliance of industrial processes.
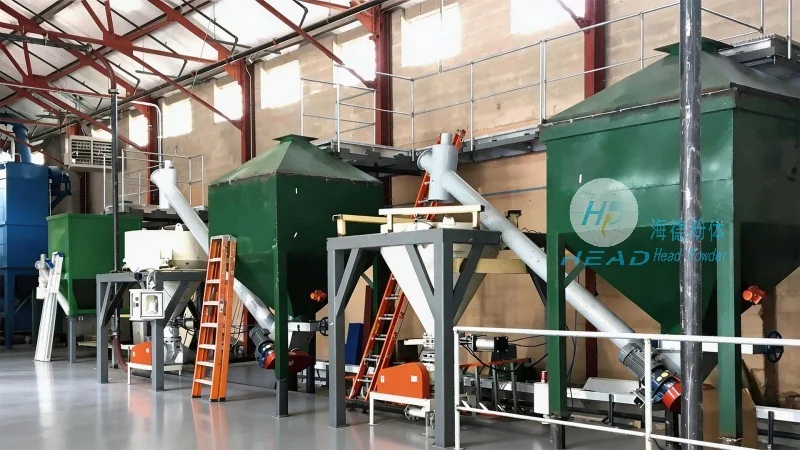
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced dust collector ash material conveying systems. With a strong commitment to quality and innovation, HeadPowder has established itself as a trusted partner for industries requiring robust and efficient material handling solutions. The company's facilities and expertise are centered in Shandong, providing a solid foundation for delivering high-performance conveying lines tailored to specific industrial needs.
The dust collector ash material conveying line typically consists of several key components that work in tandem to ensure the effective transport of ash from the dust collection system. These components include ash hoppers, discharge devices, conveying pipelines, air movers (such as fans or blowers), and collection or discharge units. Each component plays a vital role in the overall operation, contributing to the system's efficiency and reliability.
The operation of a dust collector ash material conveying line begins with the accumulation of ash in the dust collector's hopper. As the ash level rises, the discharge device (often a rotary valve or a star feeder) starts to release the material into the conveying pipeline. Simultaneously, the air mover (usually a centrifugal fan or a positive displacement blower) generates the necessary airflow to create a vacuum or pressure within the system. This airflow pulls the ash particles from the hopper and transports them through the pipeline to the designated destination.
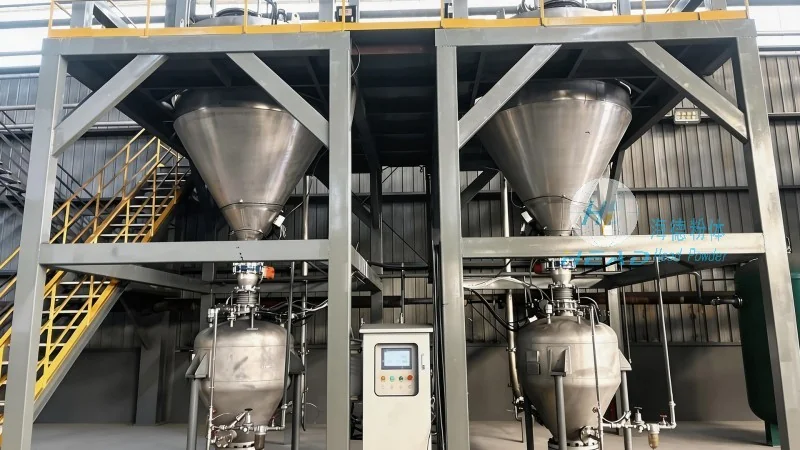
During the conveying process, the ash travels through the pipeline at a controlled velocity, which is optimized to prevent particle segregation or blockages. The system may include features such as cyclone separators or filters to ensure that the ash is delivered to the target location without loss or contamination. The entire process is automated and monitored to maintain consistent performance and minimize downtime.
The working principle of a dust collector ash material conveying line is based on the principles of fluid dynamics and mechanical transport. The system utilizes either a negative pressure (suction) or positive pressure (blowing) method to move the ash particles. In the negative pressure system, the fan creates a vacuum that draws the ash from the hopper into the pipeline. The ash is then carried by the air stream to the discharge point. In the positive pressure system, the fan pushes air through the pipeline, carrying the ash particles along with it.
Key components such as the ash hopper, discharge valve, and air mover are designed to work together seamlessly. The hopper provides a storage area for the collected ash, while the discharge device controls the flow rate of the material into the pipeline. The air mover provides the necessary force to move the ash through the system, and the pipeline ensures the material is transported to the desired location. The system may also include additional components like silencers to reduce noise and separators to remove any remaining air or fine particles from the ash.
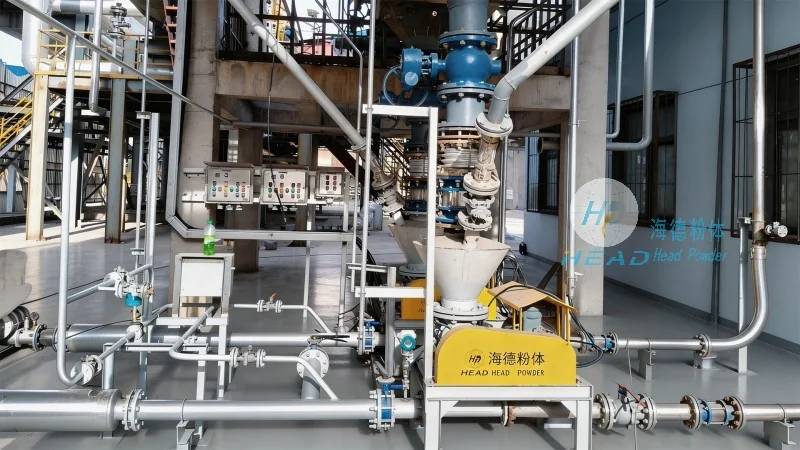
Modern dust collector ash material conveying lines from HeadPowder are equipped with several technical features that enhance their performance and reliability. These features include high-efficiency fans that minimize energy consumption, durable materials for the pipeline and components to withstand abrasive ash particles, and automated control systems that ensure consistent operation. The systems are designed to handle a wide range of ash types and particle sizes, making them versatile for various industrial applications.
One of the significant advantages of these conveying lines is their ability to operate with minimal maintenance. The use of robust materials and reliable components reduces the need for frequent repairs, leading to lower operational costs and increased uptime. Additionally, the systems are designed to be environmentally friendly, with features that minimize dust emissions and noise pollution, ensuring compliance with environmental regulations.
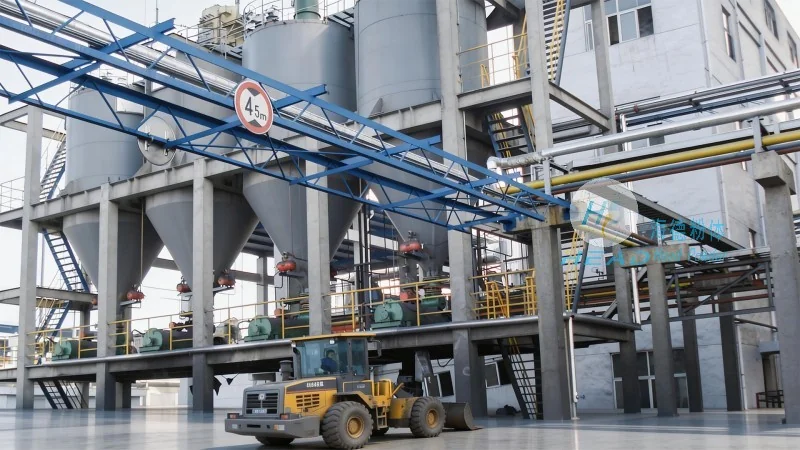
Dust collector ash material conveying lines are widely used in various industries where dust and ash are generated as byproducts. These include cement manufacturing, steel production, power generation (especially coal-fired plants), and other industrial processes that involve the handling of fine particulate materials. The systems are essential for maintaining a clean and safe working environment by efficiently removing ash from dust collectors and transporting it to appropriate storage or disposal facilities.
In cement plants, for example, the conveying line is used to transport ash from the dust collectors to the cement silos or other processing units. In steel mills, the system helps in managing the ash generated during the steelmaking process, ensuring that it is handled safely and efficiently. The versatility of these conveying lines makes them suitable for a wide range of industrial applications, providing a reliable solution for material transport in dust management systems.
The operation process and working principle of dust collector ash material conveying lines are critical to the efficient management of ash and dust in industrial settings. With advanced technology and robust design, systems from HeadPowder offer reliable and efficient solutions for transporting ash from dust collectors to storage or processing facilities. By understanding the operation and principles of these systems, industries can ensure optimal performance, reduced maintenance costs, and compliance with environmental standards. The expertise and commitment of HeadPowder in this field make them a leading provider of dust collector ash material conveying lines, catering to the diverse needs of modern industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top