With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder Engineering Co., Ltd., a professional manufacturer based in Shandong, China, specializes in the design, development, and supply of advanced powder gas-solid transport systems, particularly for ash silos. This article delves into the fundamental principles of such systems and highlights the key working scene characteristics that define their application in industrial settings.
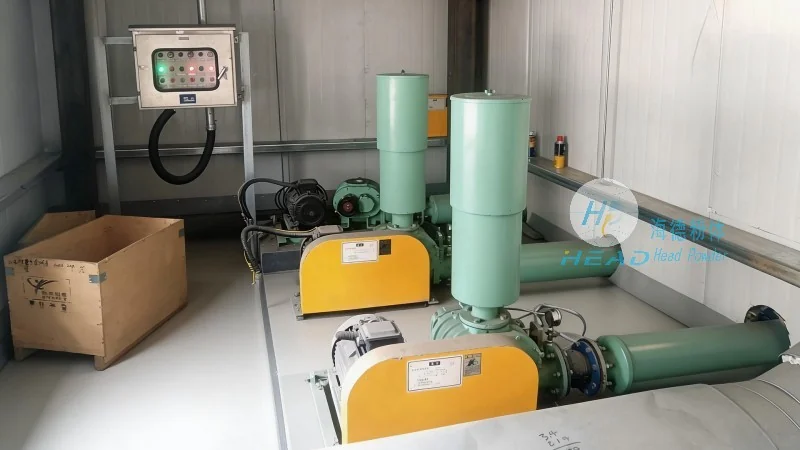
The powder gas-solid transport system for ash silos operates on the principle of transporting bulk powders, such as fly ash or other fine particulate materials, through a pipeline using a carrier gas. This method, commonly known as pneumatic conveying, leverages the kinetic energy of the gas to move the solid particles. The system typically consists of several key components, including a silo for material storage, a feeder to control the flow of powder, a conveying pipeline, and a receiver to collect the material at the destination. The carrier gas, often air or a mixture of air and other gases, is introduced into the system under controlled pressure, creating a flow that propels the powder particles through the pipeline. This approach offers significant advantages over traditional mechanical conveying methods, such as reduced equipment wear, lower maintenance requirements, and the ability to transport materials over long distances without the need for intermediate storage or handling.
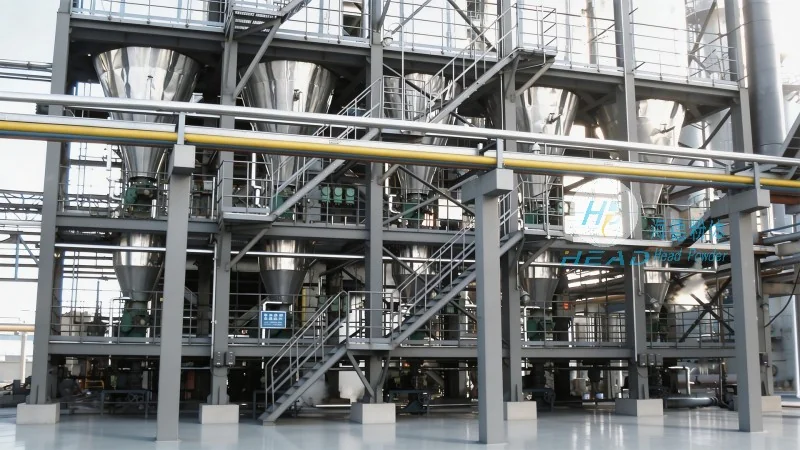
The working scene characteristics of ash silo powder transport systems are tailored to meet the specific demands of industrial applications, particularly in power plants and other facilities that generate large volumes of fly ash. These systems are designed to handle high throughput rates, ensuring efficient material transfer from the ash silo to processing or disposal locations. The characteristics include: (1) High Efficiency in Material Handling: The systems are engineered to maintain consistent flow rates, minimizing downtime and maximizing operational productivity. (2) Adaptability to Varying Particle Sizes and Densities: Modern designs incorporate adjustable parameters, such as air pressure and flow rates, to accommodate different types of ash materials, from fine to coarse particles. (3) Minimal Environmental Impact: By utilizing enclosed pipelines and controlled gas flow, the systems reduce dust emissions and ensure compliance with environmental regulations. (4) Compact and Space-Efficient Design: The components are often arranged to fit within limited plant spaces, making them suitable for retrofitting into existing facilities. (5) Reliable and Low-Maintenance Operation: Advanced materials and robust construction reduce the risk of system failures and simplify routine maintenance, contributing to long-term operational reliability.
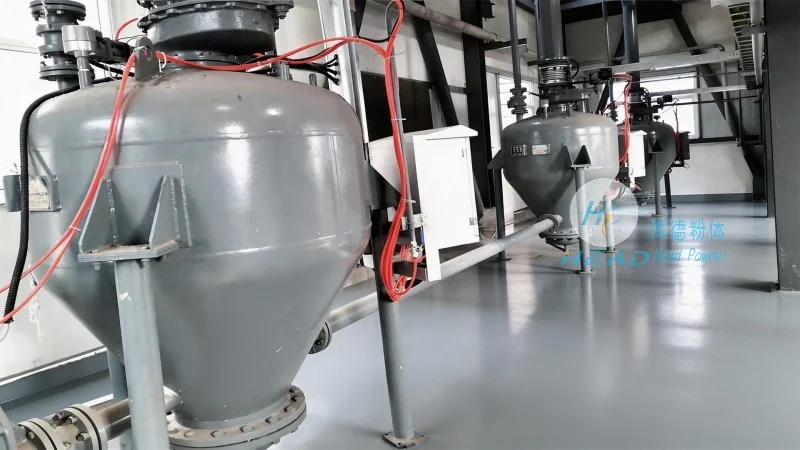
The application scenarios for ash silo powder transport systems are diverse and critical to the efficient operation of industrial plants. These systems are commonly used in: (1) Power Generation Plants: To transport fly ash from the ash silo to storage or disposal sites, ensuring smooth operation of the plant's waste management processes. (2) Industrial Processing Facilities: For conveying fine powders from silos to processing units, such as grinding or mixing equipment, where consistent material flow is essential for product quality. (3) Construction and Infrastructure Projects: In some cases, the systems may be used to transport bulk materials for construction purposes, leveraging the efficient transport capabilities of pneumatic conveying. The operational benefits of these systems include improved safety by reducing manual handling of powders, enhanced process control through precise flow regulation, and cost savings from reduced labor and equipment wear. Additionally, the systems contribute to overall plant efficiency by minimizing material loss and optimizing the use of available space.
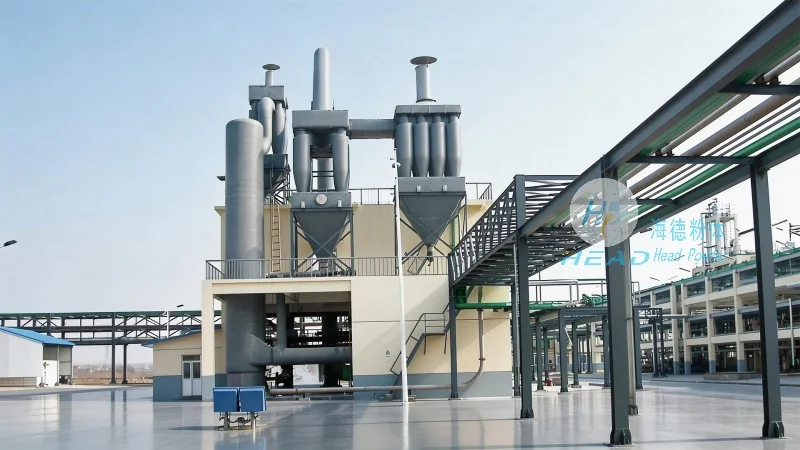
HeadPowder Engineering Co., Ltd. provides comprehensive solutions for ash silo powder gas-solid transport systems, combining advanced engineering with practical application expertise. By understanding the core principles and working scene characteristics, industrial facilities can select and implement the most suitable system to meet their specific operational needs. The company's commitment to quality, efficiency, and reliability ensures that its systems deliver long-term value and support the sustainable operation of industrial processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top