With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding the principles and operational characteristics of floor-level material handling systems is crucial for optimizing material flow in various industrial and logistics environments. These systems are designed to facilitate the efficient movement of goods from storage to processing or shipping areas, often operating beneath the floor surface to minimize space usage and maintain a clean, unobstructed workspace above.
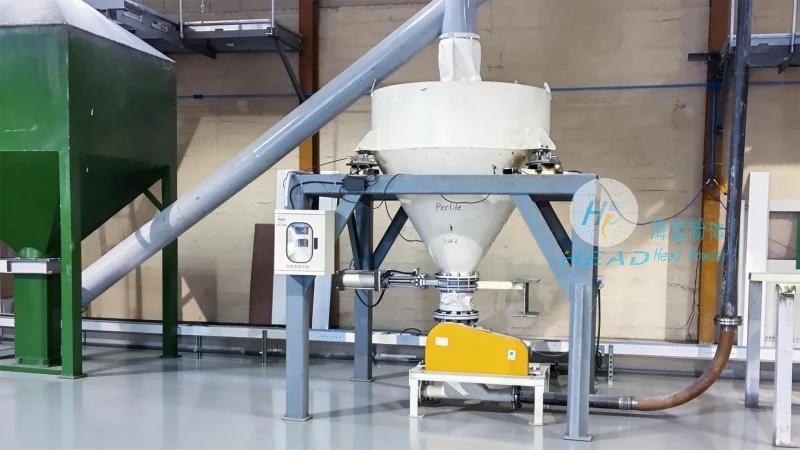
Floor-level material handling systems typically rely on a combination of mechanical components and control technologies to achieve seamless material transfer. The fundamental principle involves the use of conveyor belts, rollers, or chain-driven mechanisms that are integrated into the floor structure. A key component is the drive system, which can be electric, hydraulic, or motorized, providing the necessary force to move materials along the designated path. Control modules, often equipped with sensors and programmable logic controllers (PLCs), regulate the speed, direction, and timing of material movement, ensuring precision and safety. Additionally, these systems may incorporate load-bearing structures that are engineered to support the weight of materials and equipment, while maintaining structural integrity and stability.
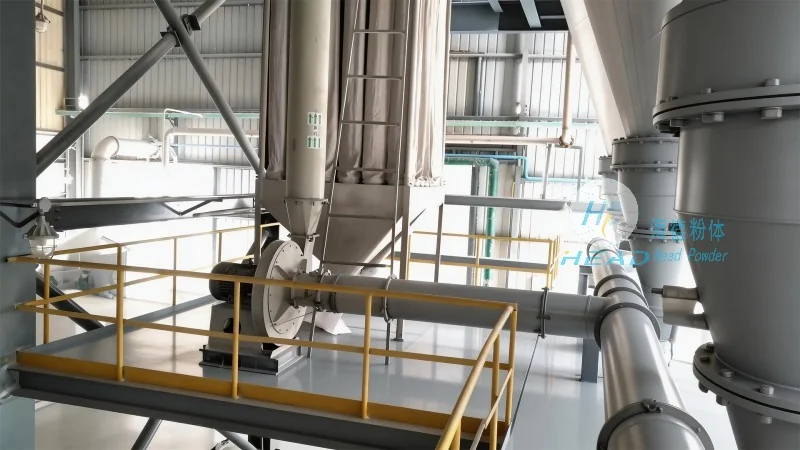
These systems are widely applied in diverse working scenarios, each tailored to specific operational needs. In warehouse environments, floor-level conveyors are commonly used for inbound and outbound material handling, such as transporting pallets or containers from storage racks to loading docks or sorting stations. The ability to operate beneath the floor allows for the creation of a clear, open workspace above, which is essential for forklift operations and manual handling tasks. In manufacturing facilities, these systems are integrated into production lines to move raw materials to workstations, transfer finished products to packaging areas, or transport waste materials to disposal points. The flexibility of floor-level systems enables them to adapt to different production layouts, accommodating changes in workflow and production volume. Additionally, in logistics and distribution centers, floor-level conveyors are used for sorting and routing packages based on destination, improving order fulfillment efficiency and reducing handling time. The systems can also be customized for specialized applications, such as in the food processing industry, where hygiene and sanitation requirements are critical, or in the pharmaceutical sector, where precise material handling is essential for maintaining product integrity.
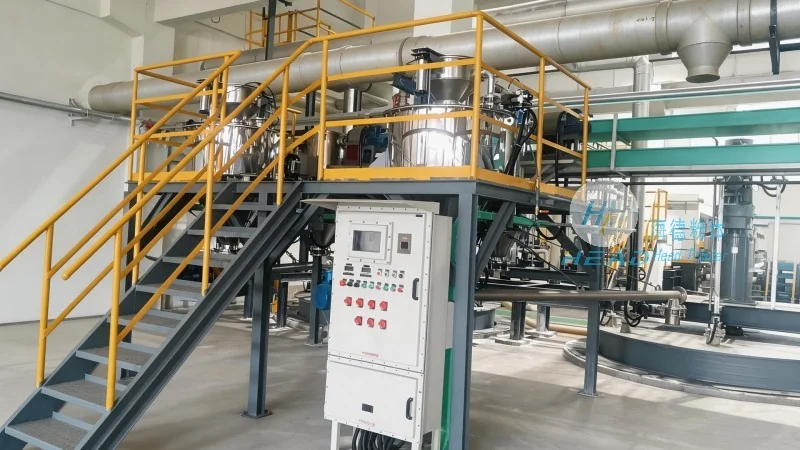
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing floor-level material conveying systems tailored to the unique needs of various industries. With headquarters in Shandong, China, the company leverages advanced engineering and manufacturing capabilities to deliver high-quality, reliable systems that enhance operational efficiency and productivity. The company's expertise lies in understanding the diverse operational requirements of clients, from small-scale businesses to large-scale industrial operations, and providing customized solutions that address specific challenges in material flow management. By combining innovative technology with practical application, Shandong HeadPowder Engineering Co., Ltd. helps clients optimize their material handling processes, reduce costs, and improve overall operational performance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top