With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Multi-functional pneumatic conveying systems represent a sophisticated technology in material handling, designed to transport bulk materials efficiently through the use of air or gas as the conveying medium. These systems are integral to modern industrial processes, offering versatility and adaptability across various applications. The core principle involves creating a pressure differential that propels particles through a pipeline, enabling seamless movement from source to destination. This method is particularly advantageous for handling fine powders, granules, and other dry bulk materials, where traditional mechanical conveyors may face challenges such as material degradation or blockages. Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field, specializes in developing advanced pneumatic conveying solutions that meet the diverse needs of industries worldwide.
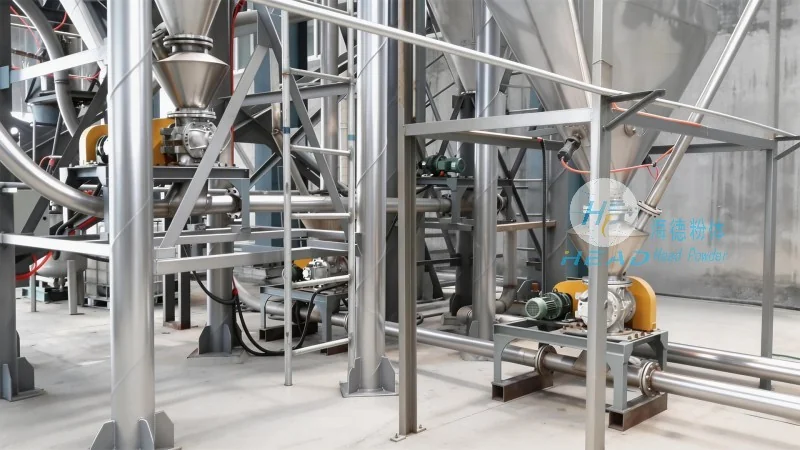
The fundamental principle of pneumatic conveying is based on the interaction between the conveying medium (air or gas) and the material being transported. There are two primary modes: pressure and vacuum. In pressure systems, compressed air is used to push material through the pipeline, while vacuum systems draw material from the source using a negative pressure. The selection of mode depends on factors like material properties, distance, and system layout. Additionally, the design of the system—including the type of airlocks, cyclones, and ductwork—plays a critical role in ensuring efficient and reliable operation. For instance, the use of rotary airlocks prevents material from backflowing into the system, maintaining a consistent flow rate. Cyclones, on the other hand, separate conveyed material from the air stream, allowing for material recovery and air filtration.
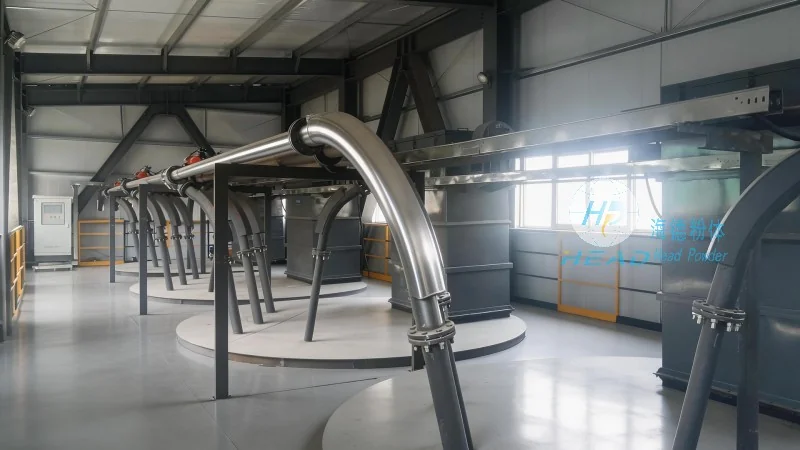
Multi-functional pneumatic conveying systems are widely employed in diverse industrial sectors, each presenting unique requirements that the technology addresses effectively. In the pharmaceutical industry, for example, these systems are used to transport sensitive powders, ensuring minimal contamination and maintaining product integrity. The ability to operate in a sterile environment is crucial, and pneumatic conveying systems can be designed with sealed components to meet these standards. Similarly, in the food processing sector, systems are adapted to handle food-grade materials, with features like stainless steel construction and hygienic design to prevent cross-contamination. The versatility of these systems also extends to the chemical industry, where they are used to transport powders that may be hazardous or reactive, requiring careful control of pressure and temperature.
One of the key advantages of multi-functional pneumatic conveying is its ability to handle a wide range of materials with minimal maintenance. Unlike mechanical conveyors, which may require regular cleaning and lubrication, pneumatic systems can often operate continuously without interruption. This leads to increased productivity and reduced downtime. Furthermore, the system's adaptability allows for easy integration into existing production lines, making it a cost-effective solution for many industries. The energy efficiency of pneumatic conveying is also noteworthy, as it can reduce energy consumption compared to other methods, especially over long distances. By optimizing the air velocity and pipeline design, operators can achieve optimal performance while minimizing operational costs.
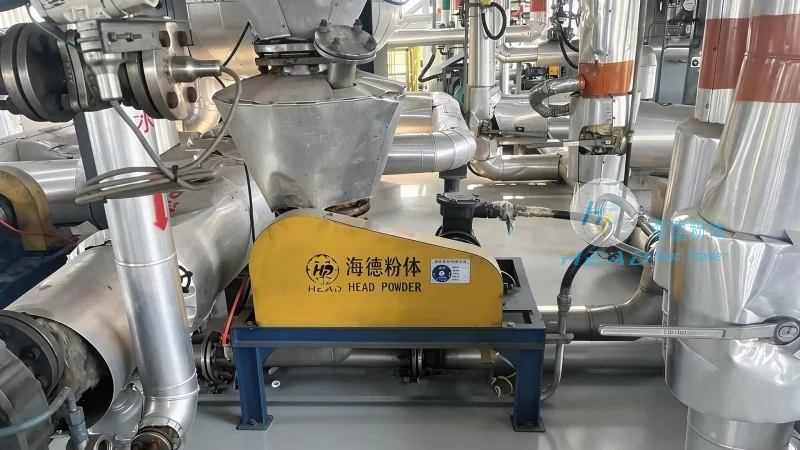
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying systems tailored to specific customer needs. The company's expertise lies in understanding the unique challenges of each application and providing solutions that enhance operational efficiency. With a focus on quality and innovation, HeadPowder offers a range of products, from basic pressure conveying systems to advanced vacuum and combined systems. The company's team of engineers works closely with clients to assess their requirements, conduct feasibility studies, and develop tailored solutions. This approach ensures that the final system meets all performance criteria while adhering to industry standards and regulations. The scalability of these systems is another significant advantage, as they can be expanded or modified to accommodate changing production demands without significant disruption.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top