Working Principle and Features of Polyvinyl Alcohol Butyral Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems, including Polyvinyl Alcohol Butyral (PVB) pneumatic conveyors. These systems are engineered to efficiently transport bulk materials, offering reliable performance and versatility in various industrial applications.
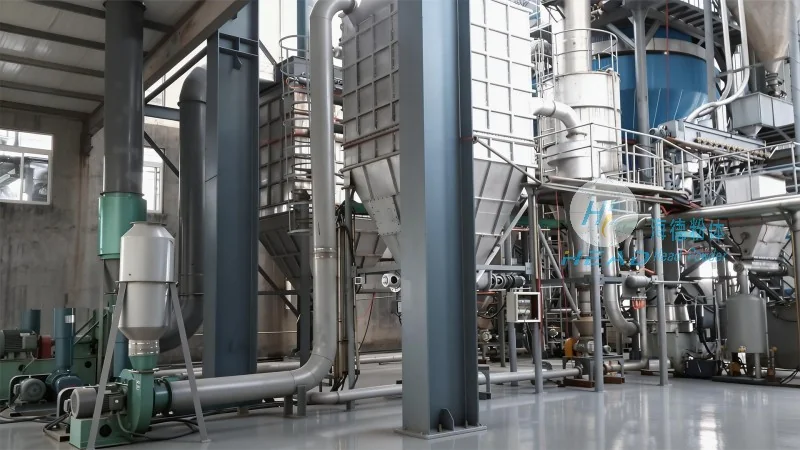
Working Principle of Polyvinyl Alcohol Butyral Pneumatic Conveying Equipment
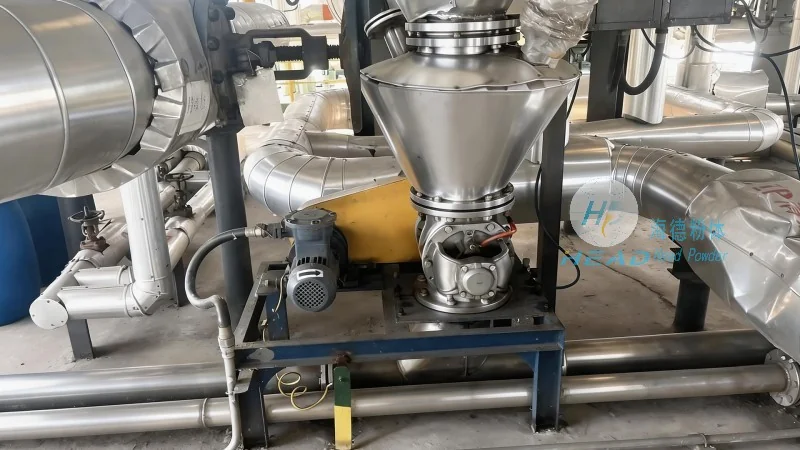
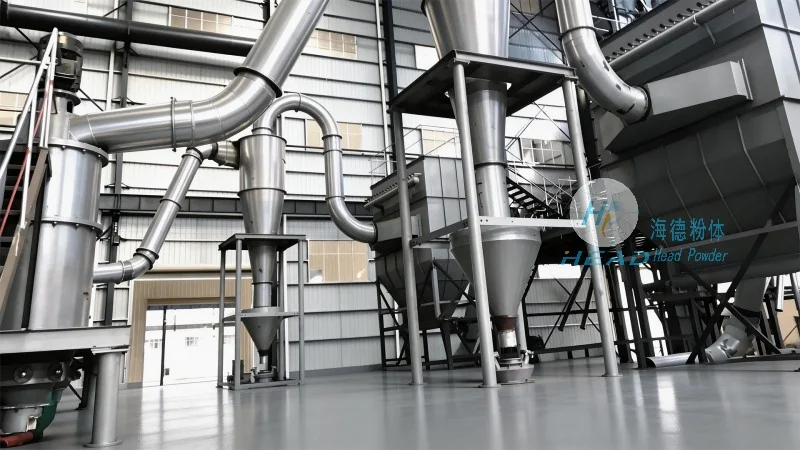
The operation of a Polyvinyl Alcohol Butyral pneumatic conveying system relies on the principle of air flow to move materials. The system typically consists of a hopper, a rotary valve, a conveying pipe, and a receiver. When the material is fed into the hopper, it is discharged through the rotary valve into the conveying pipe. Simultaneously, a fan or blower generates a high-velocity airflow within the pipe, which entrains the material particles and transports them to the receiver. The air and material mixture then passes through a separator, where the air is discharged and the material is collected. This process ensures efficient and continuous material transfer without the need for mechanical components like belts or buckets.
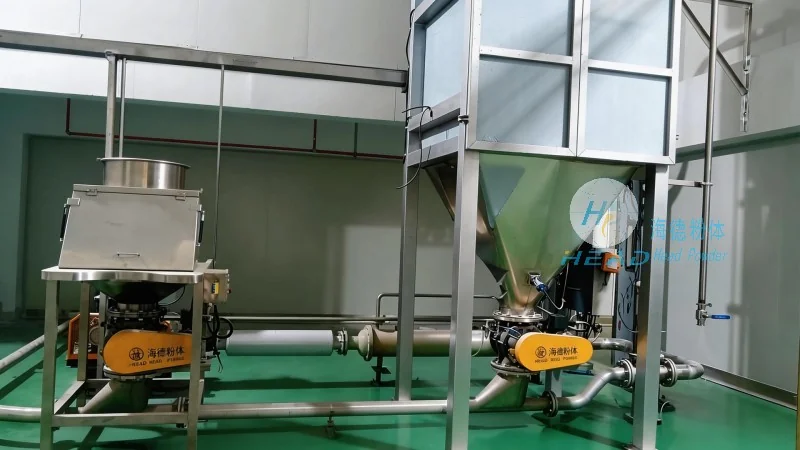
Key Features of Polyvinyl Alcohol Butyral Pneumatic Conveying Equipment
HeadPowder's PVB pneumatic conveying equipment is characterized by several notable features that enhance its performance and suitability for diverse industrial needs. Firstly, the system offers excellent material handling capabilities, capable of transporting a wide range of bulk materials, including powders, granules, and fine particles. The use of PVB as a material ensures resistance to corrosion and wear, extending the equipment's service life. Secondly, the pneumatic conveying method provides a dust-free and hygienic transfer process, which is particularly important in industries such as food, pharmaceuticals, and chemicals where contamination control is critical. Thirdly, the system is designed for low maintenance requirements, with minimal moving parts that reduce operational downtime and maintenance costs. Additionally, the flexibility of the conveying system allows for easy integration into existing production lines, adapting to various layout configurations and material flow requirements.
Applications and Benefits in Industrial Settings
Polyvinyl Alcohol Butyral pneumatic conveying equipment from HeadPowder is widely used in various industrial sectors, including chemical processing, food processing, pharmaceutical manufacturing, and mining. The equipment's ability to handle different material types and its hygienic design make it ideal for applications where material purity and safety are paramount. The benefits of using this technology include increased production efficiency, reduced labor costs, and improved workplace safety by eliminating the need for manual handling of bulk materials. Furthermore, the system's compact design and low energy consumption contribute to cost savings and environmental sustainability in industrial operations.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., located in Shandong, China, is committed to providing high-quality PVB pneumatic conveying equipment that meets the evolving needs of modern industries. With a focus on innovation, reliability, and customer satisfaction, the company ensures that its products are engineered to deliver optimal performance and durability. The working principle and features of the Polyvinyl Alcohol Butyral pneumatic conveying equipment highlight the advanced technology and expertise behind HeadPowder's solutions, making them a trusted choice for businesses seeking efficient and reliable material handling solutions.