

Working Principle and Features of Multi-functional Pneumatic Conveying System Equipment
Efficient material handling is a critical component in modern industrial operations, and the multi-functional pneumatic conveying system has emerged as a versatile solution for transporting bulk materials. This article delves into the working principle and key features of such systems, highlighting how they enhance operational efficiency and reliability in various industries. The discussion is centered around the advanced solutions offered by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, known by its common abbreviation as HeadPowder.
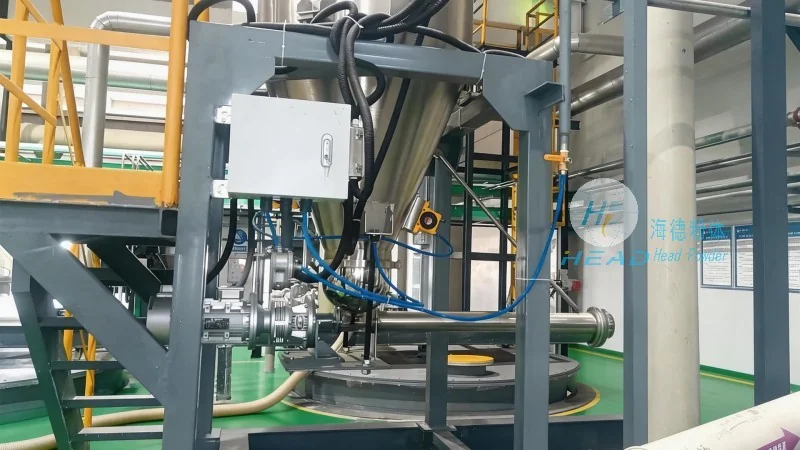
Understanding the Working Principle of Multi-functional Pneumatic Conveying Systems
The core of a pneumatic conveying system lies in its ability to transport materials through a pressurized or vacuum environment using air or other gases. In a typical setup, the system operates by creating a pressure differential that propels the material along a pipeline. For HeadPowder's multi-functional systems, the design incorporates both positive and negative pressure modes, allowing for flexibility in handling different types of materials and distances. The system typically consists of a feeding hopper, a conveying line, a control unit, and a discharge outlet. When the material is introduced into the hopper, it is drawn or pushed by the air flow through the pipeline to the destination. The control unit regulates the air pressure and flow rate, ensuring optimal performance and preventing material blockages or system damage. This dual-mode capability (positive and negative pressure) makes the system suitable for a wide range of applications, from short-distance transport to long-distance and even vertical lifting, adapting to diverse operational needs.
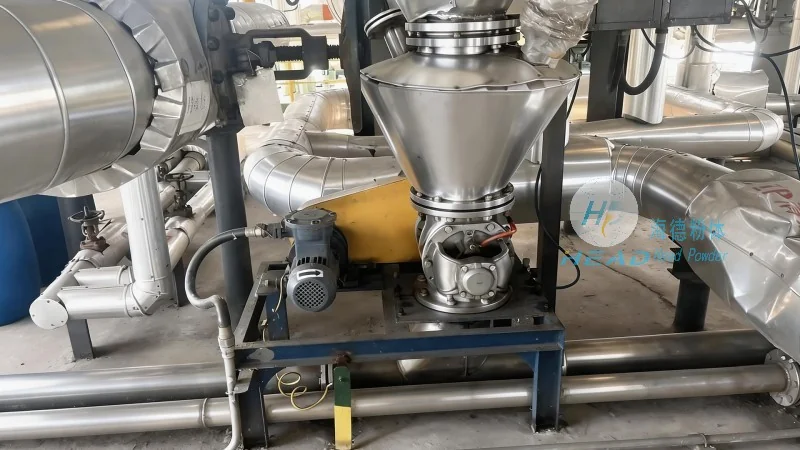
Key Features of the Multi-functional Pneumatic Conveying System
HeadPowder's multi-functional pneumatic conveying systems are distinguished by several key features that set them apart in the industry. Firstly, the system's adaptability is a standout characteristic. It can handle various materials, including powders, granules, and even bulk solids, with minimal modifications to the equipment. This versatility reduces the need for multiple handling systems, streamlining operations and lowering costs. Secondly, the system is designed for high efficiency and energy savings. Advanced control algorithms optimize air usage, minimizing energy consumption while maintaining consistent material flow rates. This not only reduces operational expenses but also aligns with sustainability goals in industrial processes. Thirdly, the system boasts exceptional reliability and durability. Constructed with high-quality materials and robust components, it can withstand harsh operating conditions, such as high temperatures or corrosive environments, ensuring long-term performance without frequent maintenance or replacements. Additionally, the system incorporates safety features, such as pressure relief valves and automatic shut-off mechanisms, to prevent accidents and protect personnel and equipment. The user-friendly interface of the control unit allows for easy monitoring and adjustment, enhancing operational convenience and reducing downtime.
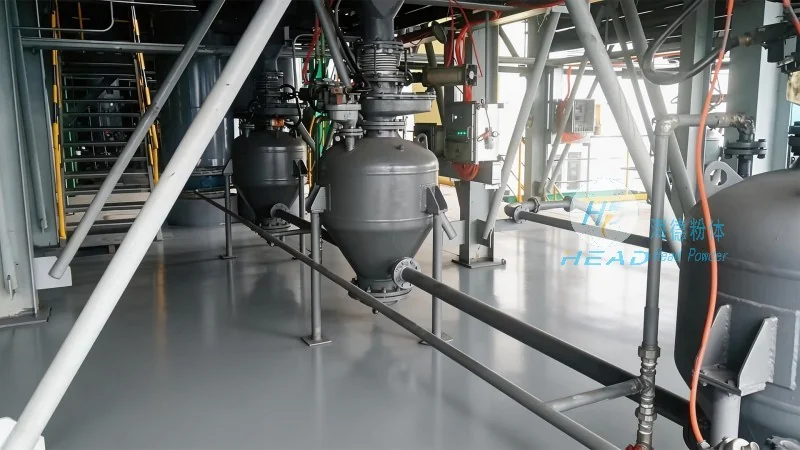
Application and Operational Benefits
The multi-functional pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. is widely used in industries such as pharmaceuticals, food processing, chemicals, and mining. In pharmaceutical manufacturing, for instance, the system ensures hygienic and dust-free material transport, meeting stringent regulatory requirements. In food processing, it maintains product quality by preventing contamination and preserving flavor and texture. The system's ability to handle fine powders without clogging is particularly beneficial in these sectors. In the chemical industry, it facilitates the safe transport of hazardous materials, reducing the risk of spills or leaks. The operational benefits extend beyond material handling efficiency. The system's compact design allows for easy integration into existing facilities, minimizing space requirements and installation time. This makes it an ideal solution for both new and retrofit projects. Furthermore, the system's low maintenance requirements contribute to overall cost savings, as fewer service interruptions are needed. The reliability of the system also enhances production continuity, as it reduces the likelihood of downtime due to equipment failures.

Conclusion and Company Overview
In conclusion, the multi-functional pneumatic conveying system by Shandong HeadPowder Engineering Co., Ltd. represents a significant advancement in material handling technology. By combining advanced working principles with a range of key features, the system offers unparalleled efficiency, versatility, and reliability for various industrial applications. The company, based in Shandong, China, has established itself as a trusted provider of innovative solutions, leveraging years of experience and expertise to meet the evolving needs of the industry. With a commitment to quality and customer satisfaction, HeadPowder continues to develop and refine its products to deliver superior performance and value to its clients. The system's adaptability, energy efficiency, and durability make it a preferred choice for businesses seeking to optimize their material handling processes and enhance overall operational productivity.