With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial applications requiring efficient material handling and dust control, the pulse dust collector material pneumatic conveying line represents a sophisticated solution. This system integrates advanced pneumatic conveying technology with pulse dust collection mechanisms to ensure optimal performance in various production environments. The following content will detail the operational process and working principles of this equipment, highlighting its key components and functional aspects.
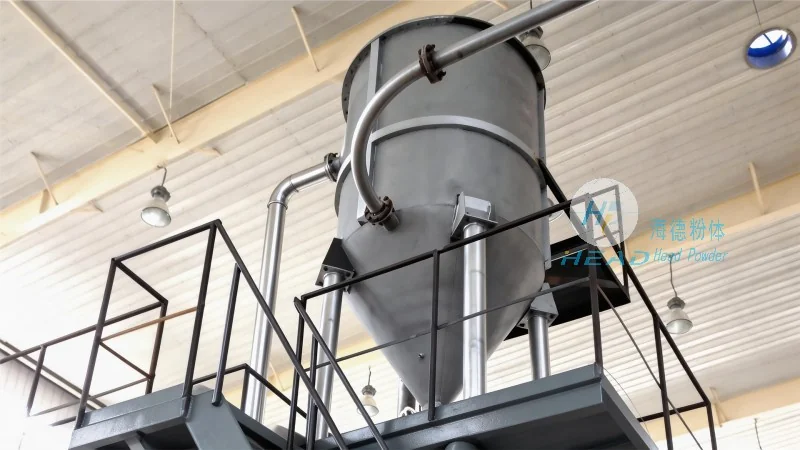
The pulse dust collector material pneumatic conveying line is a specialized system designed to transport bulk materials from one location to another while simultaneously capturing and filtering dust particles. It is widely used in industries such as pharmaceuticals, food processing, and chemical manufacturing, where maintaining air quality and material integrity is critical. The system combines the benefits of pneumatic conveying—like flexibility in layout and ability to handle fine powders—with the dust control capabilities of pulse dust collectors, making it a versatile choice for modern industrial operations.
The pulse dust collector material pneumatic conveying line consists of several core components that work in concert to achieve its objectives. These include the material hopper, which stores the bulk material; the air compressor or blower, which generates the air pressure needed for conveying; the pulse dust collector, which captures and filters dust; the conveying pipeline, which transports the material; and the control system, which regulates the operation of the entire process. Each component plays a vital role in ensuring the system operates efficiently and safely.
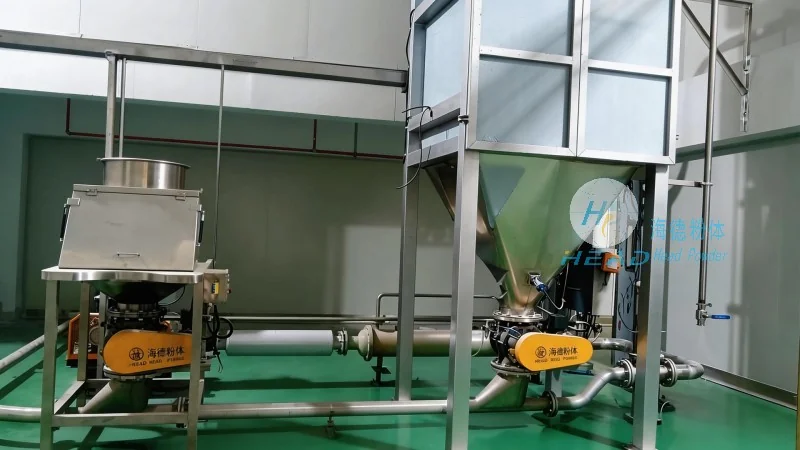
The operation of the pulse dust collector material pneumatic conveying line begins with the material being fed into the hopper. The control system then activates the air compressor, which generates a flow of air through the conveying pipeline. As the air moves through the pipeline, it picks up material from the hopper and transports it to the destination point. Simultaneously, the pulse dust collector continuously filters the air, capturing any dust particles and returning clean air to the system. This process ensures that the material is conveyed efficiently while maintaining air quality standards.
The pulse dust collector is a critical component of the system, responsible for capturing and filtering dust particles from the air stream. It operates on the principle of reverse pulse cleaning, where compressed air is periodically injected into the filter bags to dislodge accumulated dust. This mechanism prevents the filter bags from clogging and maintains the efficiency of the dust collection process. The collected dust is then discharged into a collection bin, while the cleaned air is returned to the conveying system or released into the environment after further treatment if required.
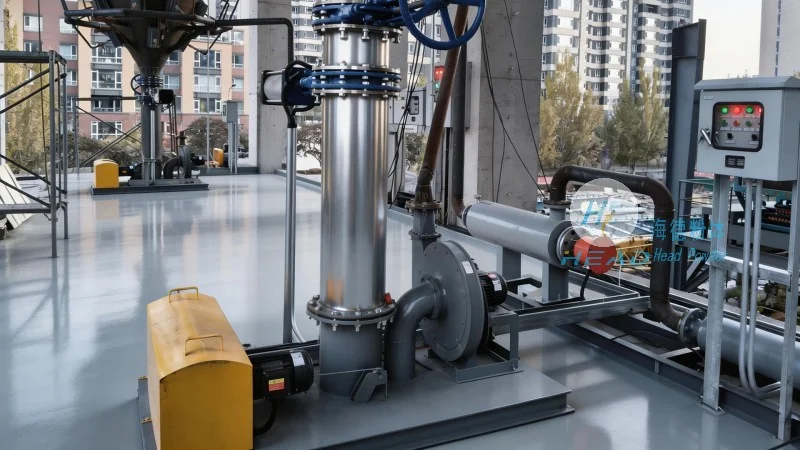
The pulse dust collector material pneumatic conveying line offers several advantages over traditional material handling methods. These include reduced labor costs due to automated operation, improved safety by minimizing manual handling of powders, and enhanced air quality by effectively controlling dust emissions. Additionally, the system is highly flexible, allowing for easy integration into existing production lines and adaptation to changing material handling requirements. Its compact design and low maintenance requirements also contribute to its overall efficiency and cost-effectiveness.
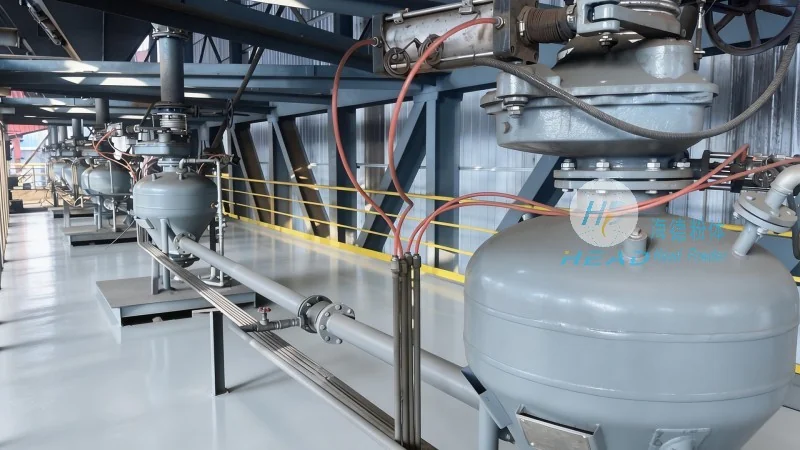
The versatility of the pulse dust collector material pneumatic conveying line makes it suitable for a wide range of applications. For instance, in pharmaceutical manufacturing, it can be used to transport active pharmaceutical ingredients (APIs) while maintaining strict dust control standards. In food processing, it can handle powders such as flour or sugar with minimal contamination risk. In chemical industries, it can convey various powders and granules while ensuring compliance with environmental regulations. These applications demonstrate the system's ability to meet the specific needs of different industries while providing reliable performance.
In conclusion, the pulse dust collector material pneumatic conveying line is a highly effective solution for material handling and dust control in industrial settings. Its integration of pneumatic conveying technology with pulse dust collection mechanisms ensures efficient operation, high air quality, and reliable performance. With its advantages in flexibility, safety, and cost-effectiveness, this system is an ideal choice for modern industrial operations. The system's design and functionality are tailored to meet the demands of various industries, making it a valuable asset for companies seeking to optimize their material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top