

What is a Potash Powder Pneumatic Conveying System? And What Are Its Design Principles?
Potash, a crucial nutrient for agricultural productivity, is often handled in bulk quantities, necessitating efficient and reliable transportation methods. The potash powder pneumatic conveying line is a specialized system engineered to transport potash powder from storage to processing or packaging areas. This technology leverages pneumatic conveying principles, utilizing air to move the powder through a network of pipes and components. Understanding this system is essential for industries involved in fertilizer production and distribution.

Understanding the Core Function of Potash Powder Pneumatic Conveying Lines
The primary function of a potash powder pneumatic conveying line is to transport potash powder in a dust-free, efficient manner. Unlike traditional mechanical conveyors, which can generate dust and require more maintenance, pneumatic systems offer a more hygienic and flexible solution. The system operates by creating a flow of air that either pulls or pushes the powder through the pipeline, ensuring minimal product loss and contamination. This is particularly critical for potash, which is sensitive to moisture and can degrade if not handled properly.
Design Principles Behind Potash Powder Pneumatic Conveying Systems
The design of a potash powder pneumatic conveying system adheres to several key principles to ensure optimal performance. First, the system must accommodate the specific properties of potash powder, such as its particle size, moisture content, and flowability. Engineers design the system with appropriate pipe diameters, air velocities, and pressure levels to prevent blockages and ensure smooth flow. Second, the system incorporates dust control measures, including filters and cyclones, to minimize environmental impact and maintain product quality. Third, the design considers the overall layout and integration with existing facilities, ensuring that the system can be installed and operated efficiently.
Key Components and Their Roles in the System
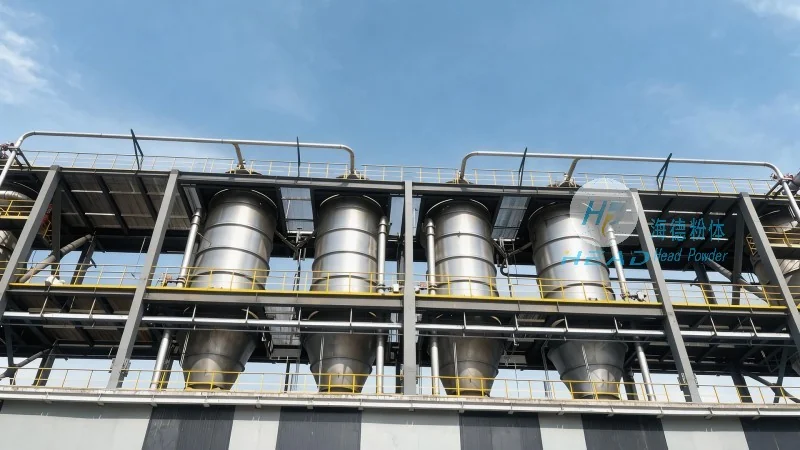
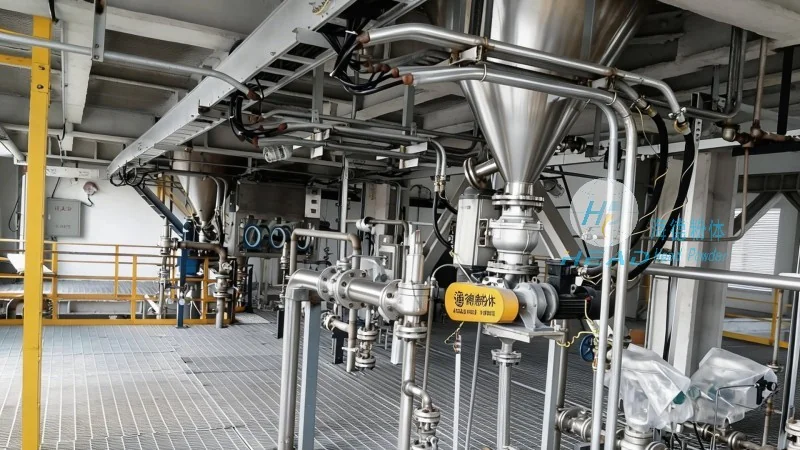
A potash powder pneumatic conveying system comprises several critical components, each playing a vital role in the overall operation. The main components include the hopper or storage silo, which holds the potash powder; the air compressor or blower, which generates the air flow; the pipeline network, which transports the powder; the dust collector or filter, which removes airborne particles; and the discharge unit, which delivers the powder to the next stage. The hopper is designed to maintain the powder's flowability, often with a conical shape and a discharge valve. The air compressor provides the necessary pressure to move the powder through the pipeline, with adjustable settings to control flow rate. The pipeline network is typically made of stainless steel or other corrosion-resistant materials to withstand the chemical properties of potash. The dust collector uses filtration or cyclonic separation to capture fine particles, preventing them from being released into the environment. The discharge unit, such as a rotary valve or a venturi, controls the release of the powder into the next process.
Application Scenarios and Benefits of Using Such Systems
Potash powder pneumatic conveying systems are widely utilized in various industrial applications, especially in the fertilizer industry. They are commonly employed in potash production facilities, where the powder is transported from storage to grinding or packaging units. The system is also used in bulk handling operations, such as in ports or terminals, where potash is loaded onto trucks or ships. The benefits of using pneumatic conveying systems for potash powder include improved safety, as there is no direct contact with the powder, reduced labor costs due to automated operation, and enhanced product quality due to minimal exposure to moisture and contaminants. Additionally, the system is flexible and can be easily scaled to accommodate changes in production volume, making it a cost-effective solution for long-term use.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of potash powder pneumatic conveying systems. With a strong focus on innovation and quality, the company has developed advanced solutions tailored to the specific needs of the fertilizer industry. HeadPowder's systems are designed to meet the highest standards of efficiency, reliability, and safety. The company's headquarters is located in Shandong, China, where it has a team of experienced engineers and technicians dedicated to research and development. HeadPowder provides comprehensive services, including system design, installation, and maintenance, ensuring that clients receive a complete solution for their potash powder handling needs. The company's commitment to customer satisfaction and product excellence has made it a trusted partner in the industry.