

Working Principle and Characteristics of High-Pressure Bin Pump Material Pneumatic Conveying
High-pressure bin pump systems represent a sophisticated method for material handling and transportation, particularly in industrial applications where efficient and reliable movement of bulk materials is critical. This technology, often referred to as pneumatic conveying, utilizes compressed air or gas to transport solid materials through a pipeline network. The high-pressure bin pump, as a key component in this system, plays a pivotal role in the entire process, ensuring smooth and consistent material flow from storage bins to processing or packaging units. By leveraging the power of compressed air, these systems offer a flexible and versatile solution for industries dealing with various types of bulk materials, from fine powders to coarse granules.
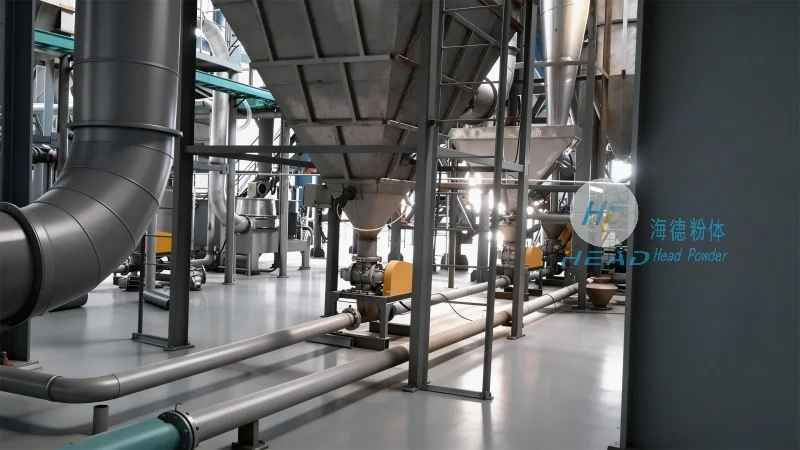
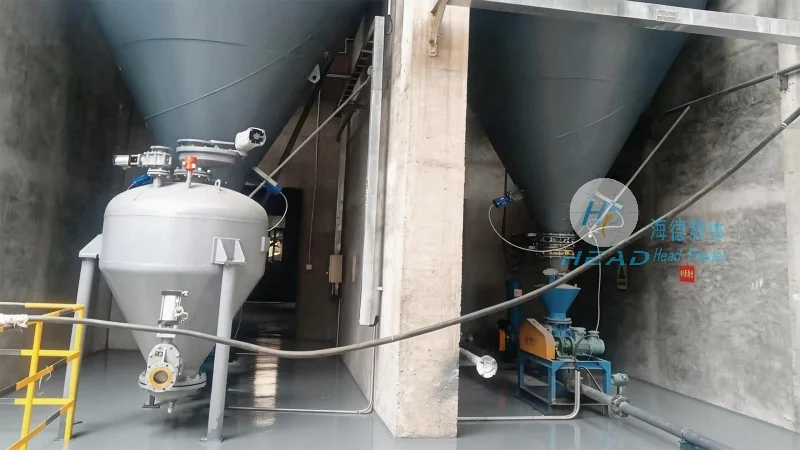
Working Principle of High-Pressure Bin Pump Material Pneumatic Conveying
The operation of a high-pressure bin pump system begins with the loading of bulk materials into a storage bin or hopper. The bin is equipped with a valve or feeder that controls the release of material into the pump's inlet. As the material enters the pump, it is mixed with a high-pressure air stream, creating a slurry or suspension. The pump then uses a positive displacement mechanism, such as a rotary lobe or piston, to compress this mixture and force it through the conveying pipeline. The high pressure generated by the pump ensures that the material is transported over long distances or through complex network configurations without the need for additional mechanical components like conveyors or elevators. The system typically includes a receiver or discharge bin at the end of the pipeline, where the material is separated from the air and collected for further use. The entire process is controlled by a programmable logic controller (PLC) or other automation systems, allowing for precise regulation of flow rates, pressure, and material discharge. This control system ensures that the operation is optimized for efficiency and safety, minimizing energy consumption and preventing material blockages or system failures.
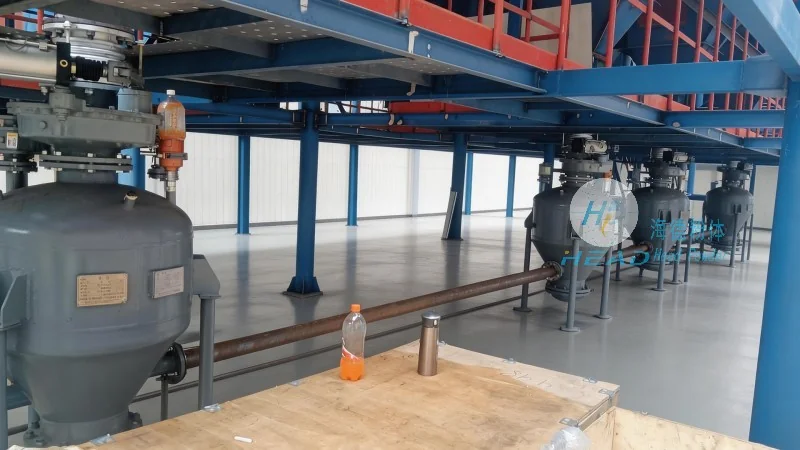
Key Characteristics and Advantages of High-Pressure Bin Pump Systems
High-pressure bin pump systems offer several distinct advantages that make them suitable for a wide range of industrial applications. One of the primary characteristics is their ability to handle a variety of materials, including powders, granules, and even bulk solids with varying moisture content or particle sizes. The system's design allows for flexible material handling, as it can be configured to transport materials over long distances, through vertical or horizontal pipelines, and even around obstacles or changes in elevation. Another key characteristic is the high efficiency and low maintenance requirements. Unlike traditional mechanical conveyors, which may require regular cleaning and maintenance, the pneumatic system operates with minimal moving parts, reducing downtime and operational costs. Additionally, the system provides excellent material containment, as the entire process is enclosed within a pipeline network, preventing dust emissions and ensuring a clean working environment. The high-pressure operation also enables the system to handle materials that are difficult to transport by other means, such as abrasive or corrosive substances, without causing wear or damage to the equipment. Furthermore, the system's scalability allows for easy expansion or modification to accommodate changing production needs, making it a versatile solution for industrial material handling. The energy efficiency of high-pressure bin pumps is another notable advantage, as they can achieve high material throughput with relatively low power consumption compared to other conveying methods. This makes them an environmentally friendly choice for industries looking to reduce their carbon footprint while maintaining operational productivity.
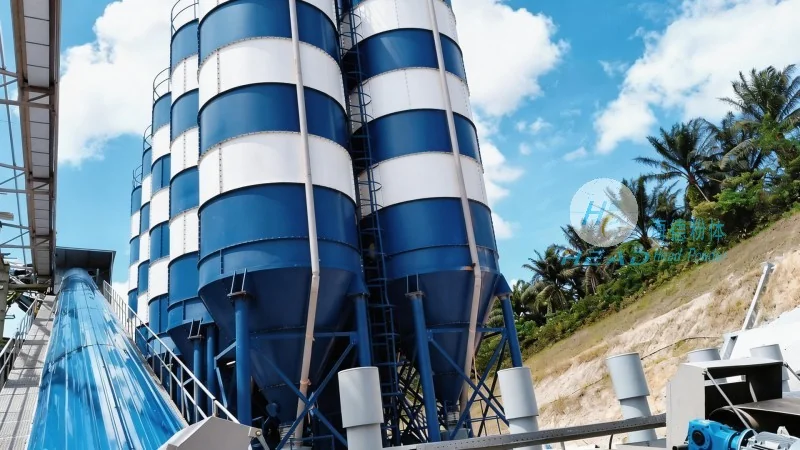
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of high-quality material handling equipment, including high-pressure bin pump systems. With a strong commitment to innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the industrial sector, providing reliable and efficient solutions for material transportation and processing. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled workforce. HeadPowder's products are designed to meet the diverse needs of various industries, including chemical, pharmaceutical, food processing, and mining, ensuring that customers receive tailored solutions that enhance their operational efficiency and productivity. The company's focus on quality control and customer support has earned it a reputation for excellence in the market, making it a preferred choice for businesses seeking durable and reliable material handling equipment. HeadPowder adheres to international quality standards and continuously invests in research and development to improve its product line, ensuring that clients benefit from the latest advancements in material handling technology. The company's team of experts provides comprehensive technical support, from system design and installation to maintenance and troubleshooting, ensuring that customers receive the best possible service throughout the product lifecycle. By partnering with HeadPowder, industries can achieve improved material handling performance, reduced operational costs, and enhanced safety in their production processes.