With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial applications involving the transport of calcium carbonate powder, a pneumatic conveying system offers an efficient and reliable solution. This technology is widely used in the chemical, food, and pharmaceutical industries due to its ability to handle fine powders like calcium carbonate with minimal dust and contamination. The system's design and operation are tailored to meet the specific requirements of material handling, ensuring consistent performance and safety.
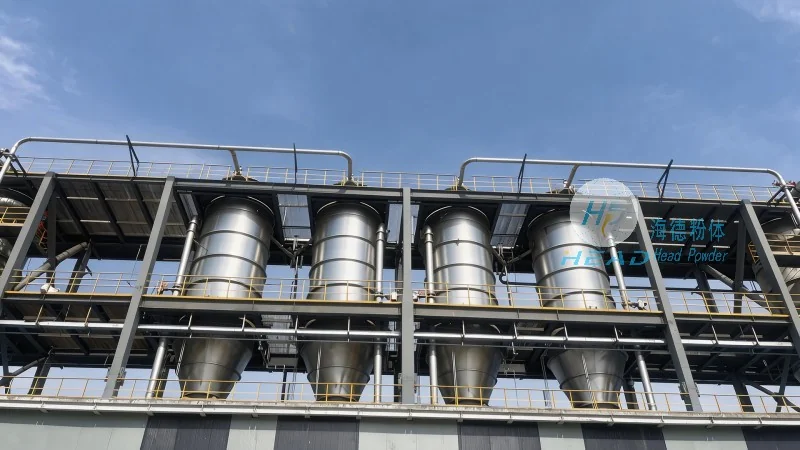
A pneumatic conveying system for calcium carbonate powder operates by using air or gas to transport the material from one location to another. The system typically consists of a hopper, a blower or compressor, a pipeline, and a receiver. The calcium carbonate powder is fed into the hopper, where it is then drawn into the pipeline by the moving air stream. The air velocity is carefully controlled to ensure the powder is carried along without clogging or degradation.
The core of the pneumatic conveying system lies in the interaction between the air flow and the powder particles. As the air is forced through the pipeline at a high velocity, it creates a negative pressure that pulls the powder particles into the stream. The powder is then suspended in the air and transported to the destination. The system can operate in either positive or negative pressure modes, depending on the application and the distance of the material transport. Positive pressure systems are suitable for short-distance transport, while negative pressure systems are ideal for longer distances or when handling dust-sensitive materials.
Several key features make this system particularly effective for calcium carbonate powder handling:
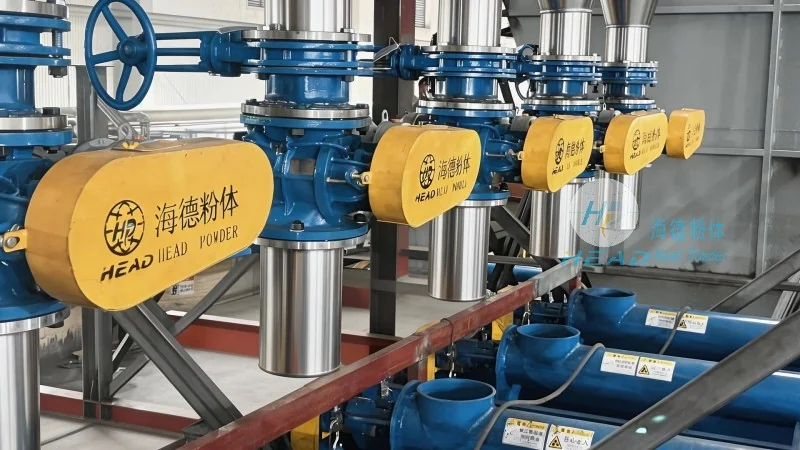
1. Low Dust and Contamination: The enclosed pipeline design minimizes dust emissions, which is crucial for maintaining a clean working environment and complying with environmental regulations. This is especially important in industries where product purity is paramount.
2. Efficient Material Transport: The system allows for continuous and uninterrupted material flow, reducing downtime and increasing overall productivity. The ability to handle fine powders without segregation or agglomeration ensures consistent material quality throughout the process.
3. Space Efficiency: Unlike traditional belt or bucket elevators, pneumatic conveying systems require less floor space and can be installed in various configurations, including vertical or horizontal layouts, to fit the specific needs of the facility.
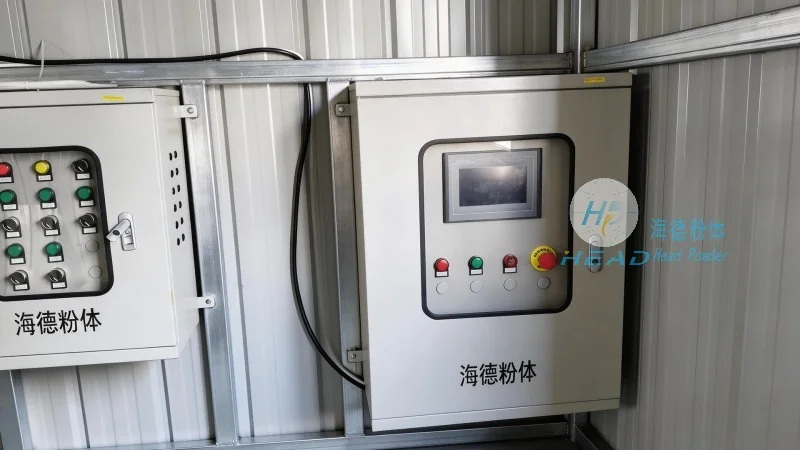
4. Flexibility in Layout: The modular design of the system enables easy integration into existing production lines or new installations. It can be adapted to handle varying material volumes and transport distances, making it a versatile solution for different industrial applications.
The calcium carbonate powder pneumatic conveying system is widely used in various industries, including the production of paper, plastics, coatings, and food products. The benefits of this technology include improved product quality, reduced labor costs, and enhanced safety in the workplace. By eliminating manual handling of powders, the system minimizes the risk of dust exposure and related health issues, contributing to a safer working environment.
In conclusion, the pneumatic conveying system for calcium carbonate powder is a highly effective and efficient solution for material handling in industrial settings. Its working principle, which relies on air flow to transport fine powders, offers several advantages over traditional methods, including low dust emissions, high efficiency, and space-saving design. The system's features and benefits make it an ideal choice for companies seeking to improve their production processes and maintain product quality. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of clients, ensuring optimal performance and reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top