With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Wheat flour conveying is a critical process in the flour milling industry, ensuring efficient and safe movement of flour from storage to processing or packaging areas. The choice of conveying method significantly impacts operational efficiency, product quality, and overall production costs. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. (commonly known as HeadPowder) offers a range of advanced solutions tailored to meet diverse industrial needs. This article explores the various methods available for wheat flour conveying, highlighting key considerations and applications.
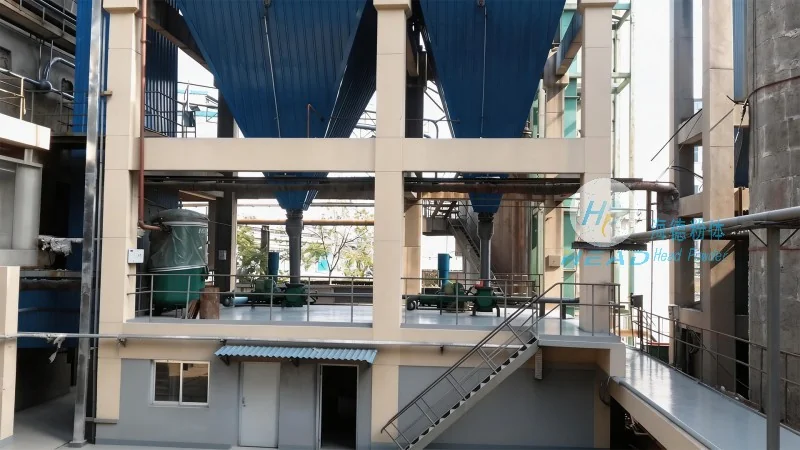
Screw conveyors, also known as auger conveyors, are a popular choice for wheat flour conveying due to their simplicity and effectiveness. These systems consist of a rotating helical screw inside a cylindrical tube, which moves flour through the conveyor by pushing it forward. HeadPowder’s screw conveyors are designed with high-quality materials, such as stainless steel or food-grade plastics, to ensure durability and compliance with hygiene standards. The smooth, polished surfaces prevent flour buildup and contamination, making them ideal for handling fine powders like wheat flour. These conveyors are particularly suitable for short to medium-distance transport, vertical lifting, and horizontal movement. They offer consistent flow rates and can be easily integrated into existing flour milling systems. The design allows for easy cleaning and maintenance, reducing downtime and operational costs. HeadPowder’s screw conveyors are engineered to handle varying flour types, including whole wheat, white flour, and specialty flours, ensuring reliable performance in different production scenarios.
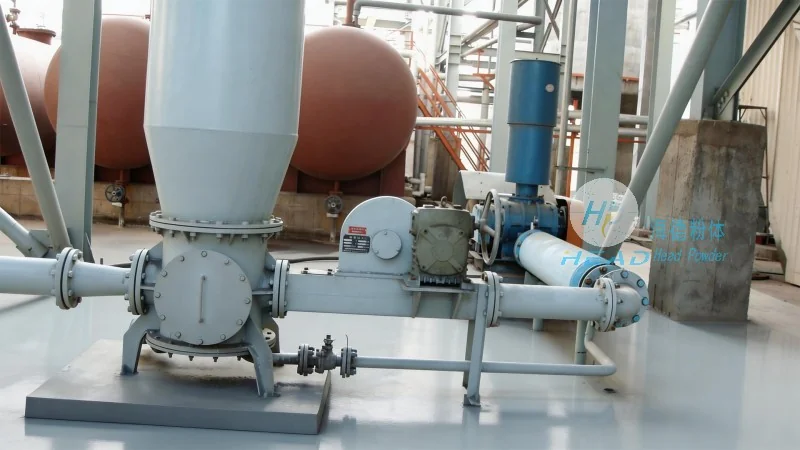
Pneumatic conveying systems use air pressure to transport wheat flour in a closed pipeline. This method is highly effective for long-distance and high-volume conveying, offering advantages such as reduced dust, minimal product contamination, and the ability to handle both dry and wet flour mixtures. HeadPowder’s pneumatic conveying systems are available in both positive and negative pressure configurations. Positive pressure systems blow air through the pipeline, pushing flour forward, while negative pressure systems create a vacuum to draw flour into the system. These systems are particularly useful for transporting flour over distances of several hundred meters and for integrating with existing dust collection systems. The design of HeadPowder’s pneumatic conveyors includes advanced filtration and separation components to maintain flour quality and prevent clogging. The systems are equipped with variable speed drives and pressure sensors, allowing for precise control of flow rates and ensuring consistent performance. Pneumatic conveying is ideal for applications requiring high-speed, continuous transport and for environments where dust control is a priority. HeadPowder’s expertise in pneumatic technology ensures that these systems are optimized for efficiency and reliability in wheat flour handling.
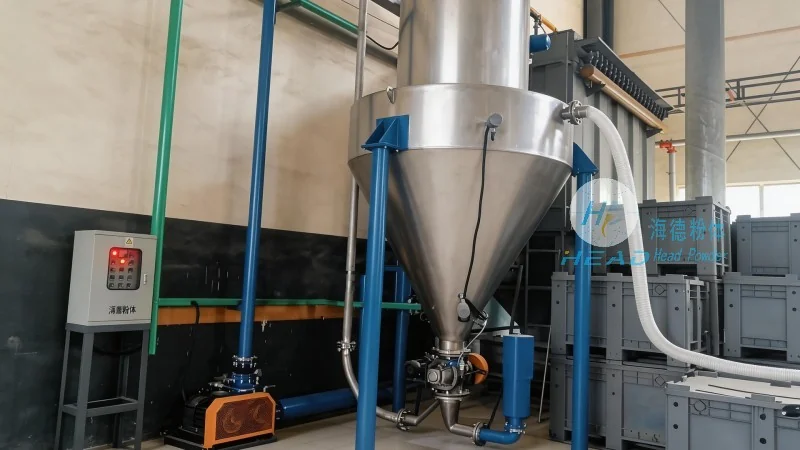
Bucket elevators are essential for vertical transport of wheat flour, enabling efficient movement from lower to upper levels in flour mills. These systems consist of a series of buckets attached to a belt or chain, which travels through a vertical or inclined frame. As the buckets move upward, they scoop up flour and discharge it at the top. HeadPowder’s bucket elevators are designed with heavy-duty construction to handle the abrasive nature of wheat flour and the continuous operational demands of milling plants. The buckets are made from durable materials, such as rubber or metal, with smooth edges to prevent flour sticking and ensure smooth discharge. The elevator frames are equipped with safety guards and emergency stop mechanisms, ensuring operational safety. These systems offer high capacity and can handle large volumes of flour with minimal energy consumption. HeadPowder’s bucket elevators are available in various configurations, including belt and chain types, to suit different production capacities and space constraints. The design allows for easy maintenance, with accessible components and quick replacement of buckets. Vertical transport via bucket elevators is crucial for optimizing floor space and improving workflow in flour mills, making them a vital component of efficient flour processing.
Belt conveyors are widely used for horizontal transport of wheat flour, providing a reliable and cost-effective solution for moving flour over short to medium distances. These systems consist of a continuous belt supported by rollers, which moves flour from one point to another. HeadPowder’s belt conveyors are designed with high-strength belts, often made from food-grade materials, to ensure durability and resistance to flour abrasion. The conveyor frames are constructed from stainless steel or other corrosion-resistant materials, ensuring hygiene and longevity. These systems are equipped with adjustable speed controls and load sensors, allowing for precise control of flour flow and preventing overloading. Belt conveyors are particularly suitable for applications requiring gentle handling of flour, as the smooth belt surface minimizes product damage. HeadPowder’s belt conveyors can be customized with additional features, such as side guides, diverters, and accumulation zones, to enhance functionality and adapt to specific production needs. The design allows for easy integration with other conveying equipment, such as screw or pneumatic systems, creating a comprehensive flour handling solution. Horizontal belt conveyors are essential for connecting storage silos, processing units, and packaging lines, ensuring seamless workflow and efficient production in flour mills.
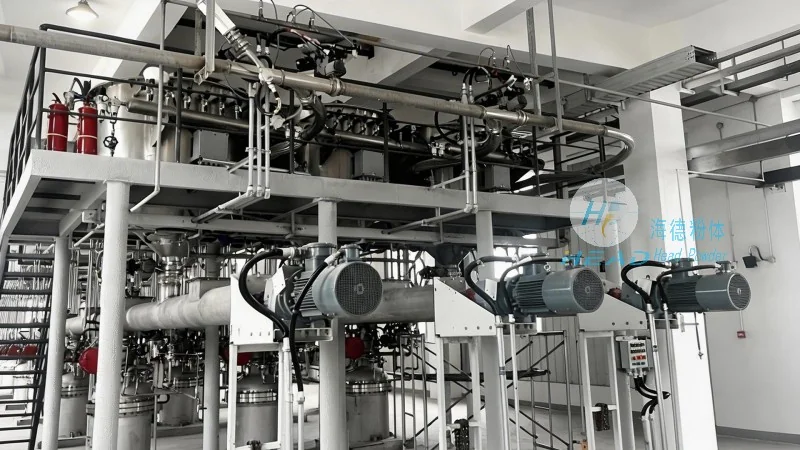
For many flour mills, a single conveying method may not be sufficient to meet all operational requirements. HeadPowder offers combined or integrated conveying solutions that combine multiple technologies to optimize flour handling. These systems may include a combination of screw conveyors, pneumatic conveyors, and bucket elevators, designed to handle different stages of flour processing. For example, a typical system might use a screw conveyor to transport flour from a storage silo to a bucket elevator for vertical lifting, followed by a pneumatic conveyor to move it to a packaging line. The integration of these components allows for seamless flow and minimal downtime, improving overall production efficiency. HeadPowder’s engineers work closely with clients to design customized conveying systems that align with their specific production goals, space constraints, and budget considerations. The combined solutions are equipped with advanced control systems, allowing for centralized monitoring and automation of the conveying process. This not only enhances operational efficiency but also reduces labor costs and improves product quality. By leveraging a combination of technologies, HeadPowder’s integrated conveying solutions provide a comprehensive approach to wheat flour handling, ensuring that all aspects of the process are optimized for performance and reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top