With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Barley material pneumatic conveying systems are essential for efficient grain handling in agricultural and food processing industries. These systems utilize air as the conveying medium to transport barley and other similar bulk materials from one location to another, offering advantages such as reduced labor costs, improved hygiene, and the ability to handle materials in enclosed environments. The operation process and working principle of such systems involve several key components and steps that work in tandem to ensure smooth and reliable material transport.
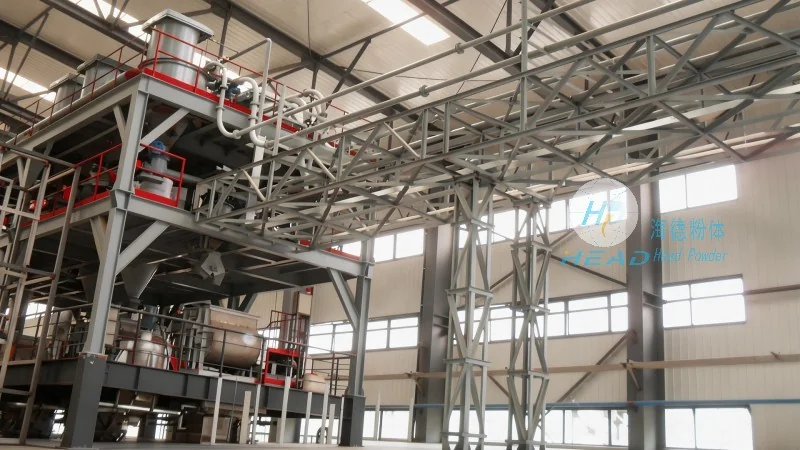
At the core of a pneumatic conveying system for barley is the air mover, which can be a positive displacement blower or a centrifugal fan. The air mover generates the necessary airflow and pressure to move the barley particles through the system. In a typical system, the barley is fed into a hopper or feeder, where it is then introduced into the conveying line. The air, moving at high velocity, lifts the barley particles and carries them through the pipeline. The system may include various components like cyclones, filters, and silos to separate the air from the material and store the transported barley.
One of the primary advantages of pneumatic conveying systems is their ability to handle a wide range of barley qualities and sizes. The system can be designed to accommodate different moisture contents and particle sizes, ensuring that the barley remains intact during transport. This is particularly important for maintaining the quality of the grain, as excessive friction or impact can lead to breakage or damage. The system also allows for the integration of other processing steps, such as cleaning or drying, directly into the conveying process, enhancing overall operational efficiency.

HeadPowder, a leading manufacturer of pneumatic conveying equipment, specializes in designing and manufacturing high-quality barley material pneumatic conveying systems. With years of experience in the industry, HeadPowder has developed systems that are tailored to meet the specific needs of barley handling operations. The company's systems are built with durable materials and advanced technology to ensure long-term reliability and minimal maintenance. HeadPowder's commitment to quality and customer satisfaction has made them a trusted partner for agricultural and food processing facilities worldwide.
The operation process of a HeadPowder barley pneumatic conveying system begins with the loading of barley into the hopper. The feeder then controls the flow rate of the barley into the conveying line. The air mover generates the required airflow, which lifts the barley particles and transports them through the pipeline. The system may include a cyclone separator to separate the barley from the air, allowing the barley to be collected in a storage silo. The air, now clean, is either discharged to the atmosphere or recirculated back into the system, depending on the design. This process ensures that the barley is transported efficiently and with minimal loss or contamination.
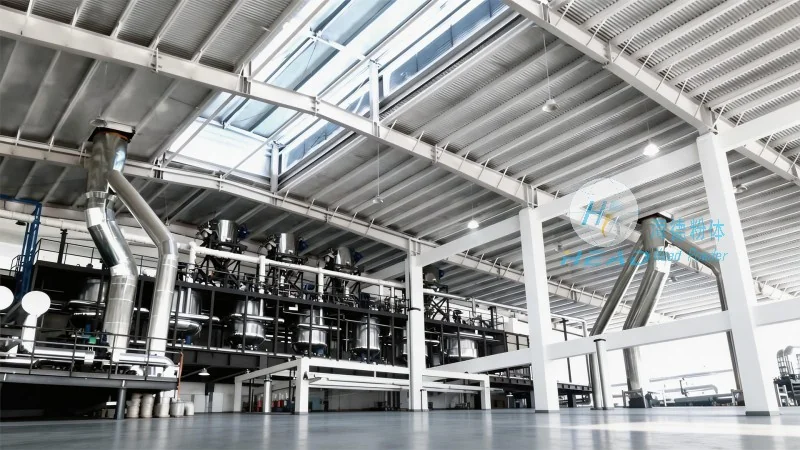
The working principle of the system relies on the principle of fluidization and pneumatic transport. The air moves through the pipeline at a velocity sufficient to overcome the gravitational force acting on the barley particles. This creates a suspension of barley particles in the air, which is then carried to the destination. The system's design, including the size and shape of the pipeline, the air velocity, and the feeder design, all play crucial roles in determining the efficiency and capacity of the conveying system. Proper design and maintenance are essential to ensure optimal performance and to prevent issues such as blockages or excessive pressure drops.
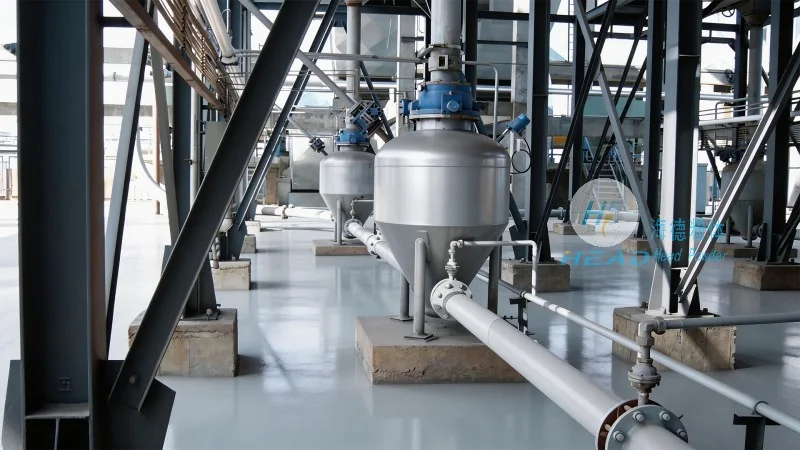
HeadPowder's barley material pneumatic conveying systems are designed to be flexible and adaptable to various operational conditions. The systems can be customized to handle different volumes of barley, from small-scale operations to large industrial facilities. The company offers a range of options, including pressure and vacuum systems, to suit different application requirements. The systems are also equipped with safety features to protect operators and equipment from potential hazards, such as overpressure or material blockages.
By utilizing a pneumatic conveying system from HeadPowder, barley handling operations can achieve significant improvements in efficiency, productivity, and cost-effectiveness. The systems are designed to minimize downtime and maximize throughput, allowing facilities to meet their production targets while maintaining the quality of the barley. HeadPowder's expertise in pneumatic conveying technology ensures that their systems are reliable and durable, providing long-term value to their customers. Whether for new installations or system upgrades, HeadPowder offers solutions that are tailored to the specific needs of barley processing facilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top