With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for sulfur handling. This article explores the fundamental principles behind sulfur pneumatic conveying technology and highlights key application scenarios where such systems are employed effectively.
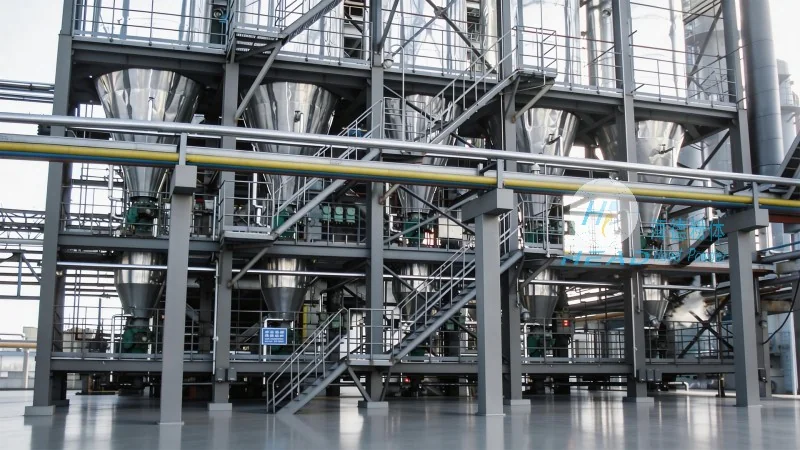
The core principle of sulfur pneumatic conveying involves transporting solid sulfur particles through a pipeline using a pressurized air or gas stream. This method eliminates the need for mechanical components like conveyors or elevators, reducing friction and wear while ensuring a clean and efficient transfer process. The system typically operates by generating a high-pressure air flow that draws sulfur particles into the pipeline, where they are carried to the destination point. The design of the system, including the air velocity, pipeline diameter, and pressure levels, is critical to ensure stable and reliable transport of sulfur, which can vary in form from granular to powdered depending on the application.
A typical sulfur pneumatic conveying system comprises several essential components that work in tandem to achieve efficient material transport. These include a dust collector or air filter to remove particulate matter from the air stream, a blower or compressor to generate the necessary pressure, a hopper or storage silo to hold the sulfur, and a pipeline network that connects the source to the discharge point. The system may also incorporate control valves, pressure sensors, and monitoring equipment to regulate the flow and ensure safe operation. Each component is carefully selected and sized based on the specific characteristics of the sulfur being conveyed, such as its density, moisture content, and particle size distribution.
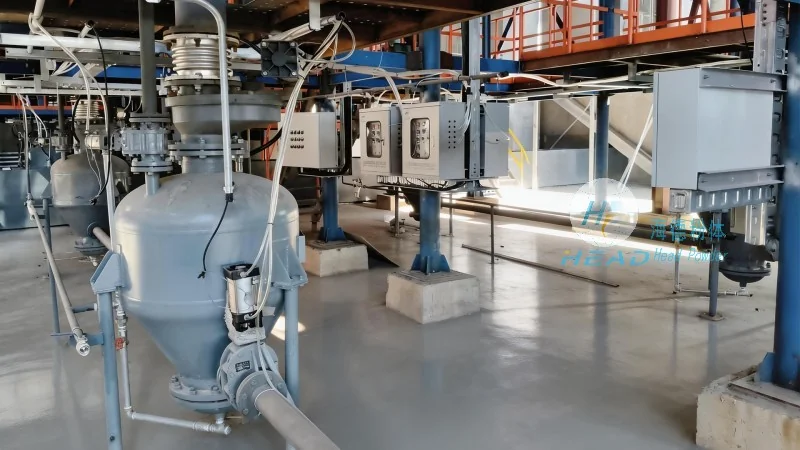
Sulfur pneumatic conveying systems are widely used in various industrial settings due to their flexibility and efficiency. One common application is in the chemical industry, where sulfur is transported from storage facilities to processing units or reactors. The system allows for a continuous and automated transfer of sulfur, reducing manual handling and minimizing the risk of contamination or spills. Another key application is in the fertilizer manufacturing sector, where sulfur is used as a raw material for producing sulfur-based fertilizers. The pneumatic conveying system ensures that sulfur is delivered to the production line in a controlled manner, maintaining consistent quality and reducing downtime. Additionally, in the petrochemical industry, sulfur is often handled as a byproduct of refining processes, and pneumatic conveying systems provide a safe and effective means of transporting it to storage or disposal facilities. The operational advantages of these systems include reduced labor costs, improved safety by minimizing direct contact with sulfur, and enhanced process efficiency through continuous flow.
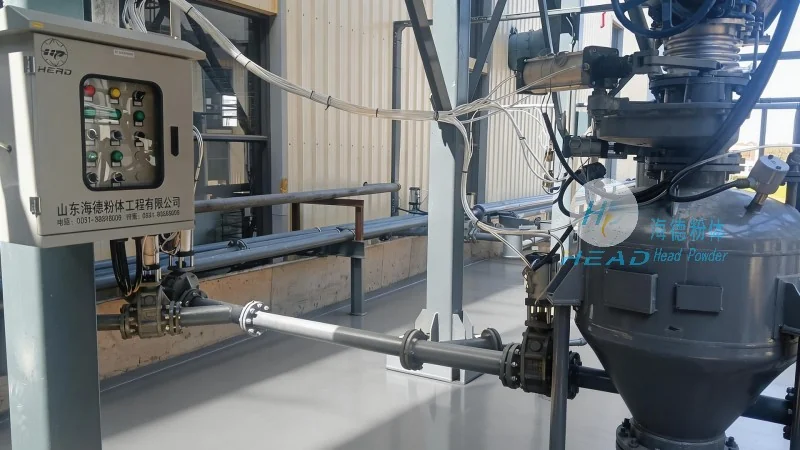
Designing an optimal sulfur pneumatic conveying system requires careful consideration of several factors to ensure long-term performance and reliability. The choice of pipeline material is crucial, as sulfur can be corrosive and abrasive, potentially damaging metal or plastic components over time. Stainless steel or specialized coatings are often used to protect the pipeline from sulfur attack. Additionally, the system must be designed to handle variations in sulfur properties, such as changes in moisture content or particle size, which can affect the flow characteristics. Regular maintenance is essential to prevent blockages or system failures. This includes cleaning the pipeline and filters regularly, inspecting components for wear or corrosion, and monitoring pressure and flow rates to detect any issues early. Proper maintenance not only extends the lifespan of the system but also ensures consistent performance and compliance with safety regulations.
HeadPowder's expertise in sulfur pneumatic conveying systems enables the company to provide tailored solutions for a wide range of industrial applications. By leveraging advanced engineering principles and robust system design, HeadPowder ensures that clients can benefit from efficient, safe, and reliable sulfur transport. Whether for chemical processing, fertilizer production, or petrochemical applications, the company's systems are designed to meet the specific needs of each project, delivering optimal performance and operational advantages. With a strong presence in Shandong, China, HeadPowder continues to be a trusted partner for industries requiring advanced material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top