With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading manufacturer in the field of powder handling technology, specializes in providing advanced solutions for the safe and efficient transportation of bulk powders. This article delves into the operation process and working principle of nitrogen-protected powder handling equipment, highlighting how these systems ensure product integrity and operational safety.
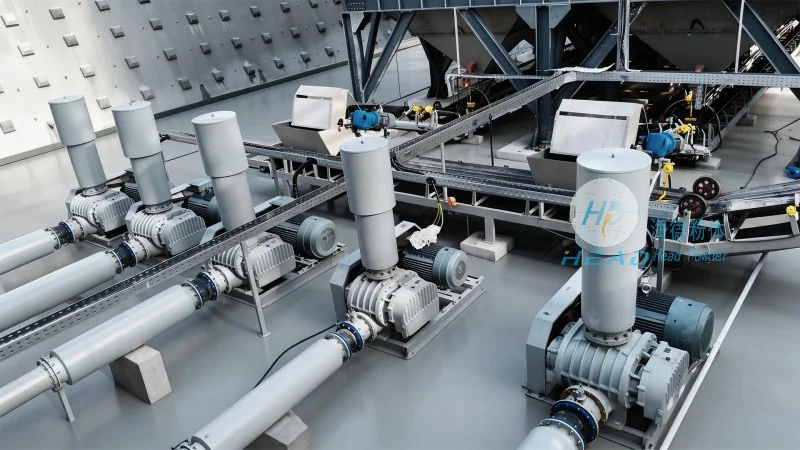
HeadPowder, operating under the full name Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. The company is dedicated to developing innovative powder handling equipment that meets the stringent requirements of various industries, including pharmaceuticals, food processing, and chemical manufacturing. With a focus on quality and reliability, HeadPowder has established itself as a trusted partner for businesses seeking to optimize their powder handling processes.
Nitrogen-protected powder handling equipment is designed to maintain an inert atmosphere within the system, preventing oxidation, moisture absorption, and contamination of the powder. This is particularly critical for sensitive materials such as pharmaceuticals, food ingredients, and fine chemicals, where product quality and shelf life are paramount. The system typically consists of several key components, including a nitrogen gas supply, a pressure control system, and a powder handling unit, all working in concert to ensure a controlled environment.
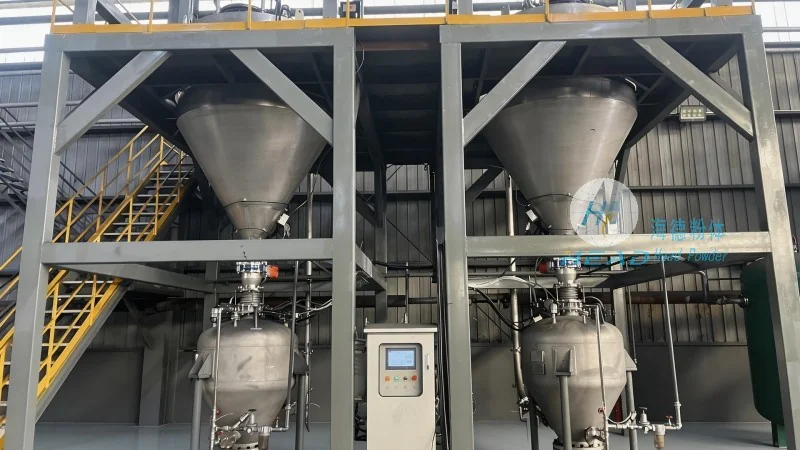
The nitrogen-protected powder handling system comprises several essential components that work together to achieve the desired operational outcomes. The nitrogen gas supply unit provides a continuous flow of high-purity nitrogen, which is introduced into the system to displace air and create an inert environment. The pressure control system monitors and regulates the pressure within the equipment, ensuring it remains within safe operating limits. The powder handling unit, which may include hoppers, conveyors, and valves, is responsible for the actual movement of the powder through the system. Each component plays a vital role in maintaining the integrity of the powder and preventing any potential hazards.
The operation of nitrogen-protected powder handling equipment follows a systematic process to ensure safe and efficient powder transfer. The process typically begins with the preparation of the system, which involves checking the nitrogen gas supply, verifying the pressure levels, and ensuring all components are properly sealed. Once the system is ready, the nitrogen gas is introduced to create an inert atmosphere. The powder is then loaded into the hopper, and the conveyor system begins to transport the powder through the system. The pressure control system continuously monitors the pressure, adjusting the nitrogen flow as needed to maintain the desired conditions. The powder is discharged from the system at the end of the process, ready for further processing or packaging.
The working principle of nitrogen-protected powder handling equipment is based on the principle of inert gas purging. By introducing nitrogen gas into the system, the air is displaced, creating an environment where oxidation and moisture absorption are minimized. This helps to preserve the quality and stability of the powder, extending its shelf life and ensuring it meets the required specifications. The system also prevents the formation of static electricity, which can be a significant hazard in powder handling operations. The combination of nitrogen purging and proper sealing ensures that the powder remains free from contamination and maintains its original properties throughout the handling process.
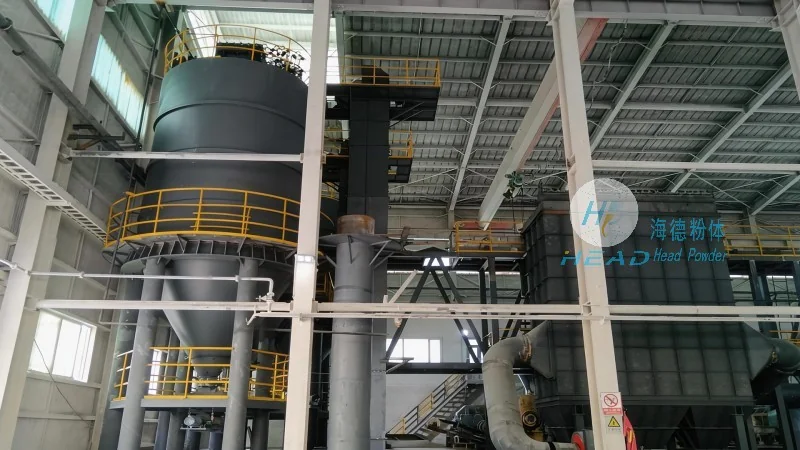
Implementing nitrogen-protected powder handling equipment offers several significant benefits for businesses. Firstly, it enhances product quality by preventing oxidation and moisture damage, which can affect the performance and shelf life of the powder. Secondly, it improves operational safety by reducing the risk of fire or explosion due to static electricity or oxygen presence. Thirdly, it increases efficiency by maintaining consistent flow rates and reducing downtime caused by material degradation. For industries dealing with sensitive materials, the use of nitrogen-protected systems is not just a best practice but a necessity to meet regulatory requirements and maintain customer trust.
HeadPowder's nitrogen-protected powder handling equipment represents a sophisticated solution for the safe and efficient transportation of bulk powders. By understanding the operation process and working principle of these systems, businesses can optimize their powder handling operations, enhance product quality, and ensure compliance with industry standards. With its headquarters in Shandong, China, HeadPowder continues to innovate and provide reliable solutions that meet the evolving needs of the powder handling industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top