With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
When it comes to handling and transporting corn kernels in industrial settings, selecting the right conveying method is crucial for maintaining efficiency, minimizing product damage, and ensuring smooth operations. Shandong HeadPowder Engineering Co., Ltd., a leading provider of specialized engineering solutions, offers a range of advanced corn kernel conveying systems tailored to meet diverse industrial needs. This article explores the key methods used for corn kernel transportation, highlighting the benefits and applications of each approach.
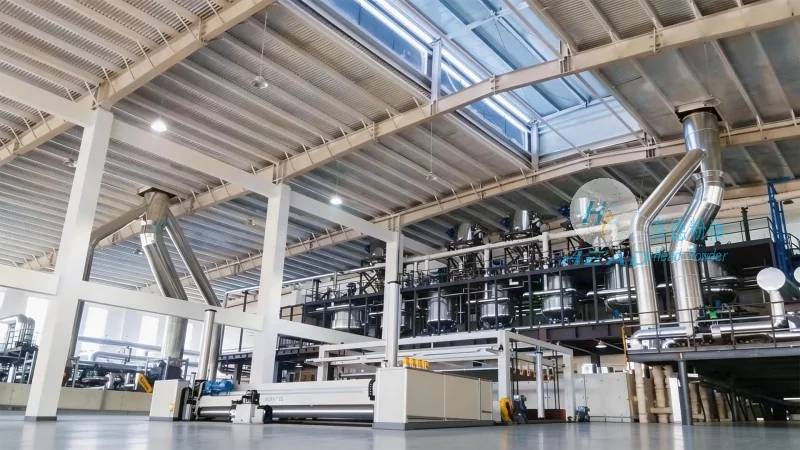
Screw conveyors, also known as auger conveyors, are a widely used method for transporting corn kernels due to their simplicity and reliability. These systems consist of a rotating helical screw inside a trough, which moves material along the length of the conveyor. HeadPowder's screw conveyors are designed with durable materials, such as stainless steel or high-quality carbon steel, to withstand the abrasive nature of corn kernels. The design minimizes product breakage and ensures consistent flow, making it suitable for both horizontal and slight incline applications. The compact structure of these conveyors allows for easy integration into existing processing lines, providing a cost-effective solution for many corn processing facilities.
Pneumatic conveying systems utilize air pressure to move corn kernels through a network of pipes and ducts. This method is ideal for high-volume transport over longer distances, as it can handle large quantities of material with minimal labor. HeadPowder's pneumatic conveying solutions are engineered to maintain product integrity by controlling air velocity and pressure. The systems can be configured as positive or negative pressure, depending on the specific requirements of the corn processing operation. Pneumatic conveyors are particularly effective for transporting corn kernels from storage silos to processing units, ensuring a continuous flow without the need for manual handling. The flexibility of these systems allows for easy reconfiguration to accommodate changes in production volume or layout.
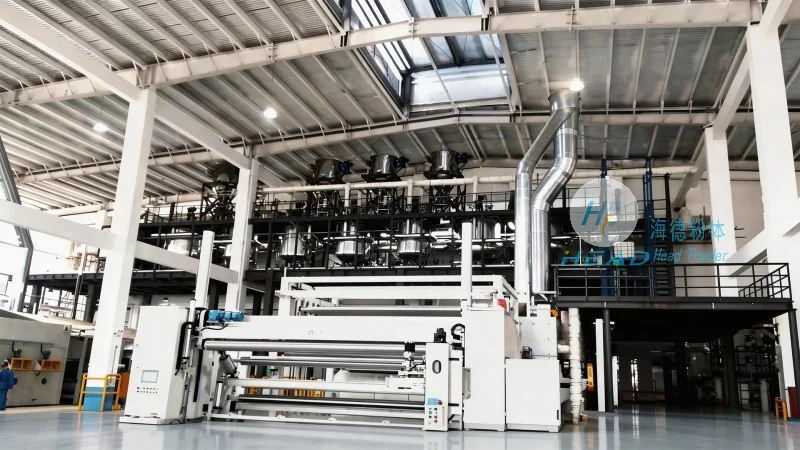
Belt conveyors are another common choice for corn kernel transportation, especially in applications requiring the movement of large volumes of material over longer distances. These systems feature a continuous belt that moves the corn kernels along a fixed path, supported by rollers or idlers. HeadPowder's belt conveyors are constructed with heavy-duty materials, such as rubber or PVC, to provide resistance to wear and tear from the corn kernels. The design allows for efficient transfer of corn kernels from one processing stage to another, such as from cleaning to drying or storage. Belt conveyors are also suitable for incline and decline applications, making them versatile for various corn processing workflows. The robust construction ensures long service life and low maintenance costs, contributing to overall operational efficiency.
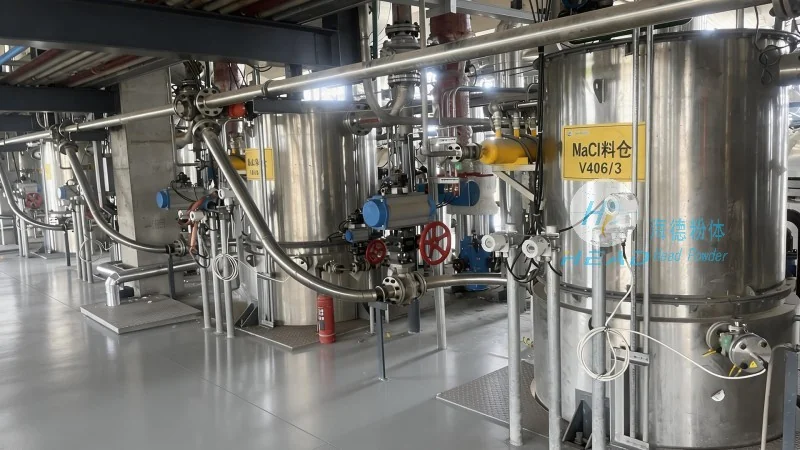
For vertical transport of corn kernels, bucket elevators are an efficient solution. These systems use a series of buckets attached to a chain or belt, which move vertically to lift the corn kernels from lower to higher levels. HeadPowder's bucket elevators are designed with durable buckets and strong chains to handle the weight and abrasiveness of corn kernels. The vertical movement minimizes the need for horizontal space, making them ideal for facilities with limited floor area. Bucket elevators are commonly used in corn processing plants to move corn kernels from storage bins to processing equipment, such as mills or dryers. The high capacity and reliability of these elevators ensure consistent material flow, reducing downtime and improving productivity.
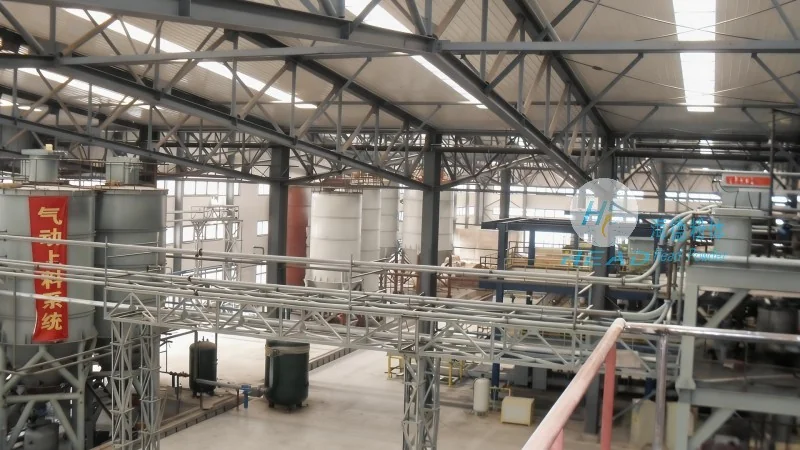
Vibrating conveyors use vibrations to move corn kernels along a trough. This method is particularly suitable for handling corn kernels that are sensitive to impact or abrasion, as it minimizes product damage. HeadPowder's vibrating conveyors are engineered with adjustable vibration frequencies and amplitudes to control the speed and direction of material flow. The gentle movement of the corn kernels ensures that the product remains intact, making it ideal for applications where product quality is paramount. These conveyors are often used in the final stages of corn processing, such as before packaging or further processing. The low noise and energy consumption of vibrating conveyors also contribute to a more sustainable operation.
In conclusion, the choice of corn kernel conveying method depends on several factors, including the volume of material, the distance to be covered, the need for product integrity, and the available space in the processing facility. Shandong HeadPowder Engineering Co., Ltd. offers a comprehensive range of conveying solutions, including screw conveyors, pneumatic systems, belt conveyors, bucket elevators, and vibrating conveyors, to meet the diverse needs of corn processing industries. By selecting the appropriate conveying method, corn processing facilities can enhance operational efficiency, reduce costs, and ensure the quality of their products. With their expertise in engineering and manufacturing, HeadPowder provides reliable and customized solutions that help clients achieve their production goals effectively.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top