With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding the working principle and features of cereal powder pneumatic conveying systems is crucial for industries dealing with bulk powder handling, such as food processing, pharmaceuticals, and chemical manufacturing. These systems offer efficient, reliable, and hygienic methods to transport cereal powders and other fine particulate materials. In this article, we explore the fundamental mechanisms behind these systems and highlight their key characteristics that make them indispensable in modern processing operations.
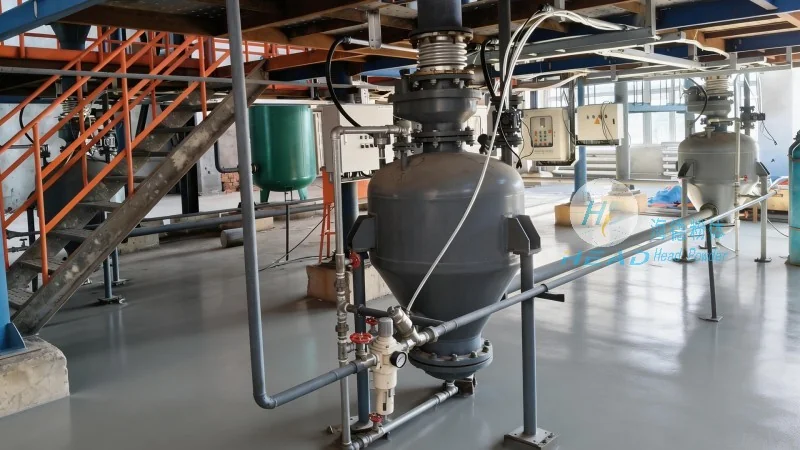
The core of a pneumatic conveying system lies in its ability to use compressed air or vacuum to move powder materials through a pipeline. The system typically consists of a hopper for material storage, a conveyor line, and a receiver for the discharged material. The working principle can be categorized into two main types: pressure and vacuum systems.
In a pressure system, compressed air is introduced into the hopper, creating a pressure differential that forces the powder into the conveyor line. The air and powder mixture travels through the pipeline to the receiver, where the air is separated from the powder, often using a cyclone or filter. This method is suitable for long-distance and high-capacity applications, as it can maintain consistent pressure throughout the system.
Conversely, a vacuum system operates by creating a negative pressure in the receiver, which draws the powder from the hopper through the pipeline. The air and powder mixture is then drawn into the receiver, where separation occurs. Vacuum systems are ideal for short-distance or low-volume applications, as they require less energy and are easier to install in existing facilities.
Both systems rely on the principle of fluidization, where the powder particles are suspended in the air stream, allowing them to move freely through the pipeline. The velocity of the air, the particle size, and the density of the material all influence the efficiency of the conveying process. Proper design of the system, including the diameter of the pipeline and the air velocity, is essential to prevent blockages and ensure smooth operation.
HeadPowder, a leading manufacturer in the field, offers pneumatic conveying systems tailored to the specific needs of cereal powder handling. These systems are characterized by several key features that enhance performance and reliability:
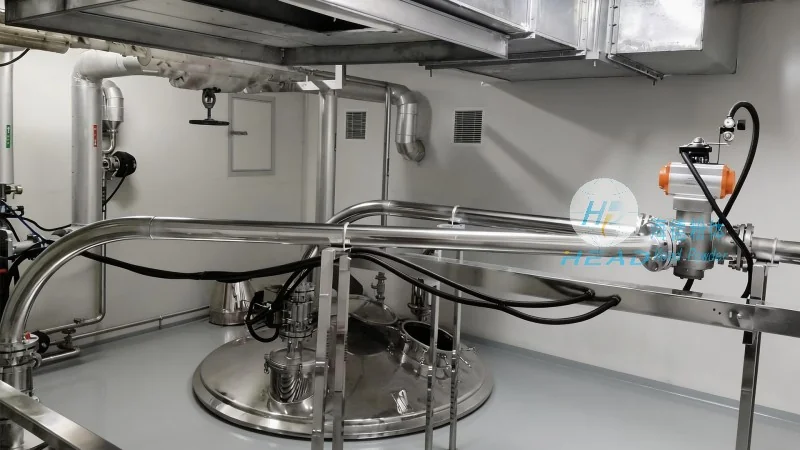
Firstly, the systems are designed for high efficiency and low energy consumption. By optimizing the air velocity and pipeline design, HeadPowder ensures that the conveying process is both effective and economical. This is particularly important for large-scale operations where energy costs can significantly impact overall production expenses.
Secondly, the systems provide a hygienic and dust-free environment. The enclosed pipeline and sealed components prevent contamination from external sources and minimize dust emissions, which is critical in food and pharmaceutical industries where product purity and safety are paramount. HeadPowder's systems are constructed from materials such as stainless steel, ensuring compliance with industry standards and regulations.
Thirdly, the systems offer flexibility and adaptability. They can be customized to handle various types of cereal powders, including wheat, corn, oats, and other grains, with different particle sizes and moisture contents. This versatility allows HeadPowder to serve a wide range of applications, from small-scale processing to large industrial facilities.
Additionally, the systems are equipped with advanced control and monitoring features. Sensors and control panels allow operators to adjust the air pressure, flow rate, and other parameters in real-time, ensuring optimal performance and preventing system failures. HeadPowder's systems are designed for easy maintenance and repair, reducing downtime and increasing overall productivity.
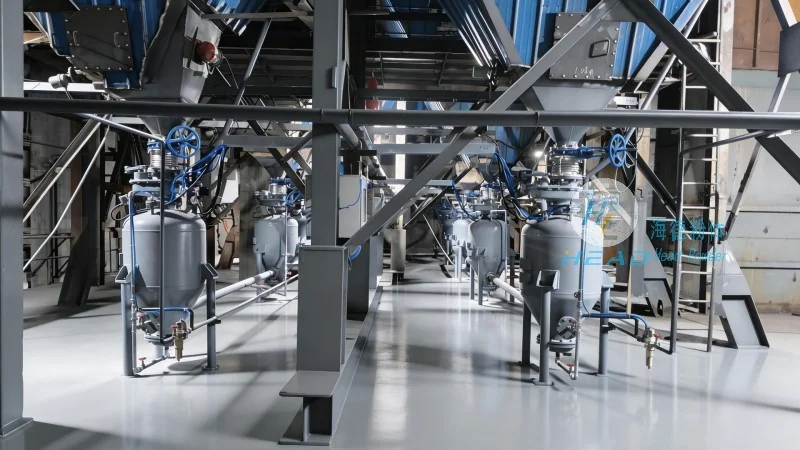
Cereal powder pneumatic conveying systems are widely used in various stages of cereal processing, from raw material handling to finished product packaging. In the milling process, these systems efficiently transport raw grains from storage silos to the milling equipment, ensuring a continuous supply of material. During the grinding and sifting stages, the systems handle fine powders, preventing clogging and maintaining consistent product quality.
In the packaging phase, pneumatic conveying systems are used to transport finished cereal products from the production line to the packaging machines. This ensures that the products are handled gently and without contamination, preserving their freshness and quality. The systems also facilitate the transfer of ingredients for blending and flavoring, allowing for precise control over the final product composition.
The benefits of using pneumatic conveying systems in cereal processing extend beyond efficiency and hygiene. They also contribute to improved safety in the workplace by reducing manual handling of powders, which can be a source of dust exposure and respiratory issues. The enclosed systems minimize the risk of dust explosions, a common concern in powder handling operations.
HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in designing and manufacturing customized pneumatic conveying systems for cereal powder applications. The company's team of engineers and technicians works closely with clients to understand their specific requirements and develop tailored solutions. Whether it's a new installation or an upgrade to an existing system, HeadPowder provides comprehensive support throughout the entire process.
From initial consultation and system design to installation, commissioning, and ongoing maintenance, HeadPowder ensures that clients receive a high-quality product that meets their operational needs. The company's commitment to quality and customer satisfaction has earned it a reputation as a trusted partner in the industry. With a focus on innovation and customer service, HeadPowder continues to deliver reliable and efficient pneumatic conveying systems that enhance the performance of cereal processing operations worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top