

Working Principle and Features of Rubber Granule Pneumatic Conveying Systems
HeadPowder, a leading provider of pneumatic conveying solutions, specializes in rubber granule handling systems. This article explores the working principle and key features of rubber granule pneumatic conveying systems, highlighting how they efficiently transport rubber granules from one location to another.
Introduction to Rubber Granule Pneumatic Conveying Systems
Rubber granule pneumatic conveying systems are essential in industrial applications where the efficient and safe transport of rubber granules is required. These systems utilize air or gas as the conveying medium to move rubber granules through a pipeline network. The technology offers a reliable alternative to traditional bulk material handling methods, such as belt conveyors or screw conveyors, especially in environments where dust control and contamination prevention are critical.
Working Principle of Rubber Granule Pneumatic Conveying Systems
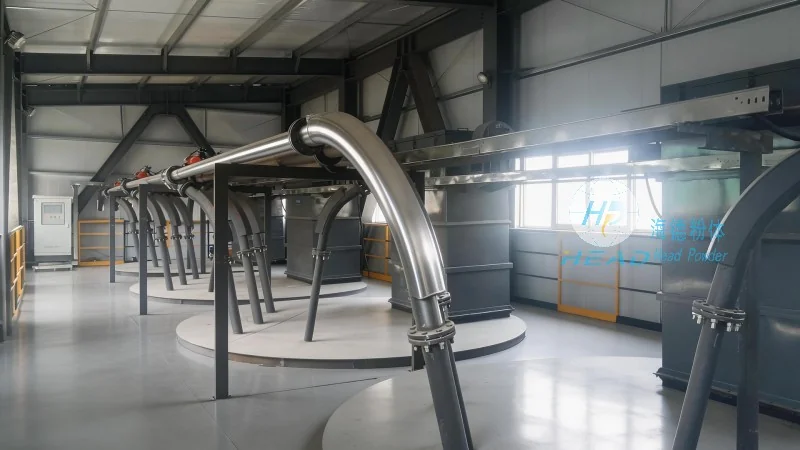
The core working principle of rubber granule pneumatic conveying systems involves the use of a pressure or vacuum source to generate airflow within a pipeline. The system typically consists of several key components, including a feeder, a conveying line, a separator, and a receiver. The process begins with the rubber granules being fed into the system, often through a hopper or a rotary valve. The feeder then introduces the granules into the pipeline, where they are entrained by the high-velocity air stream. As the air flows through the conveying line, it carries the rubber granules to the destination point. At the receiving end, a separator, such as a cyclone or a bag filter, separates the granules from the air stream, allowing the rubber granules to be deposited into a storage bin or processing equipment. The air, now clean, is either recirculated back into the system or discharged to the atmosphere, depending on the system design.
Key Features of Rubber Granule Pneumatic Conveying Systems
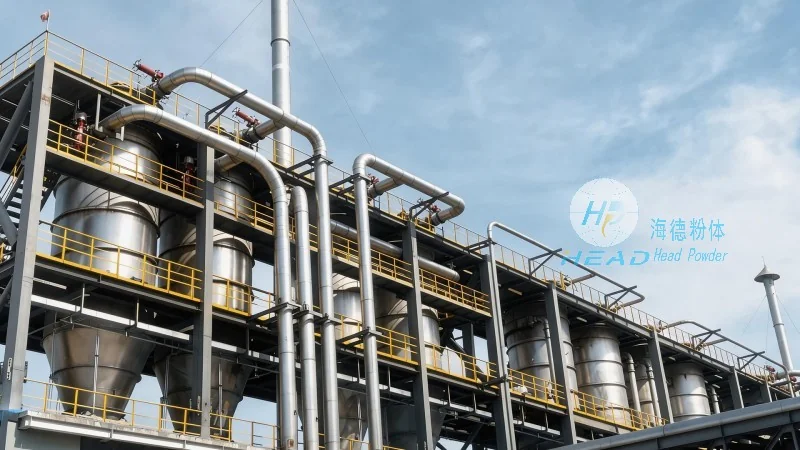
Rubber granule pneumatic conveying systems offer several advantages that make them ideal for industrial applications. One of the primary features is their ability to handle abrasive materials like rubber granules without causing wear and tear on the system components. The systems are designed with durable materials, such as stainless steel or special alloys, to withstand the abrasive nature of rubber granules and ensure long-term operational reliability. Another significant feature is the excellent dust control capability. By using a closed pipeline system, these systems minimize dust emissions, creating a safer working environment and reducing the risk of contamination in downstream processes. Additionally, the systems provide high conveying efficiency, allowing for the transport of rubber granules over long distances with minimal energy consumption. The flexibility of the system design enables it to be adapted to various industrial settings, accommodating different material flow rates and process requirements. Furthermore, the systems are equipped with advanced control systems that allow for precise regulation of the conveying process, ensuring consistent material flow and preventing overloading or underloading of the system.
Applications and Benefits in Industrial Settings
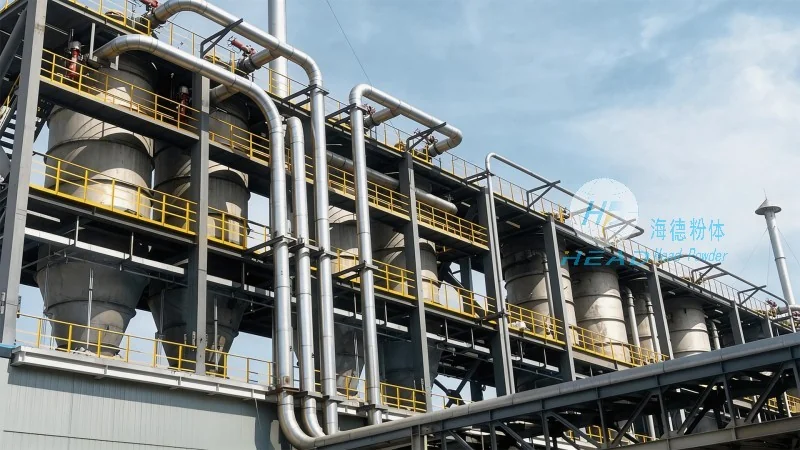
Rubber granule pneumatic conveying systems are widely used in various industries, including the rubber manufacturing, recycling, and processing sectors. In rubber manufacturing, these systems efficiently transport raw rubber granules from storage to processing equipment, such as mixers and extruders. In rubber recycling, they help in moving recycled rubber granules from sorting and cleaning processes to storage or further processing stages. The benefits of using pneumatic conveying systems in these applications include improved productivity, reduced labor costs, and enhanced safety. The systems also contribute to better material quality control by minimizing the risk of contamination and ensuring consistent material handling. Moreover, the systems are designed to be compact and space-efficient, making them suitable for installations in limited spaces within industrial facilities. The low maintenance requirements and long service life of these systems further enhance their economic viability for industrial operations.
Conclusion and Company Information
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted manufacturer and supplier of rubber granule pneumatic conveying systems. With years of experience in the industry, the company specializes in designing and manufacturing high-quality pneumatic conveying solutions tailored to the specific needs of its clients. The company's systems are known for their reliability, efficiency, and durability, making them a preferred choice for industrial applications. By leveraging advanced technology and rigorous quality control processes, HeadPowder ensures that its rubber granule pneumatic conveying systems meet the highest standards of performance and safety. For businesses seeking efficient and reliable rubber granule handling solutions, HeadPowder offers comprehensive services, including system design, installation, and maintenance, to support their operational needs. With a commitment to excellence and customer satisfaction, HeadPowder continues to be a leading provider in the pneumatic conveying industry.