With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Maltose material handling systems are critical components in industrial processes, particularly in the food and beverage sector where efficient and reliable transportation of maltose is essential. These systems are designed to handle the unique properties of maltose, ensuring safe and efficient movement from storage to processing units. Understanding the working principle and key features of such systems is vital for optimizing operational efficiency and maintaining product quality.
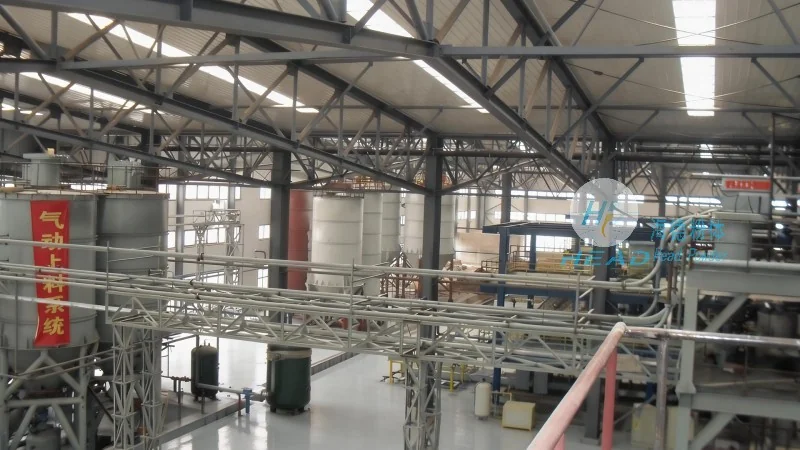
The core working principle of a maltose material handling system revolves around the integration of various components that work in tandem to transport maltose. Typically, these systems start with a storage silo or hopper where maltose is stored in bulk. From there, the material is transferred to a conveyor system, which may include screw conveyors, belt conveyors, or pneumatic conveyors, depending on the specific requirements of the application. The system often incorporates control mechanisms that regulate the flow rate and direction of the maltose, ensuring precise and controlled movement. Additionally, the design may include features such as level sensors and flow meters to monitor the material level and flow rate in real-time, providing data for process optimization and maintenance planning.
HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, offers maltose material handling systems with several distinctive features that enhance performance and reliability. One of the primary features is the robust construction, which is designed to withstand the abrasive nature of maltose and the operational stresses involved in material handling. The systems are equipped with high-quality materials, such as stainless steel, to prevent contamination and ensure hygiene compliance, which is crucial in food processing applications. Another key feature is the advanced control technology, including programmable logic controllers (PLCs) and user-friendly interfaces, that allow for precise control over the entire system. This technology enables operators to adjust parameters such as speed, flow rate, and direction with ease, improving operational flexibility and reducing downtime. Furthermore, the systems are designed with safety features, such as emergency stop buttons and overload protection, to ensure the safety of personnel and equipment. The integration of sensors and monitoring systems provides real-time data on system performance, enabling proactive maintenance and reducing the risk of unexpected failures.
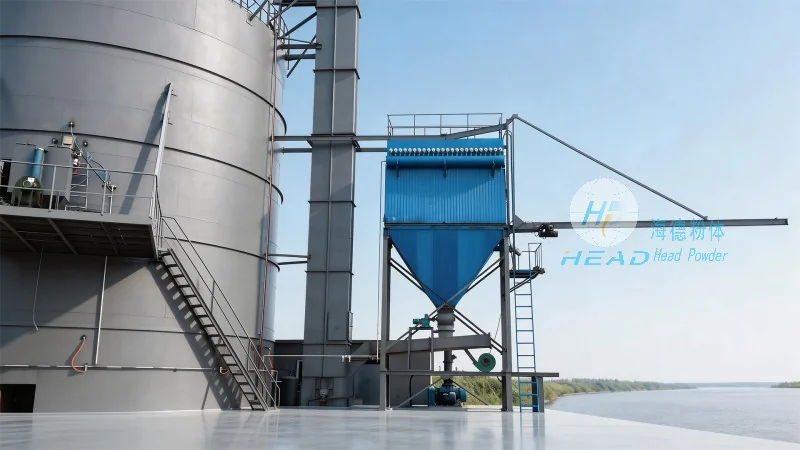
Implementing a maltose material handling system from HeadPowder Engineering Co., Ltd. offers numerous benefits for industrial operations. The primary benefit is the significant improvement in operational efficiency, as the system automates the material handling process, reducing the need for manual labor and minimizing the risk of human error. This leads to increased productivity and reduced labor costs. Additionally, the systems enhance product quality by ensuring consistent and controlled movement of maltose, which helps maintain the integrity of the product and reduces the risk of contamination. The advanced control features also contribute to energy efficiency, as the system can optimize energy consumption based on the actual demand. Furthermore, the robust construction and reliable performance of the systems result in lower maintenance costs and longer service life, providing a better return on investment for the users.
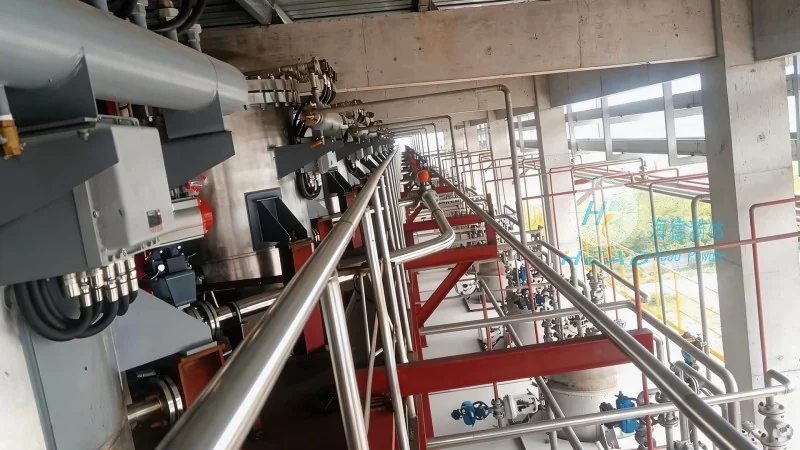
HeadPowder Engineering Co., Ltd. understands that different industrial applications have unique requirements, and therefore, offers customized maltose material handling systems to meet specific needs. The company's engineering team works closely with clients to understand their operational challenges and design solutions that address those challenges effectively. The systems can be tailored in terms of capacity, speed, and control features to suit the specific requirements of the application. For example, in a large-scale maltose production facility, a system with high-capacity screw conveyors and advanced monitoring systems may be preferred, while a smaller system with a belt conveyor and basic controls may be suitable for a smaller operation. The flexibility in design also allows for integration with existing infrastructure, reducing the need for major modifications and minimizing downtime during installation.
HeadPowder Engineering Co., Ltd. provides comprehensive maintenance and support services to ensure the long-term performance and reliability of its maltose material handling systems. The company offers regular maintenance services, including routine inspections, cleaning, and part replacements, to prevent potential issues before they become major problems. The maintenance team is trained to handle the unique requirements of maltose handling systems, ensuring that all components are properly maintained and functioning optimally. Additionally, the company provides technical support and troubleshooting services to assist clients in resolving any issues that may arise during operation. The support team is available 24/7 to provide assistance, ensuring minimal disruption to the production process. The comprehensive maintenance and support services offered by HeadPowder Engineering Co., Ltd. help clients to maximize the lifespan of their equipment and minimize downtime, leading to improved operational efficiency and reduced costs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top