

Working Principle and Features of Grain Granular Material Conveying Systems
Grain granular material conveying systems are essential in the agricultural and food processing industries, designed to efficiently transport bulk materials such as grains, seeds, and other granular products. These systems play a crucial role in optimizing workflow, enhancing productivity, and ensuring the safe handling of delicate or heavy materials. Understanding the working principle and key features of such systems is vital for selecting the right equipment for specific applications.
Working Principle of Grain Granular Material Conveying Systems
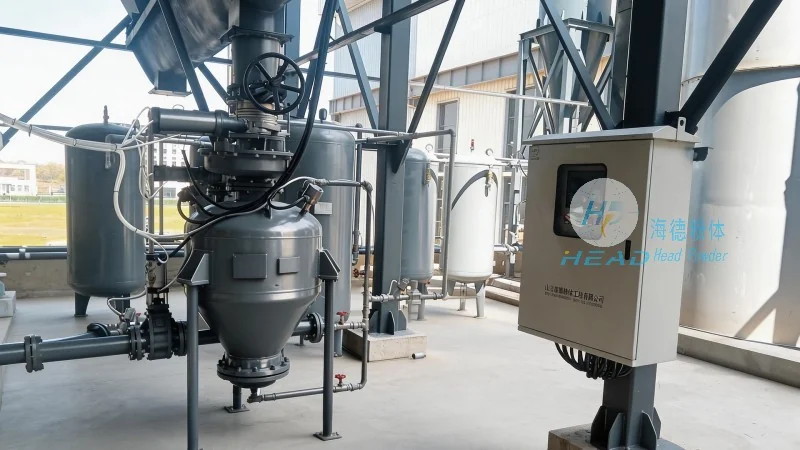
The core working principle of grain granular material conveying systems revolves around the use of mechanical components to move bulk materials from one location to another. Typically, these systems employ a combination of mechanisms like screw conveyors, belt conveyors, or pneumatic conveyors, each tailored to handle different types of granular materials and operational requirements. The process generally involves the following steps:
First, the material is fed into the system, often through a hopper or inlet. The conveying mechanism then moves the material along a designated path, using either gravity, mechanical force, or air pressure to propel the granules. For example, in a screw conveyor, a rotating screw (or auger) pushes the material forward, while in a belt conveyor, a moving belt transports the material by friction. Pneumatic conveyors utilize air pressure to create a flow of material through a pipeline, which is particularly effective for fine or dusty granular products.
During the conveying process, the system maintains consistent material flow rates and prevents blockages or overloading. Sensors and control systems are often integrated to monitor the material level, speed, and pressure, ensuring smooth operation and preventing damage to the equipment or the material. This automated control enhances efficiency and reduces the need for manual intervention, making the system suitable for continuous production environments.
Key Features of Grain Granular Material Conveying Systems
Grain granular material conveying systems are characterized by several key features that make them ideal for industrial applications. These features include:
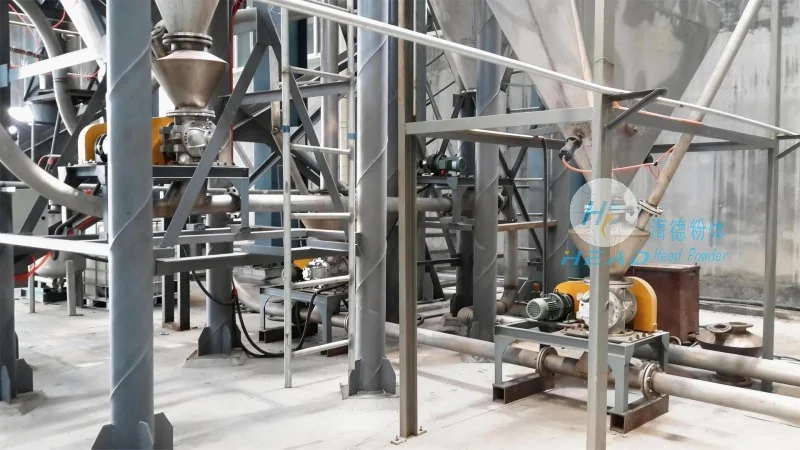
1. **High Efficiency and Capacity**: Modern conveying systems are engineered to handle large volumes of material with minimal energy consumption. The design of the conveying mechanism, such as the pitch and speed of a screw or the belt speed in a belt conveyor, is optimized to maximize throughput while maintaining low operational costs.
2. **Versatility in Material Handling**: These systems are adaptable to a wide range of granular materials, including different types of grains, seeds, and even processed food products. The ability to handle various materials without significant modifications makes them a versatile choice for diverse industrial needs.
3. **Low Maintenance and Durability**: Constructed with robust materials like stainless steel or heavy-duty plastics, these systems are designed to withstand the rigors of continuous operation. The use of wear-resistant components and regular maintenance protocols ensures long service life and reduces downtime.
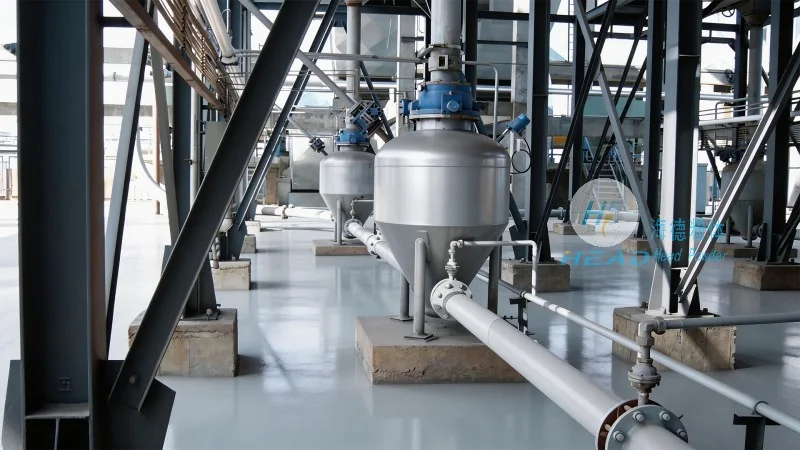
4. **Safety and Hygiene Compliance**: For applications involving food-grade materials, conveying systems are often designed with food-safe components, smooth surfaces, and easy-to-clean features. This compliance with hygiene standards is crucial for maintaining product quality and meeting regulatory requirements.
5. **Customization and Scalability**: Many manufacturers offer customized solutions to meet specific operational needs, including varying conveyor lengths, widths, and material handling capacities. This scalability allows businesses to expand their operations or adapt to changing production demands without replacing the entire system.
Applications and Benefits in Industrial Settings
Grain granular material conveying systems are widely used in various industries, including agriculture, food processing, and chemical manufacturing. In the agricultural sector, they are used for transporting harvested grains from fields to storage facilities or processing plants. In food processing, these systems facilitate the movement of raw materials through production lines, ensuring a smooth flow from raw to finished products.
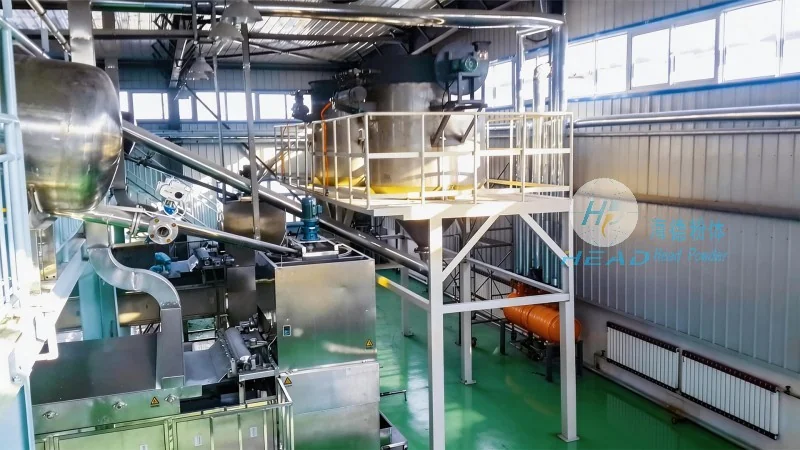
The benefits of implementing such systems extend beyond efficiency. By reducing manual labor and minimizing material handling errors, these systems enhance workplace safety and improve product quality. Additionally, the consistent material flow helps in maintaining production schedules and meeting customer demands in a timely manner.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in designing and manufacturing high-quality grain granular material conveying systems. With a focus on innovation and customer satisfaction, the company provides tailored solutions that meet the unique needs of its clients. HeadPowder's products are known for their reliability, efficiency, and adherence to industry standards, making them a trusted choice for businesses seeking to optimize their material handling processes.
HeadPowder's commitment to quality is reflected in its use of advanced manufacturing techniques and rigorous quality control measures. The company's team of experienced engineers and technicians work closely with clients to understand their operational requirements and develop customized conveying systems that deliver optimal performance. Whether for small-scale operations or large industrial facilities, HeadPowder offers solutions that enhance productivity and ensure the safe handling of granular materials.
Located in Shandong, China, HeadPowder leverages its local expertise and resources to deliver superior products and services. The company's dedication to research and development ensures that its conveying systems incorporate the latest technological advancements, providing clients with cutting-edge solutions that meet evolving industry demands.