

Principle and Working Scene Characteristics of Capsule Material Pneumatic Conveying Equipment
Efficient and reliable material handling is a critical factor in various industrial processes, particularly when dealing with sensitive or specialized products like capsule materials. Pneumatic conveying equipment has emerged as a sophisticated solution for transporting such materials with precision and minimal contamination. This article delves into the fundamental principles behind capsule material pneumatic conveying systems and explores the distinct characteristics of their operational environments.
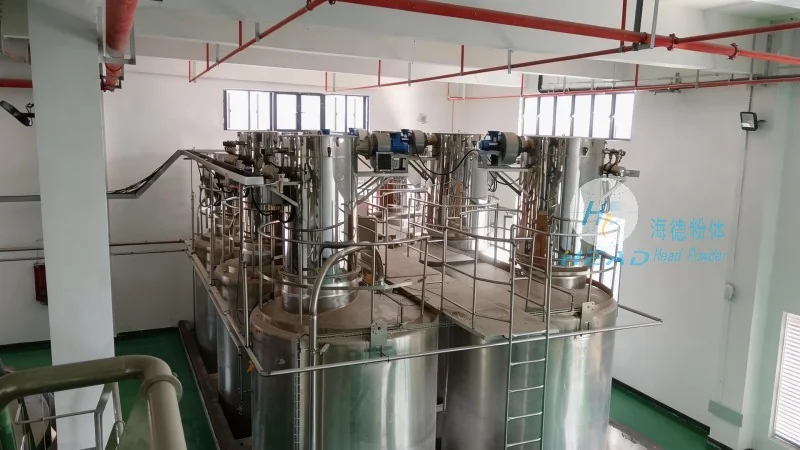
Understanding the Core Principle of Pneumatic Conveying
The fundamental principle of pneumatic conveying involves the use of air or gas to transport bulk materials through a pipeline system. In the context of capsule materials, which often require sterile and controlled environments, the design of these systems must prioritize hygiene, efficiency, and product integrity. The process typically operates under either positive pressure (where air is forced through the system) or negative pressure (where air is drawn out, creating a vacuum). For capsule materials, positive pressure systems are commonly preferred as they minimize the risk of contamination and ensure consistent flow rates. The equipment includes components such as a hopper, feeder, conveyor line, and a receiver, all working in tandem to move the capsules from the source to the destination. The air velocity and pressure within the system are carefully calibrated to prevent material degradation or damage, ensuring that the capsules retain their shape and quality throughout the conveying process.
Key Working Scene Characteristics of Capsule Material Pneumatic Conveying
The operational environments for capsule material pneumatic conveying systems exhibit several unique characteristics that set them apart from traditional bulk material handling. Firstly, the systems are often integrated into cleanroom environments, particularly in pharmaceutical and food industries, where maintaining sterility is paramount. This necessitates the use of stainless steel components, air filtration systems, and sealed connections to prevent any cross-contamination. Secondly, the equipment is designed to handle a wide range of capsule sizes and shapes, from small, hard capsules to larger, soft gelatin capsules, ensuring versatility across different production lines. Thirdly, the systems are typically equipped with advanced control mechanisms that allow for real-time monitoring of flow rates, pressure, and air quality, enabling operators to adjust parameters dynamically and maintain optimal performance. Additionally, the conveying process is often synchronized with downstream packaging or processing equipment, creating a seamless production line that enhances overall efficiency and reduces downtime.
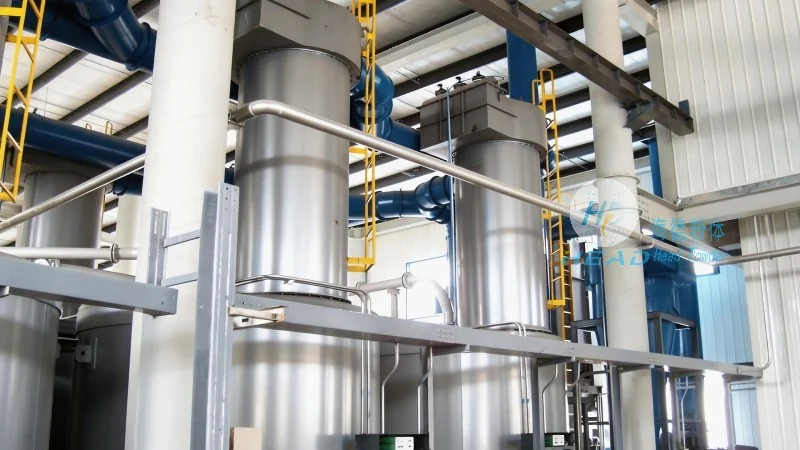
Application Scenarios in Pharmaceutical and Food Industries
One of the primary applications of capsule material pneumatic conveying systems is in the pharmaceutical industry, where the transportation of active pharmaceutical ingredients (APIs) and finished capsules requires stringent quality control. These systems are commonly used in the manufacturing of oral solid dosage forms, where capsules are filled with powders or granules and then sealed. The pneumatic conveying equipment ensures that the capsules are moved from the filling station to the packaging line without any exposure to external contaminants, maintaining the product's efficacy and safety. In the food industry, similar principles are applied when handling food-grade capsules, such as those used for dietary supplements or flavorings. The systems are designed to meet food safety regulations, with components that are easy to clean and sanitize, and air filtration systems that prevent the entry of dust or microorganisms. Moreover, the ability to handle different capsule types, including soft gelatin and hard gelatin, makes these systems adaptable to various food product lines.
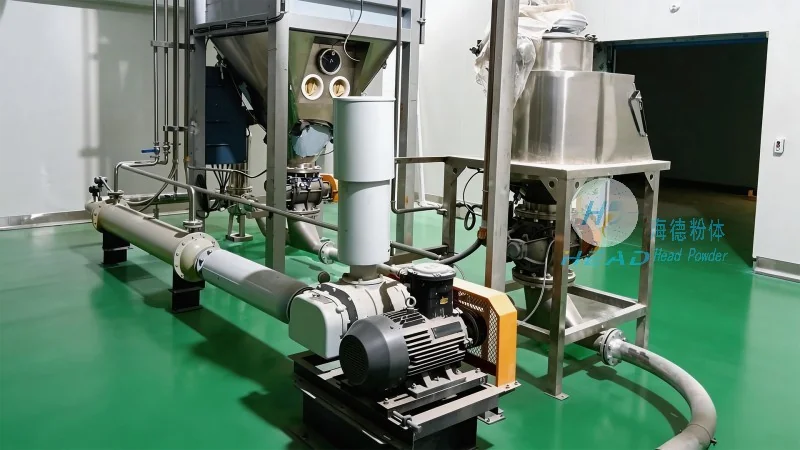
Advantages and Considerations for Operational Efficiency
Implementing capsule material pneumatic conveying systems offers several advantages that contribute to improved operational efficiency. One of the key benefits is the reduction in manual handling, which minimizes the risk of product damage and human error. The automated nature of the system allows for consistent and repeatable performance, ensuring that the capsules are transported at a uniform speed and without interruptions. Another advantage is the space-saving design, as the equipment can be installed in compact areas, making it suitable for facilities with limited floor space. However, there are also considerations to keep in mind, such as the need for regular maintenance to ensure the air filtration systems and conveyor components remain in optimal condition. Additionally, the initial investment cost of these systems may be higher compared to traditional methods, but the long-term benefits, including reduced labor costs and improved product quality, often outweigh the initial expenses.
About HeadPowder: A Leader in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a prominent manufacturer specializing in the design and production of pneumatic conveying equipment for various industries. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted partner for companies seeking reliable solutions for material handling. The company's expertise lies in customizing systems to meet the specific needs of clients, ensuring that the equipment is tailored to the type of capsule material, production volume, and operational environment. HeadPowder's commitment to using high-quality materials and advanced technology ensures that their products deliver consistent performance and durability. The company's headquarters is located in Shandong, China, where they have a dedicated team of engineers and technicians who work closely with clients to develop and implement effective pneumatic conveying solutions. By prioritizing customer satisfaction and product excellence, HeadPowder continues to be a leading provider in the field of capsule material handling.