With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading manufacturer in the field of bulk material handling solutions, specializes in providing advanced air-driven conveying systems tailored for the precise mixing and transportation of formulation ingredients. With a strong presence in Shandong, China, the company has established itself as a trusted partner for industries requiring efficient and reliable material processing technologies.
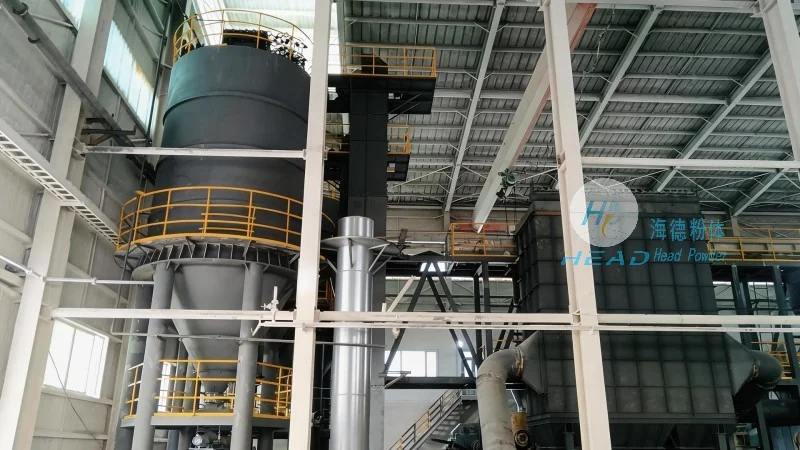
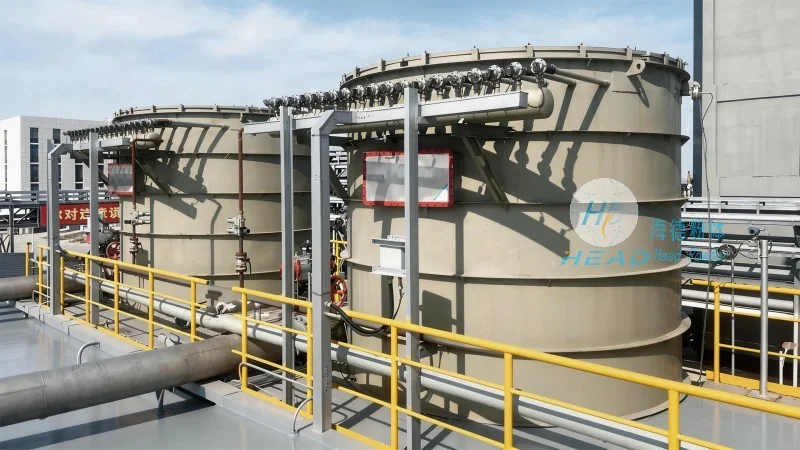
The fundamental principle behind air-driven conveying lines lies in the use of pressurized or vacuum air to transport bulk materials through a network of pipes. This method eliminates the need for mechanical components like belts or chains, reducing maintenance requirements and enhancing operational safety. The system typically operates by creating a pressure differential that propels the material forward, ensuring a consistent and controlled flow. For formulation applications, this technology is particularly advantageous as it maintains the integrity of sensitive ingredients, preventing contamination and degradation during transport. The air-driven mechanism also allows for flexible system design, enabling the integration of multiple mixing and conveying stages within a single, compact setup.
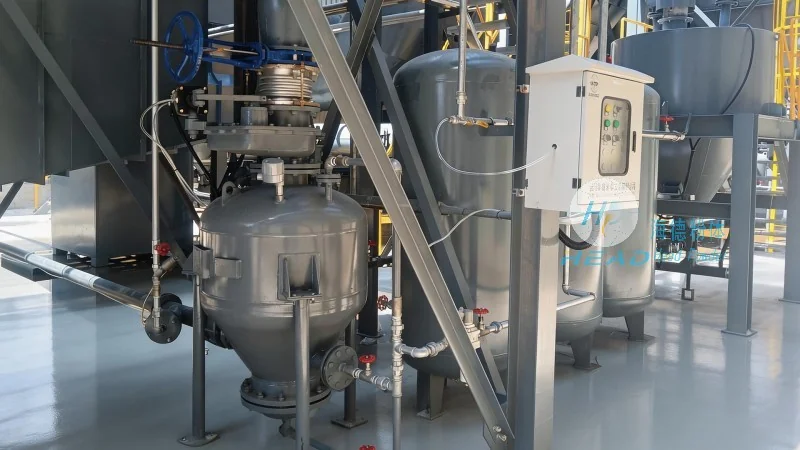
When evaluating the working scene characteristics of these systems, several critical factors come into play. Firstly, the system's ability to handle diverse material types is a defining feature. Whether dealing with powders, granules, or even fine particles, the air-driven design accommodates a wide range of bulk materials commonly used in formulation processes. This versatility is crucial for industries such as pharmaceuticals, food processing, and chemical manufacturing, where material consistency and purity are paramount. Secondly, the system's scalability is noteworthy. From small-scale laboratory applications to large industrial production lines, the conveying lines can be customized to meet varying throughput requirements. This adaptability ensures that the system can grow with the client's production needs, providing long-term value. Additionally, the system's energy efficiency stands out. By utilizing compressed air as the primary driving force, the operation consumes less energy compared to traditional mechanical conveying methods, contributing to lower operational costs and reduced environmental impact. The quiet operation of air-driven systems is another advantage, minimizing noise pollution in industrial environments and enhancing workplace safety.
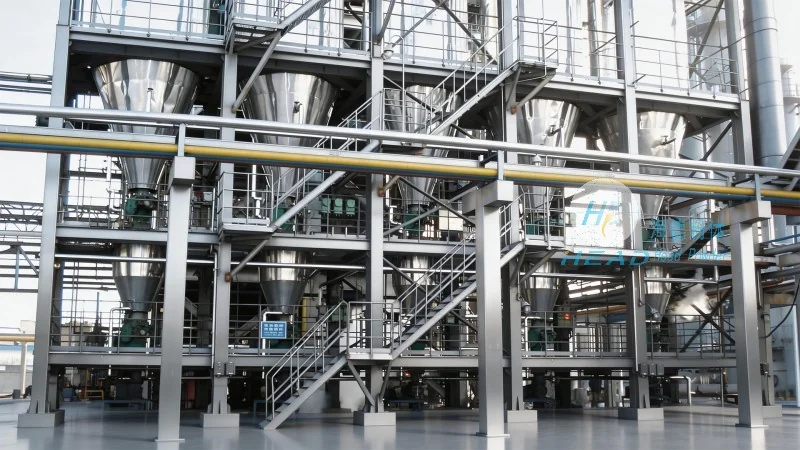
The practical application of bulk material mixing and air-driven conveying lines spans across multiple industries, each benefiting from the system's unique capabilities. In the pharmaceutical sector, for instance, the system is used to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the final product meets stringent quality standards. The enclosed design of the conveying lines prevents cross-contamination, a critical requirement in pharmaceutical manufacturing. Similarly, in the food industry, the system handles ingredients like flour, sugar, and spices, maintaining their freshness and preventing moisture absorption. The gentle handling of materials by the air flow minimizes product degradation, preserving the quality and taste of the final food products. In chemical manufacturing, the system is employed to transport raw materials and intermediates, supporting continuous production processes. The ability to integrate mixing and conveying stages in a single system streamlines the production workflow, reducing processing time and improving overall efficiency. Furthermore, the system's modular design allows for easy integration with existing production lines, minimizing downtime during installation and setup. This flexibility is particularly valuable for companies undergoing expansion or modernization of their facilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top