

Working Principle and Features of Phosphate Calcium Pneumatic Conveying Equipment
Phosphate calcium pneumatic conveying equipment is a specialized device designed for the efficient transport of phosphate calcium materials in industrial settings. This equipment operates by utilizing air pressure to move bulk materials through a pipeline system, eliminating the need for traditional mechanical conveyors like belts or buckets. The working principle centers on the creation of a low-pressure zone within the conveying line, which draws the material into the air stream and propels it to the destination. This process is highly effective for handling powders and granules, ensuring minimal material degradation and loss during transport.
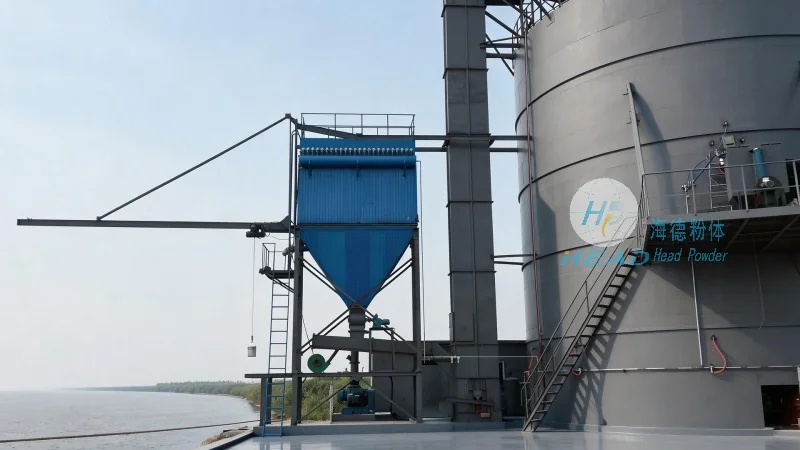
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of such advanced pneumatic conveying systems. The company's expertise lies in customizing equipment to meet specific operational requirements, including varying material characteristics, distance, and throughput needs. By leveraging state-of-the-art technology, HeadPowder ensures that their phosphate calcium pneumatic conveyors deliver reliable performance and durability in demanding industrial environments.
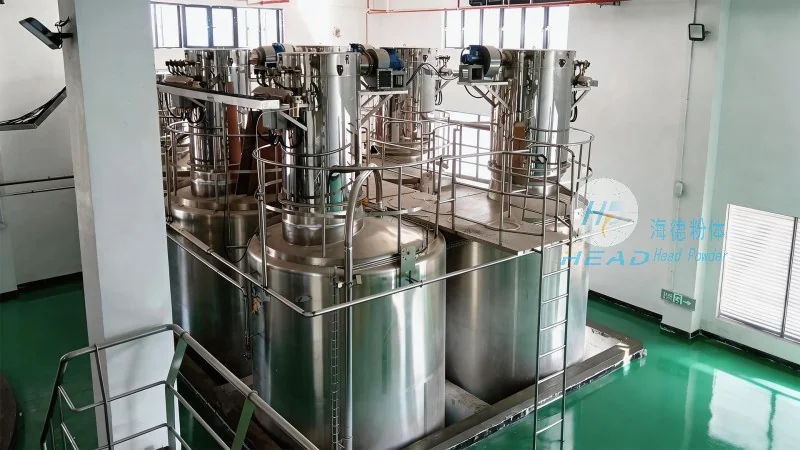
Key features of the phosphate calcium pneumatic conveying equipment include high efficiency in material transport, reduced maintenance compared to traditional systems, and the ability to handle a wide range of particle sizes and moisture content. The equipment is also designed with safety in mind, incorporating features such as air filtration and pressure relief mechanisms to prevent accidents and ensure compliance with industrial safety standards. Additionally, the system's modular design allows for easy integration into existing production lines, minimizing downtime during installation and operation.
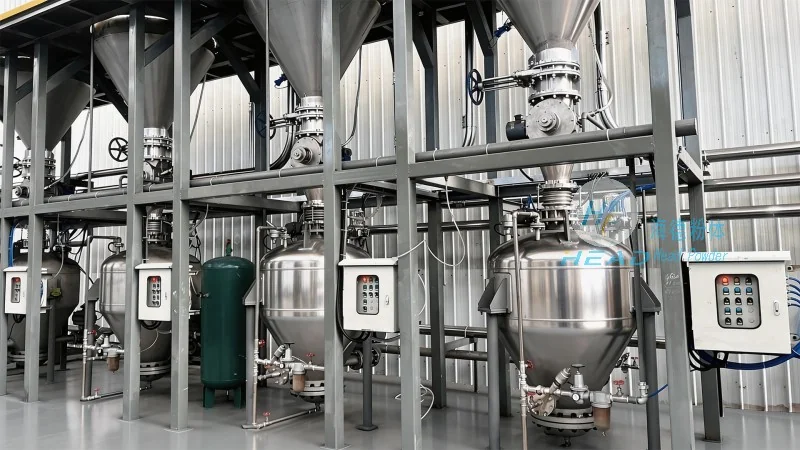
Another notable characteristic is the equipment's ability to handle abrasive materials without significant wear on components. This is achieved through the use of high-quality materials for the conveying line and appropriate air flow management, which reduces friction and extends the lifespan of the system. The pneumatic conveying process also offers advantages in terms of hygiene, as it prevents cross-contamination and maintains the purity of the phosphate calcium product, which is crucial for applications in food and pharmaceutical industries.
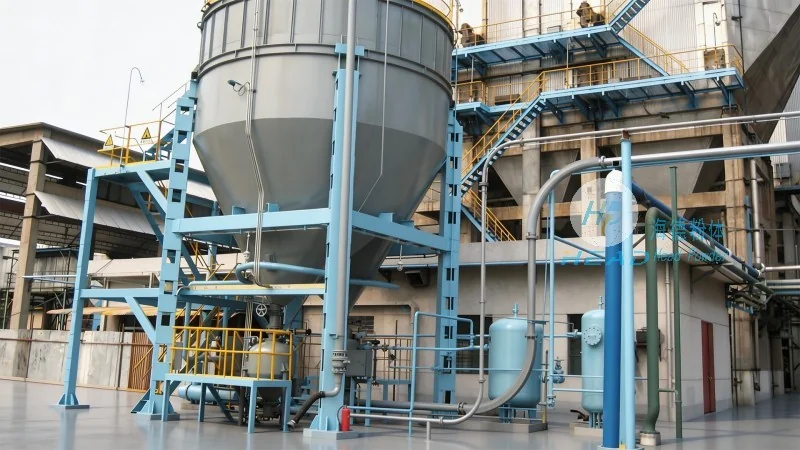
HeadPowder's commitment to quality and innovation is reflected in the robust construction and performance of their phosphate calcium pneumatic conveying equipment. The company's products are engineered to withstand the rigors of continuous operation, ensuring consistent and reliable material transport. By focusing on customer needs and industry standards, HeadPowder provides solutions that enhance operational efficiency and reduce costs for clients in various sectors, including chemical processing, mining, and food processing.