With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading enterprise in the field of pneumatic conveying technology, specializes in the design, manufacturing, and installation of advanced systems for transporting purified ash. This article provides a comprehensive overview of the purified ash pneumatic conveying system, detailing its structural components and operational principles to help clients understand its functionality and benefits. Based in Shandong, China, HeadPowder leverages decades of industry experience to deliver high-quality solutions tailored to the needs of industrial clients.
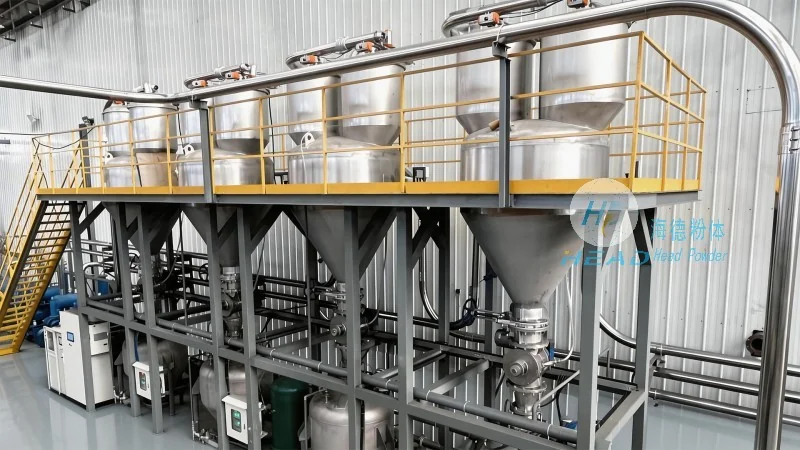
At Shandong HeadPowder Engineering Co., Ltd., our purified ash pneumatic conveying system is engineered to efficiently handle ash from various industrial processes, such as power generation and cement production. The system is designed to ensure minimal dust emission and optimal material transport, aligning with environmental standards and operational efficiency. By leveraging advanced pneumatic conveying technology, this system offers a reliable solution for ash handling, reducing labor costs and improving overall process safety. The system is particularly suitable for facilities seeking to enhance their environmental performance while maintaining operational productivity.
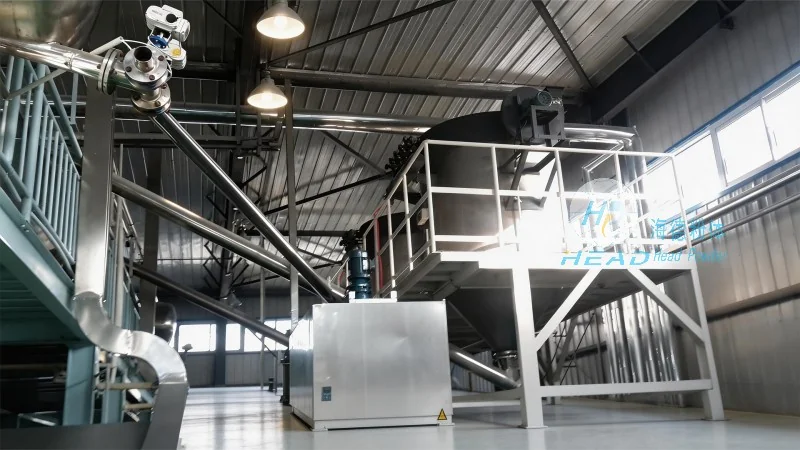
The purified ash pneumatic conveying system consists of several critical components that work in harmony to achieve effective material transport. These components include the ash collection hopper, the air compressor, the conveying pipeline, and the dust filtration system. Each component is meticulously designed to withstand the demands of ash handling, with robust materials and precise engineering to minimize wear and tear. The ash collection hopper is equipped with a feed mechanism that ensures consistent material flow, while the air compressor is selected based on the required pressure and flow rate to match the system's capacity. The conveying pipeline is typically made of corrosion-resistant materials, such as stainless steel or polyethylene, to prevent ash buildup and ensure long-term durability. The dust filtration system, often incorporating bag filters or cartridge filters, captures fine ash particles and returns clean air to the environment, meeting regulatory requirements for air quality.
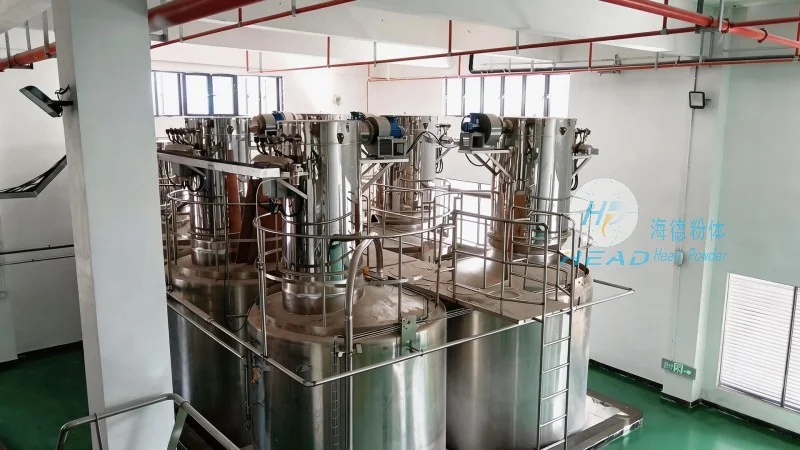
The operation of the purified ash pneumatic conveying system is based on the principle of air flow to move material through a pipeline. The process begins with the ash being fed into the collection hopper, where it is then mixed with compressed air from the air compressor. The air and ash mixture is then introduced into the conveying pipeline, where the air pressure propels the ash forward. The system uses a combination of positive and negative pressure zones to control the flow of material, ensuring consistent and efficient transport. The positive pressure zone is created near the air compressor, where the air is pressurized and mixed with ash, while the negative pressure zone is established at the discharge end, where the air is drawn to create suction and help move the material. This two-stage approach ensures that the material is transported smoothly without blockages or uneven flow. The system also includes a control panel that monitors pressure, flow rate, and other parameters, allowing for real-time adjustments to maintain optimal performance.
Implementing the purified ash pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. offers numerous advantages for industrial facilities. The system reduces the need for manual handling of ash, minimizing the risk of dust exposure and improving workplace safety. Additionally, the automated process enhances operational efficiency, allowing for continuous material transport without interruptions. The system also contributes to environmental sustainability by reducing dust emissions and improving air quality. Furthermore, the modular design of the system allows for easy integration into existing industrial setups, providing flexibility and scalability for various applications. Clients can benefit from reduced maintenance costs due to the system's durable components and low maintenance requirements. The system's energy efficiency is another key advantage, as it optimizes air usage and reduces operational expenses over time.
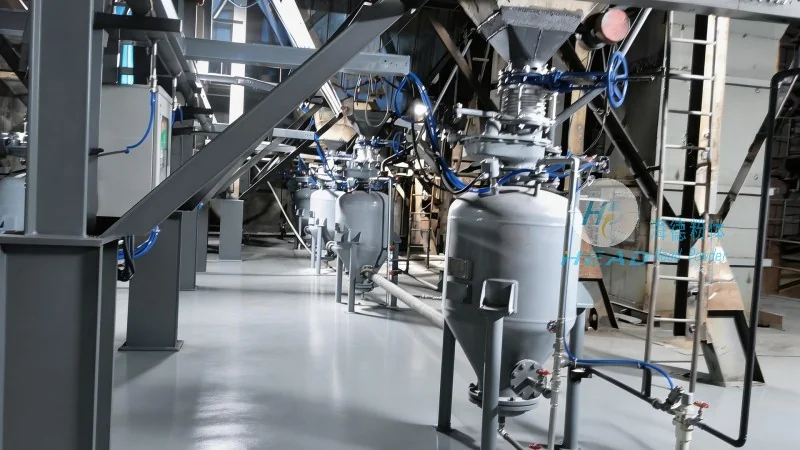
The purified ash pneumatic conveying system is suitable for a wide range of applications, including power plants, cement factories, and waste management facilities. The system can be customized to meet specific client requirements, such as varying ash types, transport distances, and environmental standards. Shandong HeadPowder Engineering Co., Ltd. works closely with clients to understand their unique needs and develop tailored solutions that optimize performance and cost-effectiveness. Whether for new installations or upgrades to existing systems, the purified ash pneumatic conveying system provides a reliable and efficient solution for ash handling. For example, in power plants, the system can transport fly ash from boilers to storage silos, while in cement factories, it can handle raw material ash for clinker production. The system's adaptability makes it a versatile choice for various industrial processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top