With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for the fine chemicals industry. This article provides an overview of the core components, operational principles, and key advantages of such systems, highlighting how they enhance efficiency and safety in material handling processes.
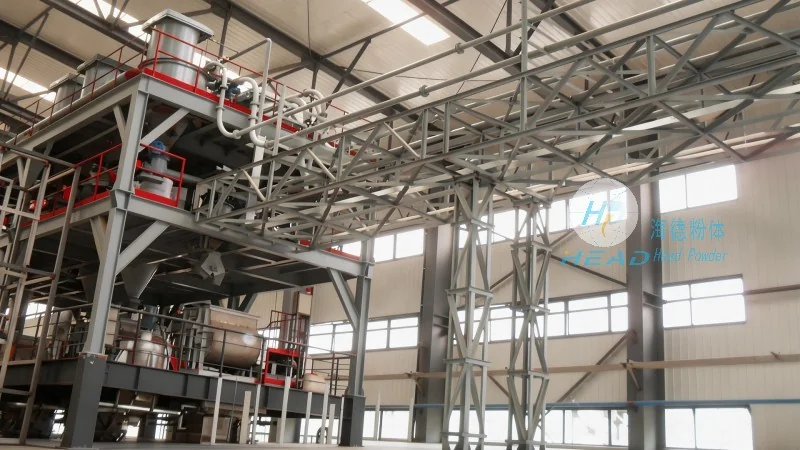
The pneumatic conveying system for fine chemicals typically consists of several critical components that work in tandem to transport powders and granules. These include the material feed hopper, which holds the bulk material and ensures a consistent feed rate; the air compressor or blower, which generates the necessary air pressure to move the material; the conveying line, which can be either positive or negative pressure depending on the application; and the receiving hopper or silo, where the material is deposited. Additionally, control valves, filters, and dust collection systems are integral to maintaining system performance and safety.
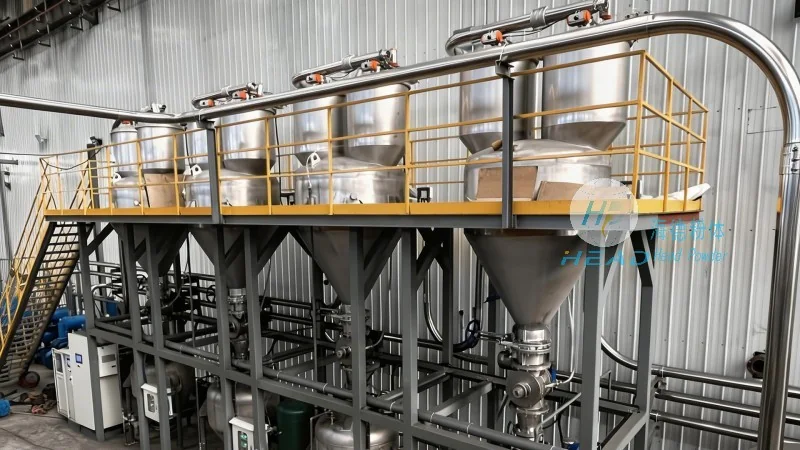
The operation of a pneumatic conveying system involves the introduction of air into the conveying line, which creates a flow that entrains the solid particles. In positive pressure systems, air is forced through the line, carrying the material from the feed point to the discharge point. Negative pressure systems, on the other hand, use suction to draw material from the source into the line. The choice between positive and negative pressure depends on factors such as the material's properties, the distance to be conveyed, and the need for containment. The system's efficiency is optimized by controlling the air flow rate, pressure, and particle size distribution, ensuring minimal material degradation and maximum throughput.
For the fine chemicals industry, pneumatic conveying systems offer several distinct advantages over traditional mechanical methods. These include improved product integrity, as the system minimizes contact with external contaminants and reduces the risk of material degradation due to friction or exposure to air. Additionally, the systems are highly flexible, allowing for easy integration into existing production lines and the ability to handle a wide range of material types, from fine powders to bulk granules. Safety is another critical benefit, as the enclosed system prevents dust emissions and reduces the risk of fire or explosion, which are common concerns with open handling methods. Furthermore, the systems can be designed to operate in a cleanroom environment, making them suitable for pharmaceutical and high-purity applications.
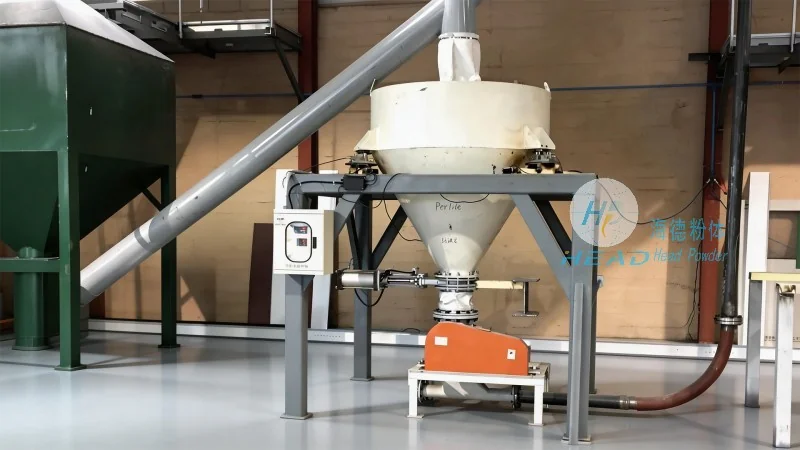
Shandong HeadPowder Engineering Co., Ltd. is a reputable company dedicated to providing innovative solutions for material handling in the fine chemicals sector. With a focus on quality and customer satisfaction, HeadPowder designs and manufactures customized pneumatic conveying systems that meet the specific needs of each client. The company's expertise in engineering and material science ensures that its systems are efficient, reliable, and compliant with industry standards, making them a trusted partner for businesses seeking to enhance their material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top