With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial applications involving sulfur pellets, efficient and reliable material handling is crucial. Pneumatic conveying systems offer a solution that minimizes dust, enhances safety, and optimizes process flow. This article provides an introduction to the structure and operational principles of sulfur pellet pneumatic conveying systems, highlighting key components and their functions.
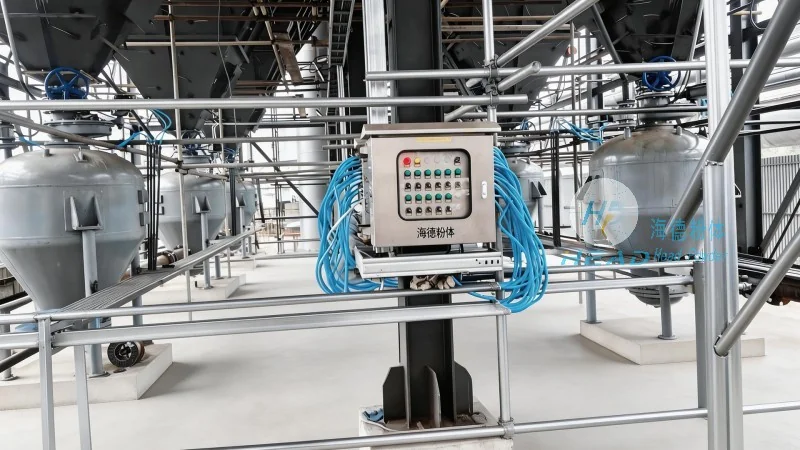
Pneumatic conveying systems transport bulk materials like sulfur pellets through a pipeline using air or gas as the conveying medium. Unlike mechanical systems that rely on belts or screws, pneumatic conveyors utilize pressure differentials to move material. This method is particularly advantageous for sulfur pellets due to their dusty nature and the need for controlled handling to prevent environmental contamination and ensure worker safety.
The core structure of a sulfur pellet pneumatic conveying system consists of several essential components, each playing a vital role in the overall operation. These components include the material feed hopper, the air compressor or blower, the conveying pipeline, the control valves, and the discharge or collection equipment. Each component is designed to work in harmony to ensure efficient and safe material transport.
The material feed hopper is the initial component where sulfur pellets are stored and prepared for transport. It is typically equipped with a feeder mechanism, such as a rotary valve or a screw feeder, which regulates the flow of pellets into the conveying pipeline. The feeder ensures a consistent and controlled feed rate, preventing overloading or underloading of the system. This control is critical for maintaining stable pressure and flow within the pneumatic system.
The air compressor or blower is the power source of the pneumatic conveying system. It generates the necessary air pressure to move the sulfur pellets through the pipeline. The choice of compressor type depends on factors such as the system's capacity, the distance of transport, and the desired conveying velocity. For sulfur pellet applications, positive displacement blowers are commonly used due to their ability to handle high volumes of air and maintain consistent pressure, even with varying material loads.
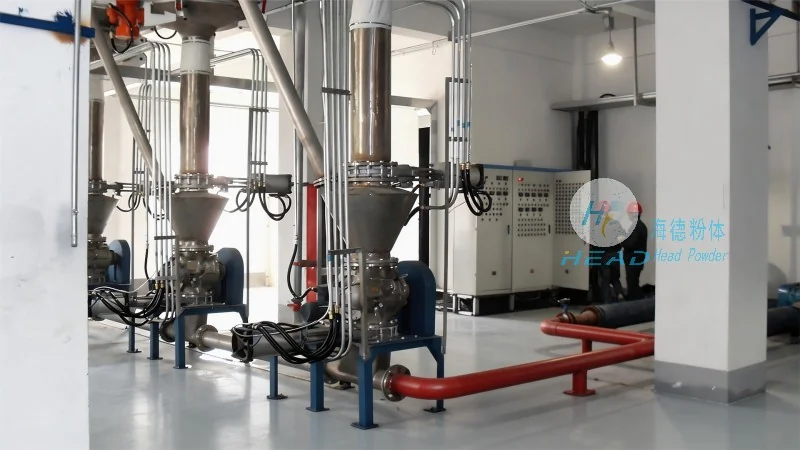
The conveying pipeline is the main channel through which sulfur pellets are transported. It is typically made of materials like stainless steel or PVC to withstand the corrosive nature of sulfur and prevent material buildup. The pipeline layout is carefully designed to minimize pressure losses and ensure smooth material flow. This includes considerations such as pipe diameter, bends, and vertical and horizontal runs, all of which impact the system's efficiency and performance.
Control valves are integral to managing the pneumatic conveying process. They regulate the air pressure and flow within the system, allowing for precise control over the material transport rate. These valves can be automated or manually operated, depending on the system's requirements. By adjusting the valve settings, operators can maintain optimal pressure differentials, prevent backflow, and ensure that the conveying system operates within its design parameters.
The discharge or collection equipment is the final component of the pneumatic conveying system, where sulfur pellets are deposited at their destination. This may include silos, storage tanks, or processing equipment. The design of the discharge system is critical to prevent material spillage and ensure a clean, efficient transfer. Some systems may include dust collection and filtration equipment to comply with environmental regulations and maintain a safe working environment.
The operational principle of sulfur pellet pneumatic conveying is based on creating a pressure differential between the feed and discharge points. The air compressor generates high-pressure air that entrains the sulfur pellets, forming a slurry-like mixture known as a "pneumatic stream." This stream travels through the pipeline, with the air providing the necessary momentum to move the material. The efficiency of the system depends on several factors, including the air velocity, the material's density and size, and the system's pressure drop.
Implementing a pneumatic conveying system for sulfur pellets offers several advantages over traditional mechanical handling methods. These include reduced dust generation, improved safety for workers, and the ability to handle materials in a closed system, minimizing environmental impact. Additionally, pneumatic conveyors can transport materials over longer distances and through complex layouts without the need for multiple transfer points, enhancing overall process efficiency.
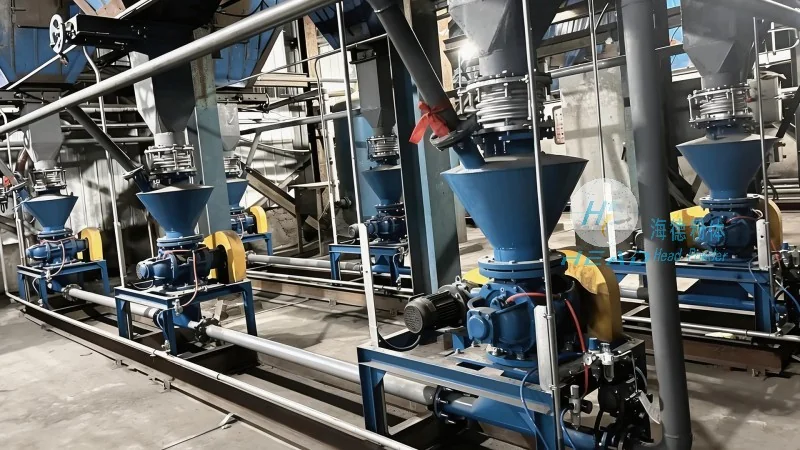
Sulfur pellet pneumatic conveying systems are widely used in various industrial sectors, including chemical manufacturing, fertilizer production, and petrochemical processing. In these applications, the system is used to transport sulfur pellets from storage facilities to processing units, or between different stages of production. The reliability and efficiency of pneumatic conveying make it an ideal solution for handling bulk materials in demanding industrial environments.
To ensure the long-term performance and reliability of sulfur pellet pneumatic conveying systems, regular maintenance is essential. This includes routine checks of the air compressor, pipeline integrity, and control valves. Additionally, proper cleaning and maintenance of the material feed hopper and discharge equipment are crucial to prevent material buildup and ensure smooth operation. Following best practices, such as regular lubrication of moving parts and monitoring of pressure and flow parameters, can extend the system's lifespan and reduce downtime.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of industrial material handling solutions. With a focus on innovation and quality, the company specializes in designing and manufacturing pneumatic conveying systems tailored to the specific needs of its clients. Headpowder's expertise in sulfur pellet handling and other bulk material transport applications has earned it a reputation for delivering reliable, efficient, and cost-effective solutions. The company is committed to providing superior service and support to its customers, ensuring that their material handling systems operate at peak performance.
HeadPowder is located in Shandong, China, and serves clients worldwide with its advanced pneumatic conveying technologies. While specific contact details are not provided here, the company's dedication to quality and customer satisfaction is evident in its comprehensive product offerings and professional service. For more information about sulfur pellet pneumatic conveying systems or other industrial material handling solutions, please visit the company's official website or contact their sales team directly.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top