

[W]Working Principle and Features of Ore Sand Pneumatic Conveying Systems
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, production, and installation of ore sand pneumatic conveying systems. These systems are crucial for efficient material handling in various industrial applications, particularly in the mining and construction sectors. This article explores the working principle and key features of such systems, providing a comprehensive overview for potential users and industry professionals.
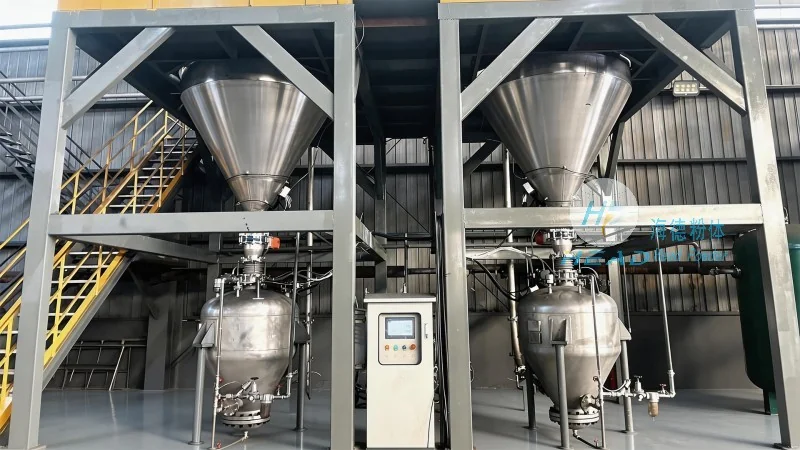
Understanding the Working Principle of Ore Sand Pneumatic Conveying Lines
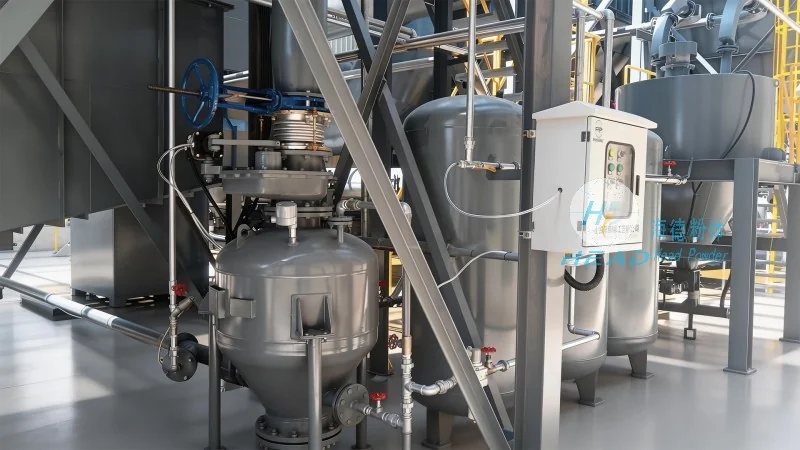
Ore sand pneumatic conveying systems operate on the principle of transporting bulk materials like ore, sand, and other granular substances through a pipeline using air or gas as the conveying medium. The process typically involves several key components, including a hopper for material storage, a feeder to control the flow rate, a blower or compressor to generate the necessary air pressure, and a pipeline network that transports the material to the destination point. The material is introduced into the pipeline either by being entrained in the air stream (in the case of dilute phase systems) or by being pushed through the pipeline with a high-pressure air flow (in the case of dense phase systems).
In a dilute phase system, the material is mixed with the air at a relatively low concentration, allowing it to be carried over long distances with minimal pressure drop. This method is suitable for transporting materials over moderate distances and is commonly used for fine powders and granules. Conversely, dense phase systems involve a higher concentration of material in the air stream, resulting in a higher pressure drop and the ability to transport materials over longer distances with less degradation of the material's quality. The choice between these systems depends on factors such as the material's properties, the required conveying distance, and the desired material handling efficiency.
Key Features of Ore Sand Pneumatic Conveying Systems
HeadPowder's ore sand pneumatic conveying systems are designed with several distinct features that enhance their performance and reliability. One of the primary advantages is the ability to transport materials in a closed system, which helps prevent dust emissions and contamination, ensuring compliance with environmental regulations and maintaining product quality. This is particularly important for ore and sand, which can be abrasive and generate fine particles that may otherwise cause health hazards or equipment wear.
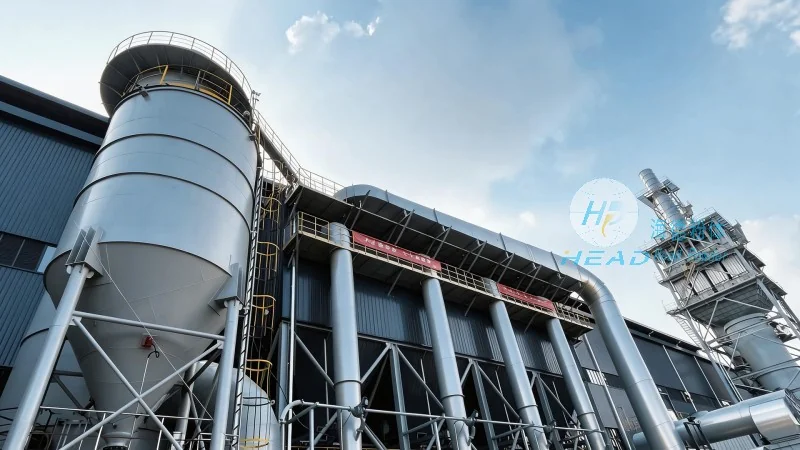
Another notable feature is the flexibility in system design, allowing customization to meet specific operational requirements. Systems can be configured for different conveying capacities, distances, and material types, making them suitable for a wide range of industrial applications. For instance, some systems are equipped with adjustable feeders that allow precise control over the material flow rate, ensuring consistent performance even with varying material characteristics. Additionally, the use of high-quality materials in the construction of the pipeline and components, such as stainless steel or corrosion-resistant alloys, enhances the system's durability and longevity, reducing maintenance costs over time.
The systems also incorporate advanced control and monitoring capabilities, enabling real-time management of the conveying process. This includes sensors to monitor air pressure, material flow rate, and pipeline conditions, which can be integrated with automated control systems to optimize operation and prevent potential issues before they occur. Such features contribute to improved operational efficiency and reduced downtime, making the systems more cost-effective for long-term use.
Applications and Benefits in Industrial Settings
Ore sand pneumatic conveying systems are widely used in various industrial sectors, including mining, construction, and manufacturing. In mining operations, these systems are essential for transporting ore from processing plants to storage facilities or for conveying sand and other materials within the mine site. The ability to handle abrasive and heavy materials efficiently reduces the need for manual labor and minimizes the risk of accidents associated with traditional material handling methods.
In the construction industry, the systems are used for transporting sand, gravel, and other aggregates to job sites, improving the speed and efficiency of construction projects. The closed system design also helps maintain the quality of the materials, preventing contamination from external sources and ensuring consistent performance in concrete and other building materials. For manufacturers, these systems offer a reliable way to transport raw materials and finished products, streamlining production processes and reducing the time and cost associated with material handling.
Overall, the combination of efficient material transport, environmental benefits, and operational flexibility makes ore sand pneumatic conveying systems a preferred choice for industries that require reliable and high-performance material handling solutions. HeadPowder's expertise in designing and manufacturing these systems ensures that clients receive tailored solutions that meet their specific needs, contributing to improved productivity and cost savings in their operations.