With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
High-alumina fly ash, a byproduct of coal combustion, is widely used in various industrial applications such as cement production, concrete manufacturing, and construction materials. The efficient and reliable transportation of this material is crucial for maintaining production efficiency and reducing operational costs. Pneumatic conveying systems, particularly those designed for high-alumina fly ash, offer a solution that minimizes dust emissions and ensures safe material handling. This article provides a detailed introduction to the high-alumina fly ash pneumatic conveying equipment, focusing on its structural design and operational principles.
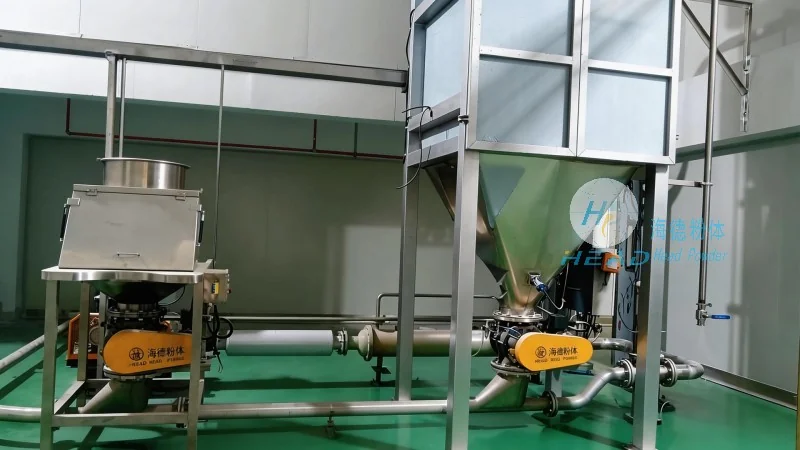
The high-alumina fly ash pneumatic conveying equipment typically consists of several key components that work in concert to achieve effective material transport. The main components include the hopper, feeder, air compressor, pipeline system, and receiver. Each component plays a vital role in the overall performance of the system.
The hopper is the initial storage unit where the high-alumina fly ash is loaded. It is designed with a sloped bottom to facilitate the material flow into the feeder. The feeder, often a rotary valve or a screw feeder, controls the flow rate of the material into the pipeline. This control is essential to maintain a consistent air-to-material ratio, which is critical for efficient pneumatic transport. The air compressor generates the necessary pressure to move the material through the pipeline. The pipeline system, made of durable materials such as stainless steel or special plastic, is designed to withstand the abrasive nature of the high-alumina fly ash. The receiver is the final storage unit where the material is deposited after being conveyed through the pipeline.
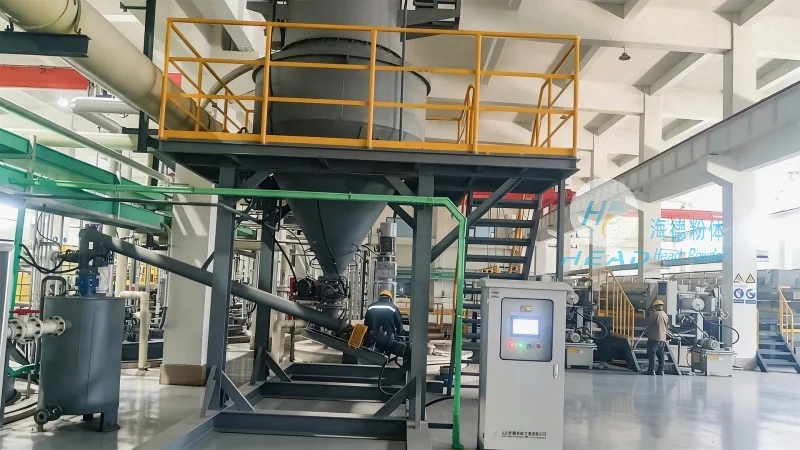
The operation of the high-alumina fly ash pneumatic conveying system follows a specific process. First, the high-alumina fly ash is fed into the hopper from a storage silo or truck. The feeder then regulates the material flow into the pipeline. Simultaneously, the air compressor supplies compressed air into the pipeline. The compressed air creates a flow that entrains the fly ash particles, forming a slurry-like mixture. This mixture travels through the pipeline under pressure, reaching the receiver where the air is separated from the material. The separated air is typically recycled back to the compressor, while the high-alumina fly ash is collected in the receiver for further use.
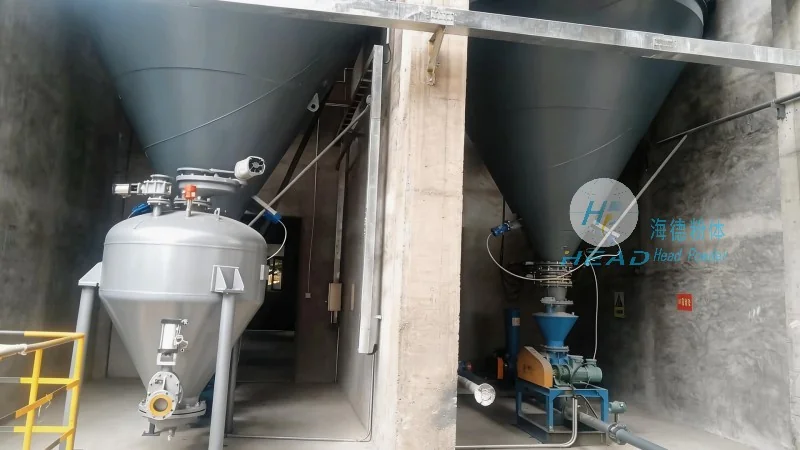
The air-to-material ratio is a critical parameter in the pneumatic conveying process. An optimal ratio ensures that the material is fully entrained and transported without clogging the pipeline. The system is designed to adjust this ratio dynamically based on the material characteristics and flow rate requirements. This adaptability makes the high-alumina fly ash pneumatic conveying equipment suitable for various industrial applications.
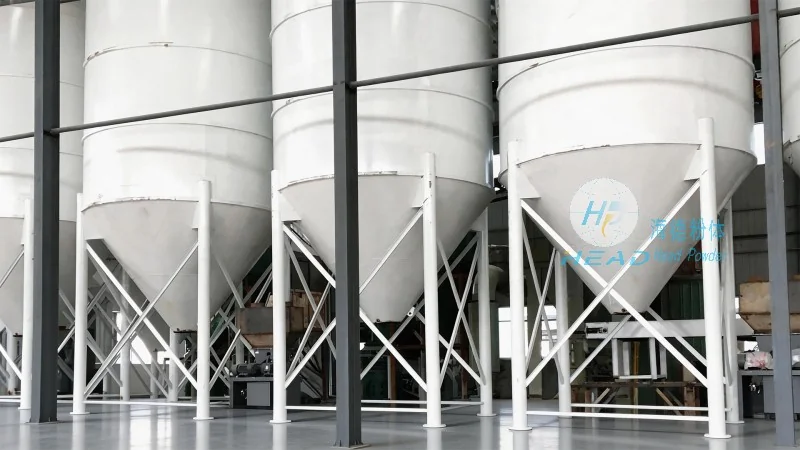
Implementing a high-alumina fly ash pneumatic conveying system offers several advantages over traditional methods such as belt conveyors or bucket elevators. One of the primary benefits is the reduction in dust emissions, which enhances workplace safety and compliance with environmental regulations. The system also minimizes material spillage and loss, as the material is contained within the pipeline. Additionally, the equipment is more compact and requires less floor space compared to traditional bulk handling systems. The automated operation of the system reduces labor costs and improves overall production efficiency. The durability of the components, especially the pipeline and feeder, ensures long-term reliability and low maintenance costs.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of pneumatic conveying equipment and related industrial solutions. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the bulk material handling industry. HeadPowder specializes in designing and manufacturing high-performance pneumatic conveying systems tailored to the specific needs of various industries, including cement, construction, and power generation. The company's products are known for their durability, efficiency, and compliance with international standards. HeadPowder's commitment to customer satisfaction and technical excellence has earned it a reputation for delivering reliable and cost-effective solutions for material handling challenges. The company's headquarters is located in Shandong, China, where it leverages local resources and expertise to serve global markets.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top