With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
When it comes to handling and transporting fine powders like aminoacetic acid, specialized equipment is essential to ensure efficiency, safety, and product integrity. The aminoacetic acid powder conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated solution tailored to meet the demands of modern industrial processes. This equipment is designed to address the unique challenges associated with conveying fine powders, such as dust generation, material segregation, and system reliability. By understanding the components and design principles behind this system, users can appreciate its role in optimizing production workflows and maintaining high standards of operational safety.
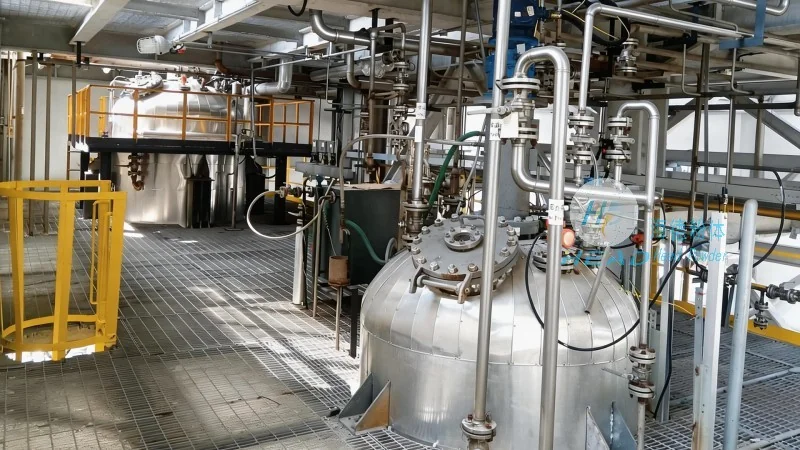
The aminoacetic acid powder conveying system typically consists of several critical components that work in tandem to facilitate smooth material transport. At the core of the system is a network of flexible or rigid conveying pipes, which are engineered to handle the specific properties of aminoacetic acid powder, including its particle size, moisture content, and flow characteristics. These pipes are often equipped with special liners or coatings to prevent material buildup and ensure consistent flow. The system also includes a drive unit, commonly a motor-driven fan or blower, which generates the necessary airflow to move the powder through the pipeline. This drive unit is usually integrated with a control panel that allows operators to adjust airflow speed and pressure, ensuring optimal performance. Additionally, the system may incorporate features like rotary valves or feeders at the inlet and outlet to regulate the flow rate and prevent backflow. These components collectively ensure that the powder is conveyed efficiently and without loss or contamination.
The design of the aminoacetic acid powder conveying system is guided by several fundamental principles that prioritize functionality, safety, and durability. One of the primary principles is the application of fluid dynamics, where the system is engineered to treat the powder as a fluid under controlled conditions. This approach allows for consistent and predictable material transport, reducing the risk of clogging or blockages. Material science plays a crucial role in the design, as the equipment is constructed from materials that are resistant to corrosion and chemical reactions with aminoacetic acid. For instance, stainless steel or specialized polymers are commonly used for components that come into direct contact with the powder, ensuring longevity and maintaining product purity. Another key principle is the integration of automation and control systems. Modern conveying systems are equipped with sensors and feedback mechanisms that monitor parameters such as pressure, temperature, and flow rate, allowing for real-time adjustments and preventing operational issues. This level of automation enhances operational efficiency and reduces the need for manual intervention, which is particularly important in environments where safety is paramount. Furthermore, the design emphasizes energy efficiency, with features like variable speed drives that adjust power consumption based on the conveying requirements. This not only reduces operational costs but also aligns with environmental sustainability goals.

The aminoacetic acid powder conveying system is widely used in various industrial sectors, including chemical manufacturing, pharmaceutical production, and food processing. In chemical plants, this equipment is essential for transporting raw materials and finished products, ensuring a seamless supply chain. The system's ability to handle fine powders without segregation or degradation makes it ideal for processes where product quality is critical. In pharmaceutical applications, the system's hygienic design and contamination control features are particularly valuable, as they help maintain compliance with regulatory standards. The operational efficiency of the system is a significant advantage, as it minimizes downtime and reduces the need for manual handling, which can be hazardous in powder handling environments. By automating the conveying process, the system also improves worker safety by reducing exposure to dust and other airborne particles. Additionally, the system's scalability allows it to be adapted to different production volumes, making it suitable for both small-scale and large-scale operations. This flexibility makes the aminoacetic acid powder conveying system a versatile solution for a wide range of industrial needs.
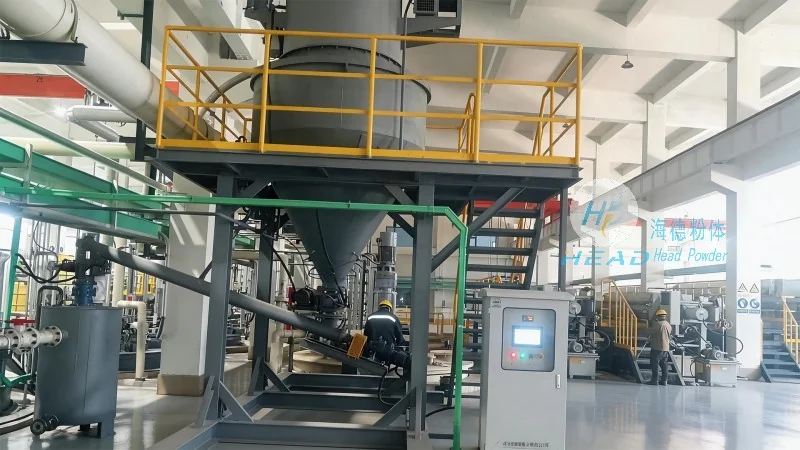
Over the years, the aminoacetic acid powder conveying system has undergone several technical advancements that enhance its performance and reliability. Innovations such as the use of positive displacement blowers, which provide consistent airflow regardless of system pressure, have improved the system's ability to handle difficult-to-convey powders. The integration of advanced control systems, including programmable logic controllers (PLCs) and remote monitoring capabilities, has further enhanced operational efficiency and troubleshooting capabilities. These systems allow for real-time data collection and analysis, enabling operators to identify and address issues before they escalate. In terms of industry standards, the system adheres to various regulations and guidelines, such as those set by the International Organization for Standardization (ISO) and the American Society of Mechanical Engineers (ASME). Compliance with these standards ensures that the equipment meets safety and performance requirements, providing users with confidence in its reliability. Additionally, the system's design incorporates features like explosion-proofing and dust suppression, which are critical in environments where fire or explosion risks are present. These technical advancements and adherence to industry standards reflect the commitment of Shandong HeadPowder Engineering Co., Ltd. to deliver high-quality, reliable equipment that meets the evolving needs of the industry.
In conclusion, the aminoacetic acid powder conveying system equipment is a sophisticated and essential tool for industries handling fine powders. Developed by Shandong HeadPowder Engineering Co., Ltd., this system combines advanced design principles, robust components, and automation to ensure efficient, safe, and reliable powder transport. By addressing the unique challenges of aminoacetic acid powder, the system enhances operational efficiency, reduces downtime, and maintains product integrity. The technical advancements and adherence to industry standards further solidify its position as a leading solution in the market. As a company based in China, Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted provider of specialized conveying equipment, with a focus on innovation and customer satisfaction. With its headquarters in Shandong, China, the company continues to serve a global clientele, delivering solutions that meet the diverse needs of modern industrial processes. The aminoacetic acid powder conveying system exemplifies the company's commitment to excellence and its role in advancing industrial efficiency and safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top