With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industries dealing with fine powders and granular materials, efficient material handling is a critical operational requirement. Synthetic fiber conveying systems, particularly those utilizing pneumatic conveying technology, have emerged as a reliable solution to address the challenges associated with traditional bulk material transport methods. This article provides an overview of synthetic fiber conveying systems, highlighting their key advantages and features, while introducing the capabilities of Shandong HeadPowder Engineering Co., Ltd. (hereinafter referred to as HeadPowder), a leading provider in this field.
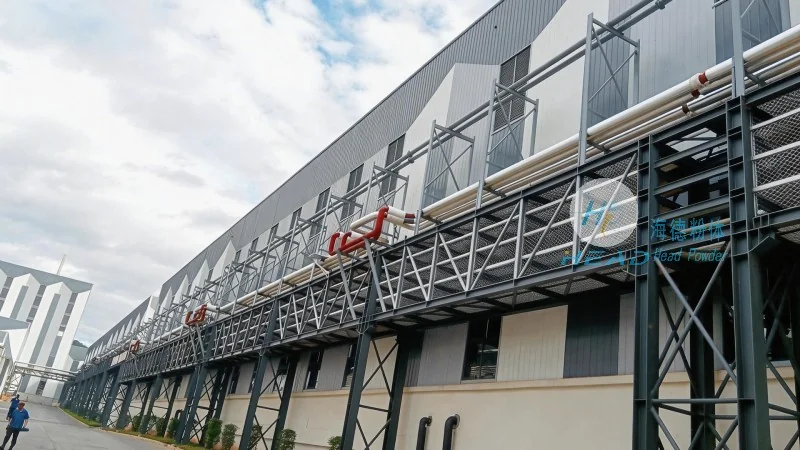
Synthetic fiber conveying systems are engineered to transport bulk materials through a network of flexible or semi-rigid hoses made from synthetic fibers. These systems operate on the principle of pneumatic conveying, where compressed air or other gases are used to move materials from a source to a destination. The synthetic fiber hoses offer several benefits over traditional metal or plastic hoses, including enhanced flexibility, resistance to abrasion, and improved durability under high-pressure conditions.
One of the primary advantages of synthetic fiber conveying systems is their ability to handle a wide range of materials, from fine powders to coarse granules. The flexible hose design allows for smooth material flow, reducing the risk of blockages and ensuring consistent throughput. Additionally, synthetic fibers are resistant to chemical corrosion, making them suitable for transporting materials that may be acidic or alkaline. This chemical resistance extends the service life of the conveying system, reducing maintenance costs and downtime.
Another significant benefit is the energy efficiency of synthetic fiber pneumatic conveying. Compared to traditional methods like bucket elevators or belt conveyors, pneumatic systems can achieve higher material transport rates with lower energy consumption. The reduced friction between the hose and the material, combined with optimized air flow, minimizes energy waste and contributes to lower operational costs over time.
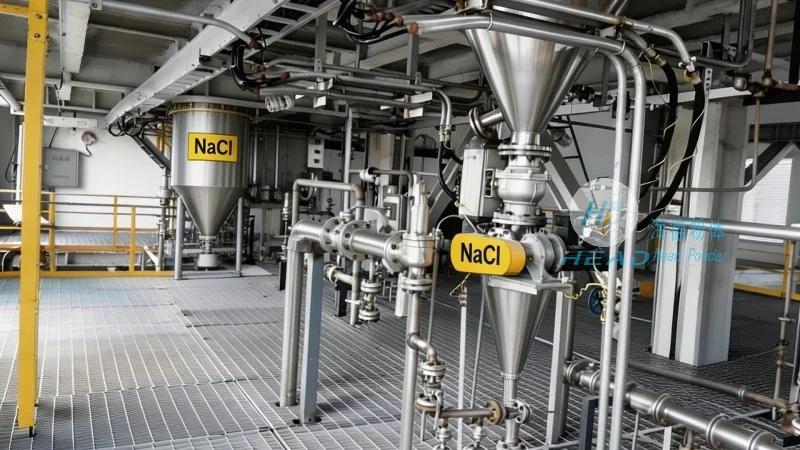
HeadPowder’s synthetic fiber conveying systems are designed with advanced features to enhance performance and reliability. The systems typically include components such as material feeders, air compressors, and control panels, all integrated to ensure seamless operation. The synthetic fiber hoses are available in various diameters and lengths, allowing customization to fit specific application requirements. Furthermore, the systems are equipped with safety features, including pressure relief valves and overheat protection, to prevent accidents and ensure operator safety.
From a technical perspective, synthetic fiber conveying systems operate at pressures ranging from low to high, depending on the material being transported. The air flow rate is carefully controlled to maintain optimal material velocity, preventing material degradation or caking. The systems also incorporate filtration and separation mechanisms to ensure that the conveyed material remains clean and free from contaminants, which is crucial for industries where material purity is essential.
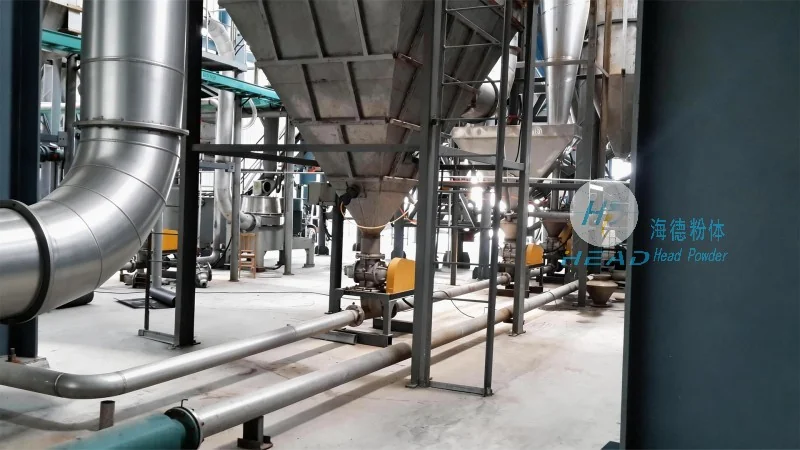
Synthetic fiber conveying systems find applications in numerous industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. In the pharmaceutical industry, for example, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the materials remain sterile and free from cross-contamination. In food processing, the systems handle ingredients like flour, sugar, and spices, maintaining hygiene standards and preventing product spoilage. The chemical industry utilizes synthetic fiber conveying for transporting acids, bases, and other corrosive materials, leveraging the chemical resistance of the synthetic fibers to protect both the equipment and the materials being handled.
In the mining sector, synthetic fiber conveying systems are employed to transport ore and other bulk materials from mines to processing facilities. The flexibility of the hoses allows for easy installation in complex mine layouts, while the high durability of the synthetic fibers withstands the harsh conditions of underground operations. The energy efficiency of the systems also contributes to cost savings in remote mining locations where power is a limited resource.
Synthetic fiber conveying systems represent a modern and efficient solution for bulk material transport, offering significant advantages over traditional methods. With their ability to handle diverse materials, resistance to corrosion, and energy efficiency, these systems are increasingly adopted across various industries. Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of synthetic fiber conveying systems, providing tailored solutions to meet the specific needs of clients. HeadPowder’s commitment to quality and innovation ensures that their systems deliver reliable performance and long-term value, making them a trusted partner for industries seeking advanced material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top