With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Heavy calcium carbonate (often abbreviated as heavy calcium) is a widely used industrial material in various sectors such as plastics, coatings, paper, and construction. The efficient and reliable transportation of heavy calcium carbonate from production sites to processing facilities is crucial for maintaining production efficiency and product quality. This article introduces the heavy calcium carbonate conveying system, focusing on the advantages and characteristics of pneumatic conveying technology.
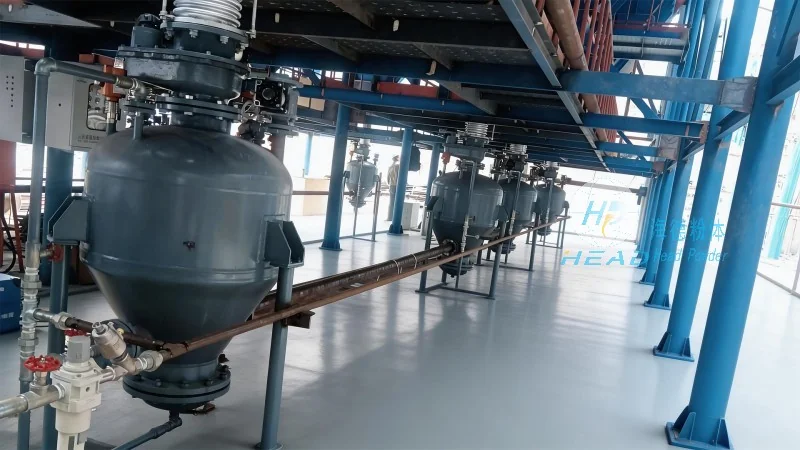
Heavy calcium carbonate conveying systems are engineered to handle the transportation of heavy calcium carbonate powder or granules from storage silos, production lines, or processing units to the next stage of manufacturing. These systems are designed to ensure minimal material loss, maintain product purity, and operate with high efficiency. The core components of a typical heavy calcium carbonate conveying system include storage silos, feeders, conveying pipes, and discharge units. The system's design is tailored to the specific characteristics of heavy calcium carbonate, such as its particle size, moisture content, and bulk density, to optimize performance.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer and supplier of advanced material handling equipment. With a strong focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the heavy calcium carbonate industry. The company's expertise lies in designing and manufacturing customized conveying systems that meet the unique requirements of clients. HeadPowder's team of engineers and technicians work closely with clients to understand their operational needs and develop tailored solutions. The company's facilities are equipped with state-of-the-art technology and quality control measures to ensure that every product meets the highest standards. HeadPowder is committed to providing reliable and efficient conveying solutions that enhance the productivity and profitability of its clients' operations.
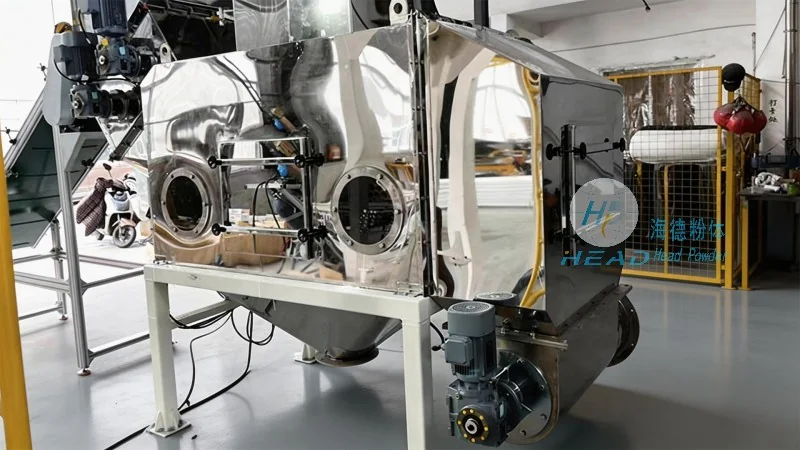
Pneumatic conveying is a widely adopted method for transporting heavy calcium carbonate due to its numerous advantages over traditional mechanical conveying systems. This technology uses air or gas to move the material through a network of pipes, eliminating the need for mechanical components like belts or chains. The primary benefits of pneumatic conveying for heavy calcium carbonate include high conveying capacity, flexibility in system layout, and reduced maintenance requirements. Pneumatic systems can handle a wide range of particle sizes and moisture levels, making them suitable for various applications. Additionally, these systems offer better control over material flow, which is essential for maintaining product quality and preventing contamination. The efficiency of pneumatic conveying is further enhanced by the use of advanced control systems that optimize air pressure and flow rates, ensuring consistent and reliable material transport.
Several key advantages make pneumatic conveying an ideal choice for heavy calcium carbonate transportation. Firstly, the system offers high conveying efficiency, allowing for the movement of large quantities of material over long distances with minimal energy consumption. This is particularly beneficial for industrial applications where large volumes of heavy calcium carbonate need to be transported. Secondly, pneumatic conveying provides excellent material handling flexibility. The system can be easily reconfigured or expanded to accommodate changes in production volume or process requirements. This adaptability is crucial for businesses operating in dynamic market conditions. Thirdly, the technology reduces operational costs by minimizing material loss and lowering maintenance expenses. Unlike mechanical systems, which are prone to wear and tear, pneumatic conveying systems have fewer moving parts, resulting in lower maintenance requirements and longer service life. Fourthly, pneumatic conveying enhances product quality by preventing contamination and maintaining the integrity of the material. The enclosed system design ensures that heavy calcium carbonate remains free from external pollutants, which is critical for applications where product purity is paramount. Finally, the system offers improved safety features compared to traditional methods. The absence of mechanical components reduces the risk of accidents and provides a safer working environment for personnel.
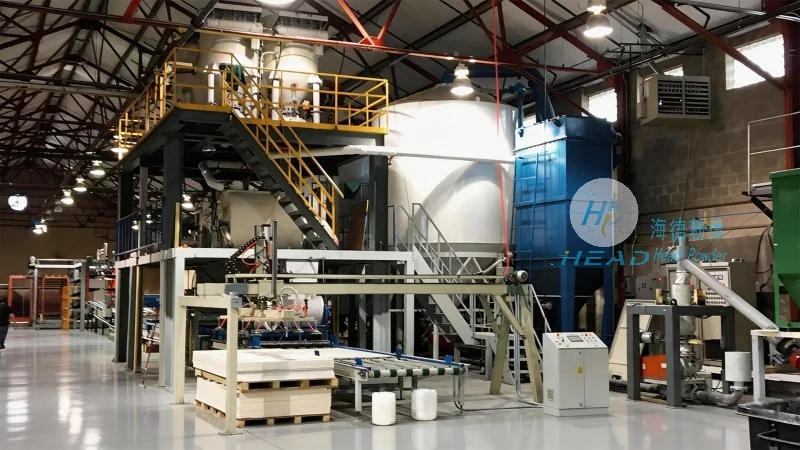
HeadPowder understands that each client's operational requirements are unique, and therefore, the company offers customized heavy calcium carbonate conveying systems. The design process begins with a thorough analysis of the client's production process, material characteristics, and operational goals. Based on this analysis, HeadPowder's engineers develop a tailored solution that optimizes material flow, minimizes energy consumption, and enhances overall system performance. The company's expertise in material handling allows it to integrate conveying systems with other processing equipment, such as mixers, grinders, or storage silos, to create a seamless production line. This integration ensures that the heavy calcium carbonate is transported efficiently from one stage to the next without any bottlenecks. HeadPowder also provides post-installation support, including maintenance services and technical assistance, to ensure that the conveying system operates at peak performance throughout its lifecycle. By offering customized and integrated solutions, HeadPowder helps its clients achieve higher productivity, lower operational costs, and improved product quality.
As the demand for heavy calcium carbonate continues to grow in various industries, the importance of efficient and reliable conveying systems cannot be overstated. Pneumatic conveying, with its numerous advantages, is set to remain a preferred method for transporting heavy calcium carbonate. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing advanced conveying solutions that meet the evolving needs of the industry. By leveraging the benefits of pneumatic conveying and customized system design, businesses can enhance their operational efficiency, reduce costs, and maintain product quality. The future of heavy calcium carbonate conveying lies in the continued innovation and adoption of advanced technologies that optimize material handling processes. With the right equipment and expertise, companies can achieve sustainable growth and remain competitive in the global market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top