With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
White sugar, as a crucial raw material in the food and beverage industry, requires efficient and reliable material handling solutions to ensure smooth production processes. The principles and working scene characteristics of white sugar material handling systems are vital for optimizing workflow, maintaining product quality, and enhancing operational efficiency in sugar processing facilities. This article explores the core principles behind white sugar material handling, along with the specific characteristics of different working scenes, providing insights into how these systems operate and their practical applications.
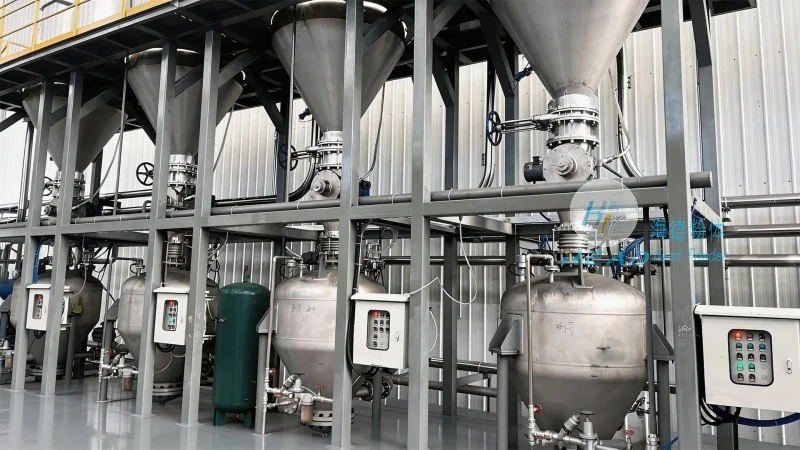
The material handling of white sugar is governed by several key principles that ensure safety, efficiency, and product integrity. First, the principle of contamination prevention is paramount, as white sugar is highly susceptible to impurities from the environment or equipment. This necessitates the use of clean, sealed systems to maintain hygiene standards. For instance, stainless steel components and sealed conveyor belts are commonly used to prevent dust and moisture from entering the system, which could compromise the purity of the sugar. Second, the principle of energy efficiency plays a significant role, as sugar processing facilities often operate continuously and require cost-effective solutions to reduce operational expenses. Modern material handling systems utilize energy-saving motors and optimized airflow designs to minimize energy consumption without sacrificing performance. Third, the principle of scalability is essential, as sugar production volumes can vary, and systems must be adaptable to accommodate changes in demand. Modular designs and adjustable conveyor speeds allow facilities to scale up or down their material handling capacity as needed, providing flexibility in response to market fluctuations. Finally, the principle of durability is critical, as sugar handling equipment is exposed to abrasive particles and high-temperature environments, demanding robust construction to withstand wear and tear. Heavy-duty bearings and corrosion-resistant materials are used to extend the lifespan of the equipment, reducing the frequency of replacements and maintenance costs.
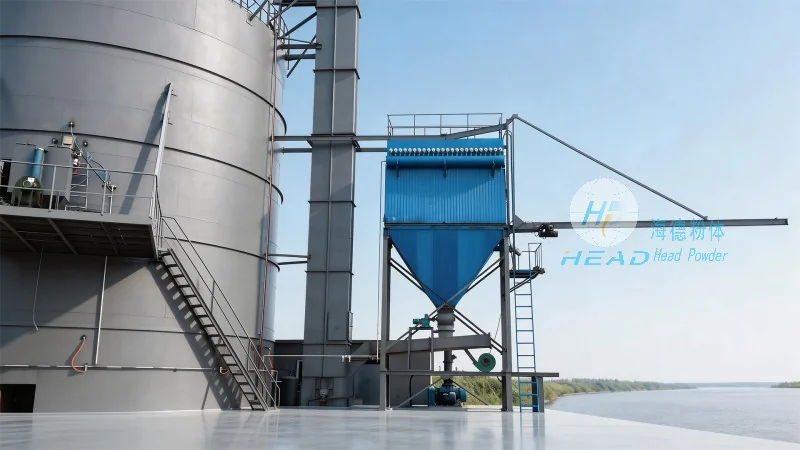
The working scene characteristics of white sugar material handling systems vary based on the stage of production and the specific application. In the raw sugar processing stage, material handling involves the transfer of raw sugar from storage silos to processing equipment, often using conveyor belts or pneumatic systems. The working scene here is characterized by large volumes of bulk material and the need for gentle handling to prevent clumping or breakage. During the refining process, the material handling focuses on transporting refined sugar, which requires more precise control to avoid particle size variations. The working scene in this phase is marked by high-speed operations and the need for consistent flow rates. In the packaging stage, the material handling involves moving finished sugar products to packaging lines, where the working scene is characterized by smaller batch sizes and the need for accurate weighing and distribution. Each of these working scenes demands tailored solutions to meet the unique challenges of white sugar handling, from bulk storage to final product delivery.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing systems tailored for the sugar industry. With a focus on innovation and customer-centric approaches, the company has established itself as a trusted partner for sugar processing facilities worldwide. HeadPowder's expertise lies in understanding the specific requirements of white sugar material handling, from raw material transfer to final product packaging. The company's team of engineers and technicians work closely with clients to develop customized solutions that address their unique operational challenges, ensuring optimal performance and reliability. HeadPowder's commitment to quality and efficiency has made it a preferred choice for sugar manufacturers seeking to enhance their material handling processes. The company's headquarters are located in Shandong, China, where it leverages local manufacturing capabilities and regional expertise to serve global markets.
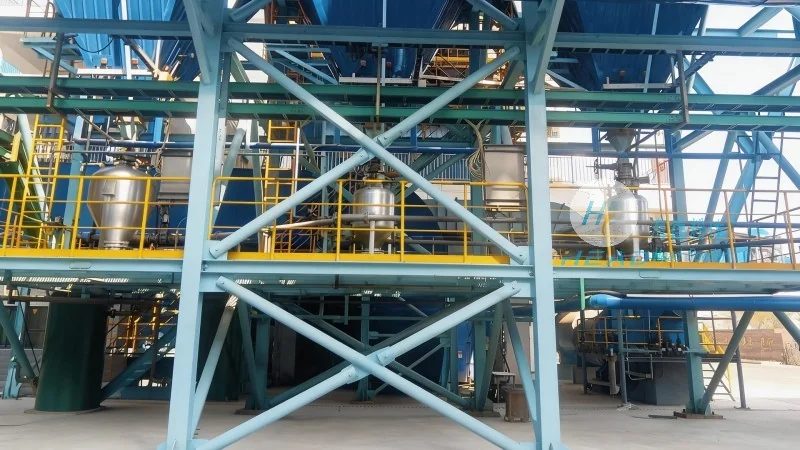
White sugar material handling systems from HeadPowder are equipped with several key features that enhance their performance and adaptability. One of the primary features is the use of stainless steel construction, which provides excellent resistance to corrosion and maintains hygiene standards in food processing environments. The systems also incorporate advanced control systems, allowing for precise regulation of flow rates and operational parameters. Additionally, the use of pneumatic conveying technology enables efficient and low-maintenance material transfer, reducing the need for frequent maintenance and downtime. The systems are designed with safety in mind, incorporating features such as overload protection and emergency stop mechanisms to prevent accidents and ensure operator safety. These features collectively contribute to the overall efficiency and reliability of white sugar material handling operations. Furthermore, HeadPowder's systems are equipped with monitoring and diagnostic tools that allow for real-time performance tracking and predictive maintenance, helping facilities to proactively address issues and minimize disruptions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top