With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Intelligent ingredient and material conveying systems have become a cornerstone in modern industrial operations, particularly in sectors requiring precise and efficient handling of raw materials. These systems integrate advanced technologies to enhance productivity, reduce human error, and ensure compliance with industry standards. As businesses strive for higher efficiency and cost-effectiveness, the adoption of such systems has grown significantly, making them indispensable in manufacturing, pharmaceuticals, food processing, and other industries where material handling is critical.
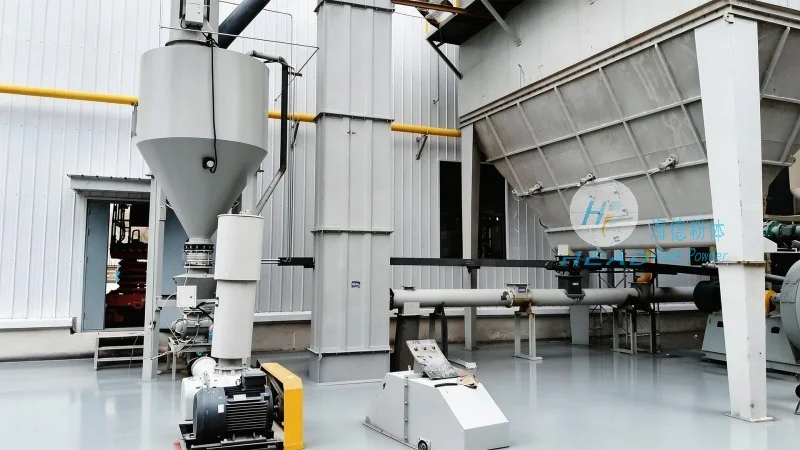
The core working principle of these systems revolves around the seamless integration of sensors, automation controls, and real-time data processing. At the heart of the system is a network of conveyors, hoppers, and feeding mechanisms that work in tandem to transport ingredients and materials from storage to processing units. The process typically begins with the loading of raw materials into designated hoppers, where sensors detect the level and type of material. This information is then transmitted to a central control unit, which manages the flow rate and direction of the conveying process. Advanced systems may incorporate artificial intelligence (AI) and machine learning algorithms to optimize the conveying path, adjust speed based on material characteristics, and predict maintenance needs, thereby minimizing downtime and maximizing operational efficiency.
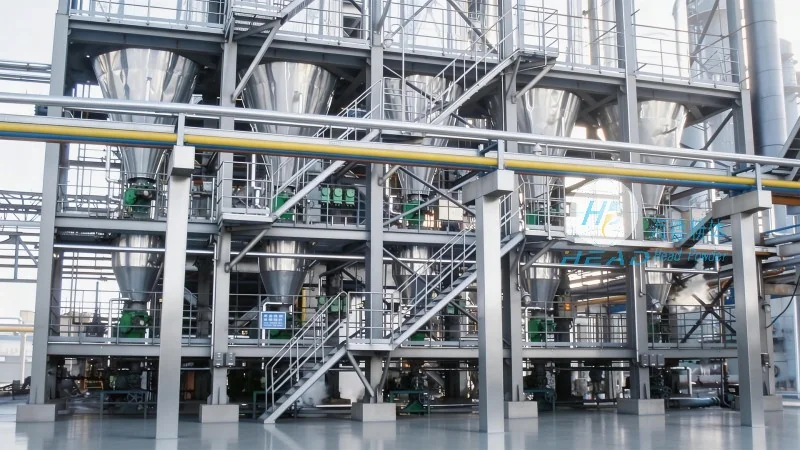
Intelligent ingredient and material conveying systems are distinguished by several key features that set them apart from traditional manual or semi-automated systems. Firstly, real-time monitoring and control is a hallmark of these systems. Equipped with sensors and IoT (Internet of Things) devices, they provide continuous feedback on material levels, flow rates, and system performance. This allows operators to make immediate adjustments, ensuring that the conveying process remains within optimal parameters. Secondly, precision and accuracy are critical features. The systems are designed to handle a wide range of material types, from powders and granules to bulk solids, with minimal segregation or loss. This is achieved through specialized feeding mechanisms, such as vibratory feeders or rotary valves, which maintain consistent material flow and prevent clogging or bridging. Thirdly, automation and integration capabilities are a major advantage. These systems can be integrated with other production equipment, such as mixers, blenders, or packaging machines, creating a fully automated production line. This integration reduces the need for manual intervention, enhances safety, and improves overall throughput. Additionally, data analytics and reporting features enable businesses to track performance metrics, identify bottlenecks, and make data-driven decisions to further optimize operations. The systems can generate detailed reports on material usage, conveyor efficiency, and maintenance schedules, providing valuable insights for process improvement.
The versatility of intelligent ingredient and material conveying systems makes them suitable for a wide range of applications across various industries. In the pharmaceutical industry, for example, these systems ensure the precise handling of active pharmaceutical ingredients (APIs) and excipients, maintaining strict quality control and preventing contamination. In the food processing sector, they facilitate the efficient transport of raw ingredients like flour, sugar, and spices, while adhering to food safety regulations. The manufacturing industry benefits from the systems' ability to handle bulk materials, such as metal powders or plastic pellets, in high-volume production lines. The primary benefits of these systems include increased productivity, reduced labor costs, improved product quality, and enhanced safety. By automating the material handling process, businesses can achieve higher throughput while minimizing human error, which is particularly important in industries where precision and consistency are paramount. Furthermore, the integration of data analytics allows for proactive maintenance, reducing unexpected downtime and extending the lifespan of equipment. This leads to long-term cost savings and improved operational reliability.
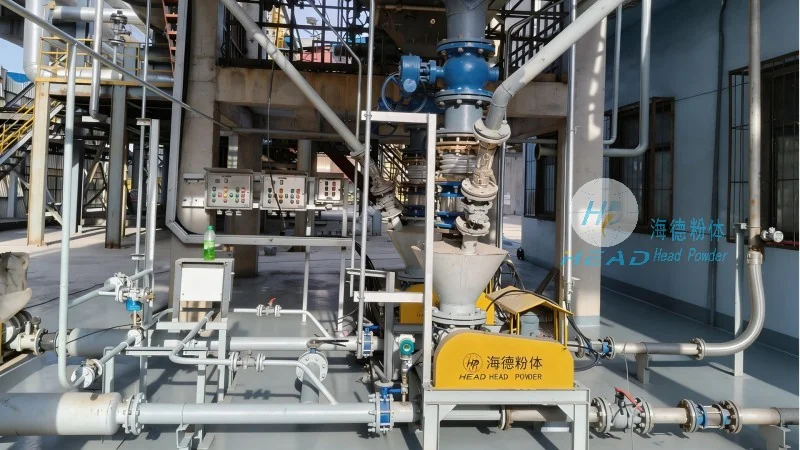
In conclusion, intelligent ingredient and material conveying systems represent a significant advancement in industrial material handling technology. Their ability to combine precision, automation, and real-time monitoring makes them essential for modern manufacturing operations. As industries continue to evolve and demand higher efficiency, these systems will play an increasingly vital role in ensuring productivity and competitiveness. Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field, specializes in designing and manufacturing customized conveying solutions tailored to the specific needs of clients. With a focus on innovation and quality, the company has established itself as a trusted partner in the industry, delivering systems that meet the highest standards of performance and reliability. Based in Shandong, China, HeadPowder leverages its expertise to help businesses optimize their material handling processes, drive efficiency, and achieve their operational goals. Whether for new installations or system upgrades, HeadPowder's intelligent conveying systems offer a reliable and efficient solution for businesses seeking to enhance their production capabilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top