With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Calcium nitrite is a widely used chemical compound in various industrial applications, and the efficient handling of this material is crucial for maintaining production efficiency and safety standards. The calcium nitrite material handling equipment developed by Shandong HeadPowder Engineering Co., Ltd. is designed to meet the demanding requirements of modern industrial processes, ensuring reliable and safe material transport. This article provides a detailed overview of the operation process and working principle of such equipment, highlighting the key components and operational mechanisms that contribute to its effectiveness.
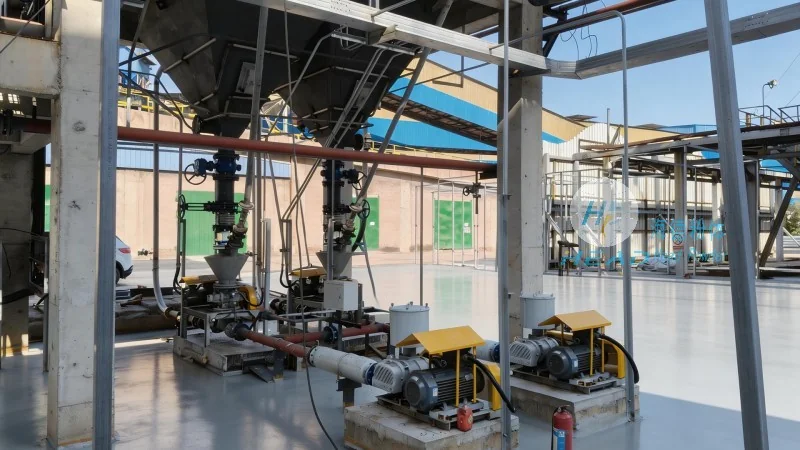
The calcium nitrite material handling equipment typically consists of several integrated components, including feeders, conveyors, storage silos, and control systems. These components work in tandem to facilitate the seamless transfer of calcium nitrite from storage to processing units. The equipment is engineered to handle the specific physical and chemical properties of calcium nitrite, such as its granular or powder form, ensuring minimal degradation or contamination during transport. Shandong HeadPowder Engineering Co., Ltd. specializes in customizing these systems to suit the unique needs of each client, whether for bulk storage, intermediate handling, or final discharge.
At the core of the calcium nitrite material handling system are several critical components that ensure smooth operation. The feeders, often equipped with variable speed drives, regulate the flow rate of the material into the conveyor system, preventing overloading or underflow. The conveyors, which may include screw conveyors, belt conveyors, or pneumatic systems, transport the calcium nitrite from the storage silo to the processing area. Storage silos are designed with appropriate aeration and discharge mechanisms to maintain material flowability and prevent caking, a common issue with calcium nitrite due to its hygroscopic nature. The control system, integrated with sensors and programmable logic controllers (PLCs), monitors and adjusts the operation of each component in real-time, ensuring optimal performance and safety compliance.
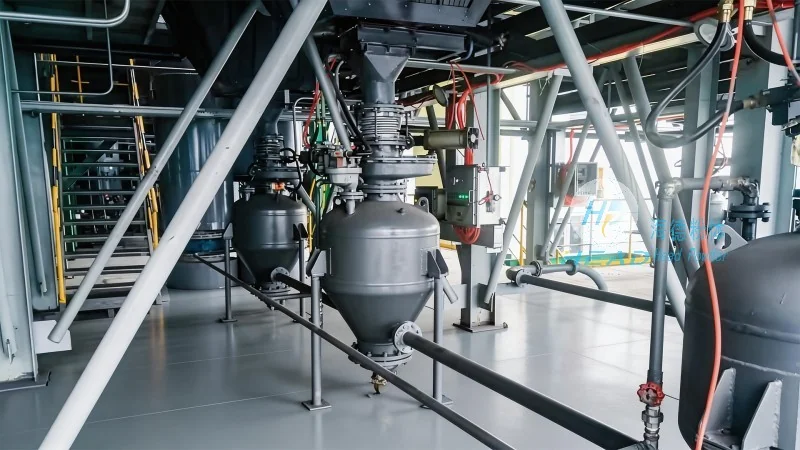
The operation of calcium nitrite material handling equipment follows a systematic process that begins with material loading into the storage silo. The first step involves the initial charging of the silo, where bulk calcium nitrite is introduced through a hopper or loading port. Once the silo is filled, the feeder system activates, gradually releasing the material into the conveyor. The conveyor then transports the calcium nitrite to the processing unit or discharge point. Throughout this process, the control system continuously monitors parameters such as flow rate, pressure, and temperature to ensure that the material is handled within safe and efficient limits. The system may also include safety features like emergency stop buttons and overload protection to prevent accidents or equipment damage.
The working principle of calcium nitrite material handling equipment combines mechanical movement with advanced control technology to achieve precise material transport. The mechanical components, such as conveyors and feeders, rely on motor-driven mechanisms to move the material along the designated path. For example, a screw conveyor uses rotating screws to push the material forward, while a belt conveyor uses a moving belt to transport it. The control system, equipped with sensors like level detectors and flow meters, provides real-time data on the material status. This data is processed by the PLC, which adjusts the speed of the motors and the operation of the feeders to maintain consistent flow. The integration of these mechanical and control elements ensures that the equipment operates efficiently, minimizing energy consumption and maximizing throughput. Additionally, the system is designed to handle the potential hazards associated with calcium nitrite, such as dust generation and chemical reactivity, through proper sealing and ventilation mechanisms.
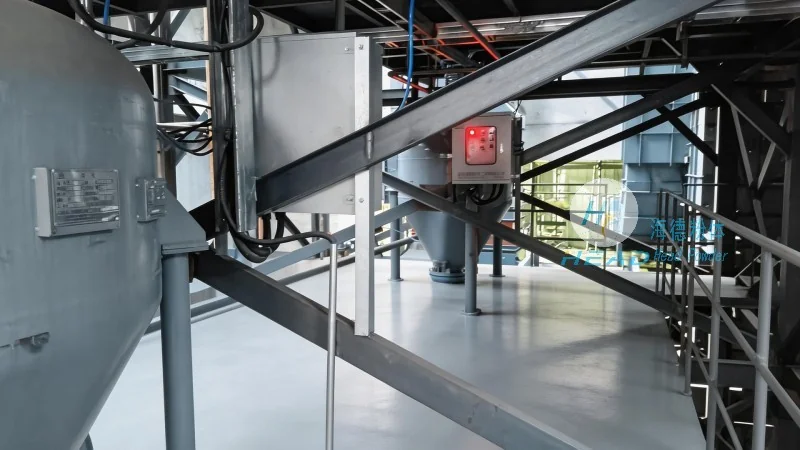
The calcium nitrite material handling equipment from Shandong HeadPowder Engineering Co., Ltd. offers several advantages that make it suitable for various industrial applications. The equipment is designed for high reliability and low maintenance, reducing downtime and operational costs. The modular design allows for easy installation and integration into existing production lines, making it a flexible solution for different production scales. The system also ensures compliance with safety regulations by incorporating features like dust suppression and explosion-proof designs, which are critical for handling potentially hazardous materials like calcium nitrite. These advantages make the equipment ideal for industries such as food processing, water treatment, and chemical manufacturing, where consistent and safe material handling is essential for product quality and regulatory compliance.
In conclusion, the calcium nitrite material handling equipment developed by Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated solution for the efficient and safe transport of calcium nitrite. By integrating advanced mechanical components with intelligent control systems, the equipment ensures reliable operation while minimizing risks associated with material handling. The detailed operation process and working principle outlined in this article highlight the engineering expertise behind the design, emphasizing the importance of tailored solutions for industrial applications. As industries continue to demand higher efficiency and safety standards, such equipment plays a vital role in maintaining production continuity and meeting regulatory requirements. Shandong HeadPowder Engineering Co., Ltd. remains committed to providing innovative material handling solutions that address the evolving needs of its clients, ensuring long-term success in the industrial sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top