With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding the working principle and characteristics of dilute phase material handling systems is crucial for industries that rely on efficient and reliable bulk material transport. These systems are designed to move powders, granules, and other particulate materials through a pipeline using a high-velocity air stream, creating a suspended flow where the material is dispersed in the air. This approach offers significant advantages in terms of energy efficiency, reduced equipment wear, and the ability to handle a wide range of materials.
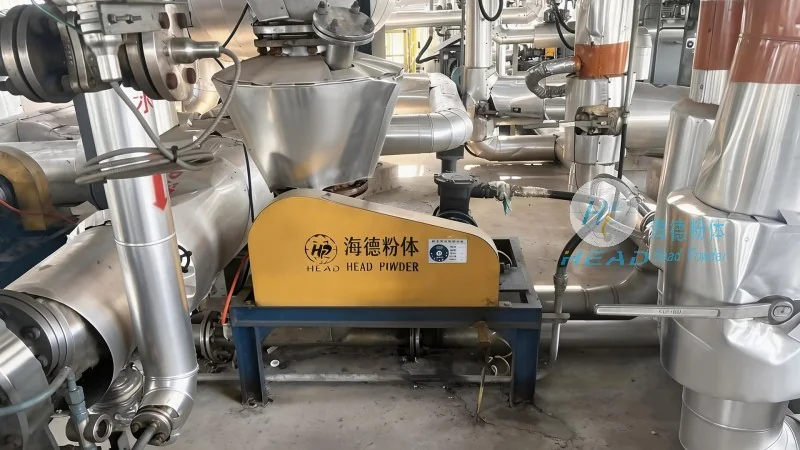
The core mechanism of dilute phase material handling systems involves the use of a high-pressure air compressor to generate a powerful air stream. The material to be transported is introduced into the pipeline at the inlet, where it is immediately entrained by the air flow. As the material particles become suspended in the air, they travel through the pipeline at a velocity sufficient to maintain the suspended state. The system typically includes components such as a feeder, a pipeline, and a receiver, with the air flow being controlled to ensure optimal transport conditions. The working principle is based on the principle of fluidization, where the material behaves like a fluid under the influence of the air stream, allowing for smooth and continuous transport without the need for mechanical conveyors in many cases.
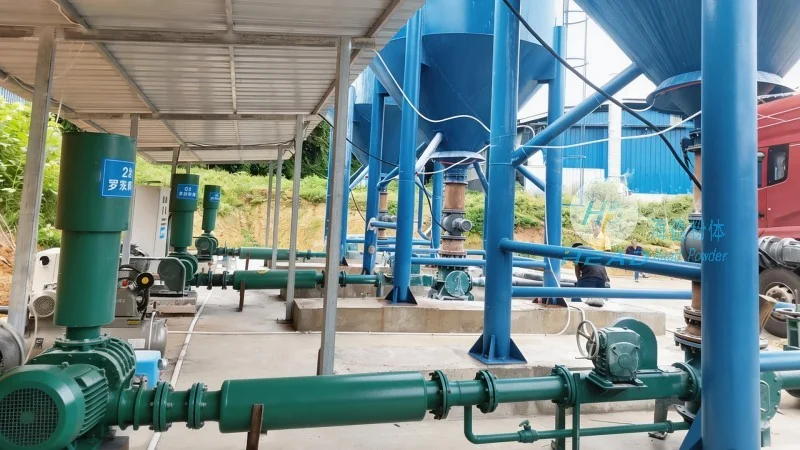
Dilute phase material handling systems exhibit several distinct characteristics that make them suitable for various industrial applications. One of the primary advantages is their high transport efficiency, as the suspended flow allows for the movement of large quantities of material over long distances with minimal energy consumption. Additionally, these systems are highly flexible, capable of handling a wide variety of materials, including fine powders, coarse granules, and even abrasive particles, without causing excessive wear on the equipment. The systems also offer excellent scalability, with the ability to adjust the air flow and pressure to accommodate different material types and transport requirements. Another important characteristic is the reduced risk of material degradation, as the air stream minimizes direct contact between particles and the pipeline walls, preventing issues such as caking or agglomeration. Furthermore, dilute phase systems are generally more compact and easier to install compared to traditional dense phase or mechanical conveyors, making them a practical choice for space-constrained environments.
Dilute phase material handling systems are widely used in industries such as pharmaceuticals, food processing, chemicals, and mining, where the transport of bulk materials requires precision and reliability. The benefits of these systems extend beyond efficiency and flexibility, as they also contribute to improved safety and operational stability. For example, in pharmaceutical manufacturing, the use of dilute phase systems ensures that powders are handled in a clean and controlled manner, minimizing contamination risks. In food processing, the systems maintain the quality of ingredients by preventing moisture absorption or temperature changes during transport. The ability to handle abrasive materials without significant equipment damage also makes these systems ideal for mining operations, where the transport of ores and other minerals is a critical process. Overall, the characteristics of dilute phase material handling systems align well with the demands of modern industrial processes, providing a cost-effective and sustainable solution for bulk material transport.
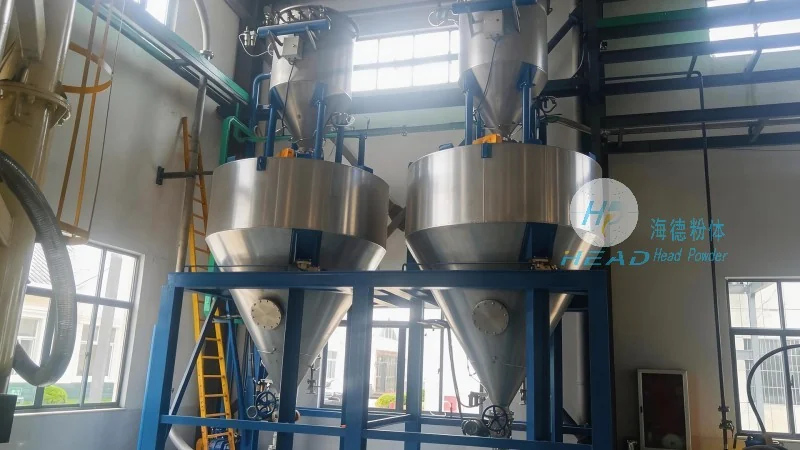
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of material handling equipment, specializing in the design and production of dilute phase material handling systems. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner for industries seeking reliable and efficient bulk material transport solutions. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled personnel. HeadPowder's team of engineers and technicians work closely with clients to understand their specific material handling needs and develop customized solutions that meet their operational requirements. By leveraging years of experience and expertise in the field, HeadPowder ensures that its products are not only efficient but also durable and easy to maintain, providing long-term value to its customers. The company's focus on customer satisfaction and technical excellence has earned it a reputation as a leading provider of material handling systems in the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top