With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Rice husk ash, a byproduct of rice processing, is increasingly recognized for its applications in construction and industrial processes. Efficient material handling of this material is crucial for optimizing production workflows and ensuring consistent quality. This article explores the working principle and key features of rice husk ash material handling systems, highlighting the technical advancements and operational benefits offered by specialized equipment designed for this specific material.
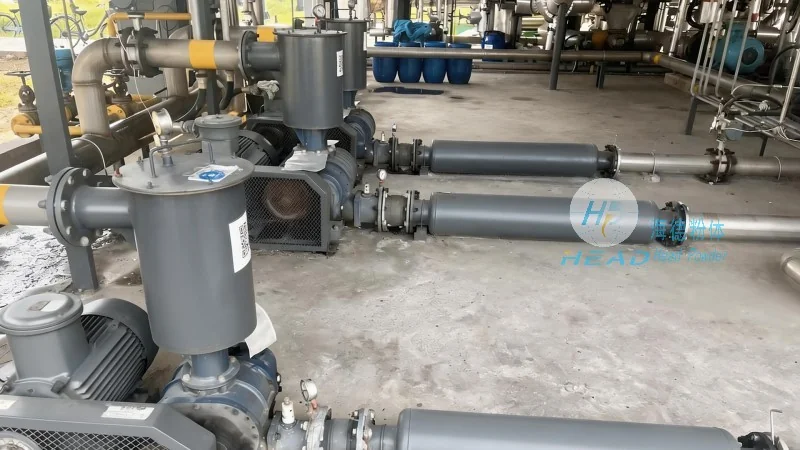
Rice husk ash, also known as rice husk ash (RHA), is a lightweight, porous material derived from the combustion of rice husks. It is widely used as a supplementary cementitious material in concrete, a raw material in the production of activated carbon, and a component in various industrial applications. The effective transport and handling of RHA are essential to maintain its physical properties and ensure seamless integration into downstream processes. Material handling systems for rice husk ash must address challenges such as dust generation, material flow variability, and the need for gentle handling to preserve particle integrity.
The working principle of rice husk ash material handling typically involves a combination of mechanical and pneumatic systems tailored to the material's characteristics. Conveying systems, such as belt conveyors, screw conveyors, and pneumatic conveyors, are commonly employed to transport RHA from storage silos or processing units to production lines. Belt conveyors are preferred for bulk material transport due to their high capacity and ability to handle large volumes of RHA with minimal maintenance. Screw conveyors, on the other hand, are suitable for vertical or inclined transport, providing precise control over material flow and preventing blockages. Pneumatic conveyors, utilizing air pressure to move material through pipes, offer advantages in dust containment and flexibility in system layout, making them ideal for applications requiring enclosed material transport.
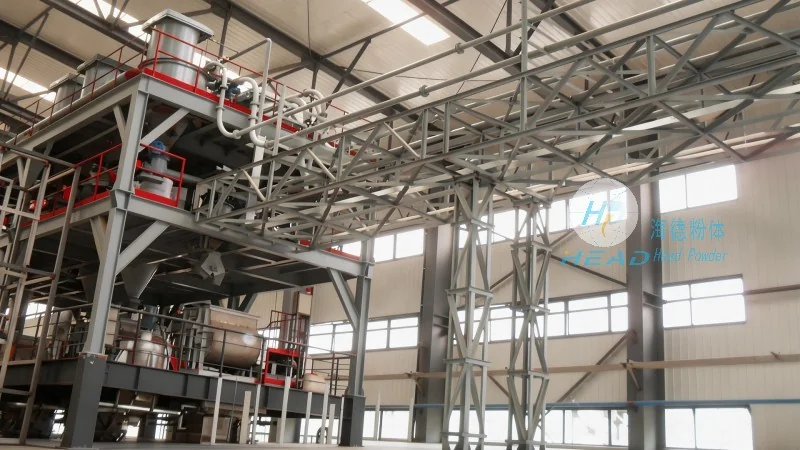
Advanced rice husk ash material handling solutions are characterized by several key features that enhance efficiency and reliability. One of the primary features is the integration of dust control mechanisms, such as enclosed conveyor systems and filtration units, to minimize environmental impact and ensure workplace safety. Another critical feature is the use of variable speed drives and adjustable conveyor components, allowing operators to optimize material flow rates based on production demands. Additionally, many systems incorporate material sensors and monitoring technologies to detect blockages, overloads, or changes in material consistency, enabling proactive maintenance and preventing process disruptions. The design of these systems also emphasizes energy efficiency, with features like low-friction components and optimized airflow to reduce operational costs.
The technical advantages of rice husk ash material handling systems extend beyond basic transport capabilities. For instance, the use of high-quality, wear-resistant materials in conveyor components ensures longevity and reduces the need for frequent replacements, thereby lowering long-term maintenance costs. The integration of automated control systems allows for seamless integration with existing production lines, improving overall operational efficiency and reducing labor requirements. Furthermore, the ability to handle RHA in both dry and slightly moist conditions without compromising material quality is a significant advantage, as it accommodates various processing requirements. The systems also support scalability, enabling easy expansion to accommodate increased production volumes or new application requirements without major system overhauls.
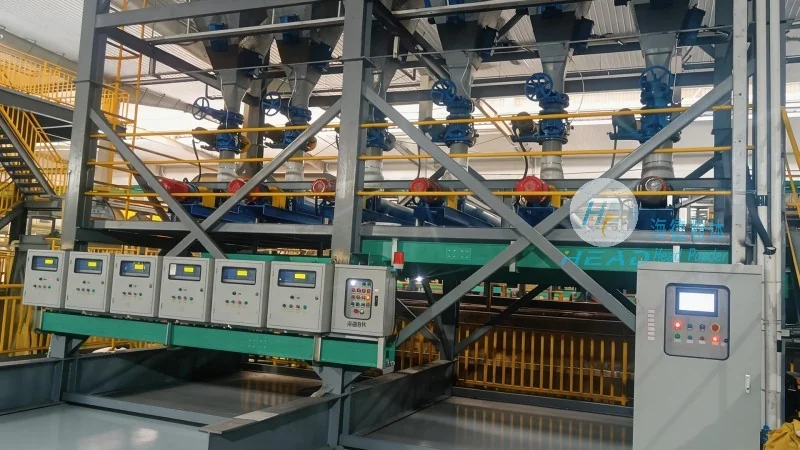
Rice husk ash material handling systems are widely applied in various industrial settings, including cement manufacturing plants, construction material production facilities, and activated carbon production units. In cement plants, for example, RHA is transported from storage silos to mixing stations where it is blended with cement clinker and other raw materials. The efficient handling of RHA ensures consistent mixing ratios, leading to improved concrete strength and durability. In activated carbon production, RHA is transported to reactors where it undergoes further processing to enhance its adsorption properties. The operational benefits of these systems include reduced downtime due to fewer maintenance issues, improved material quality control, and enhanced safety through dust containment measures. Additionally, the ability to handle RHA in bulk quantities minimizes material handling costs and optimizes production throughput.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing systems tailored to the unique requirements of rice husk ash and other similar materials. With a strong focus on innovation and customer-centric solutions, the company has developed advanced technologies that address the challenges of RHA material handling. HeadPowder's expertise lies in the integration of mechanical, pneumatic, and control systems, ensuring that their solutions are both efficient and reliable. The company's facilities are located in Shandong, China, where it leverages local resources and expertise to deliver high-quality products and services. By combining years of industry experience with cutting-edge technology, HeadPowder has established itself as a trusted partner for businesses seeking to optimize their rice husk ash material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top