With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
What is a Calcined Limestone Material Conveying Line? What Are Its Design Principles?
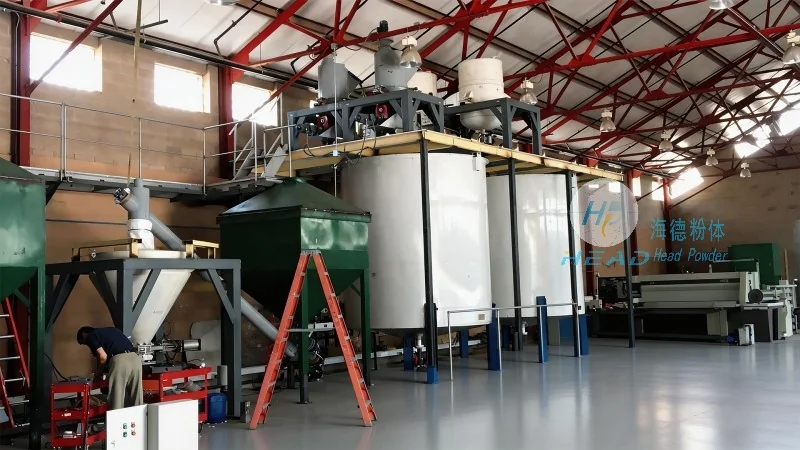
Calcined limestone, a crucial raw material in various industrial processes, requires efficient and reliable transportation systems to ensure smooth workflow. A calcined limestone material conveying line is a specialized system engineered to handle the movement of this material from storage or processing units to subsequent stages of production. Such systems are vital in industries like cement manufacturing, chemical processing, and construction material production, where consistent and safe material transfer is essential for operational efficiency.
The design of a calcined limestone material conveying line involves several critical components, each playing a specific role in the overall functionality. The primary components typically include feed hoppers, conveyor belts or screw conveyors, control systems, and dust suppression mechanisms. The feed hopper is responsible for storing and regulating the flow of calcined limestone, ensuring a steady supply to the conveyor system. Conveyor belts, often made from durable materials like rubber or specialized polymers, transport the material over long distances with minimal friction and wear. Screw conveyors, on the other hand, are ideal for vertical or inclined transport, providing flexibility in system layout. Control systems, equipped with sensors and automation features, monitor the flow rate, temperature, and pressure, maintaining optimal operational conditions. Dust suppression mechanisms, such as water sprayers or enclosed housing, are integrated to prevent dust emissions, ensuring compliance with environmental regulations and worker safety.
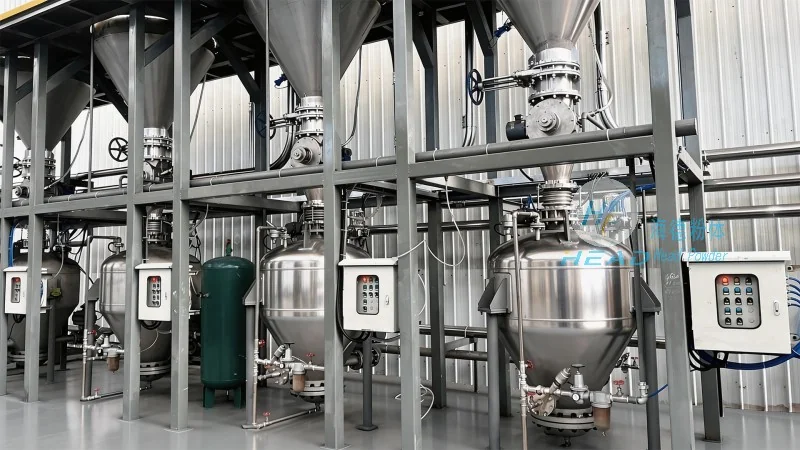
One of the key advantages of a calcined limestone material conveying line is its ability to enhance operational efficiency by reducing manual labor and minimizing material loss. The system's design allows for continuous material flow, which is particularly beneficial in high-demand production environments. The conveyor system can handle large volumes of calcined limestone, with capacities ranging from several tons per hour to hundreds of tons, depending on the specific application. The material handling capabilities are further enhanced by the system's ability to maintain consistent material quality, as the enclosed design prevents contamination from external sources. Additionally, the system's low maintenance requirements contribute to long-term cost savings, as fewer breakdowns and repairs are needed compared to traditional manual handling methods.
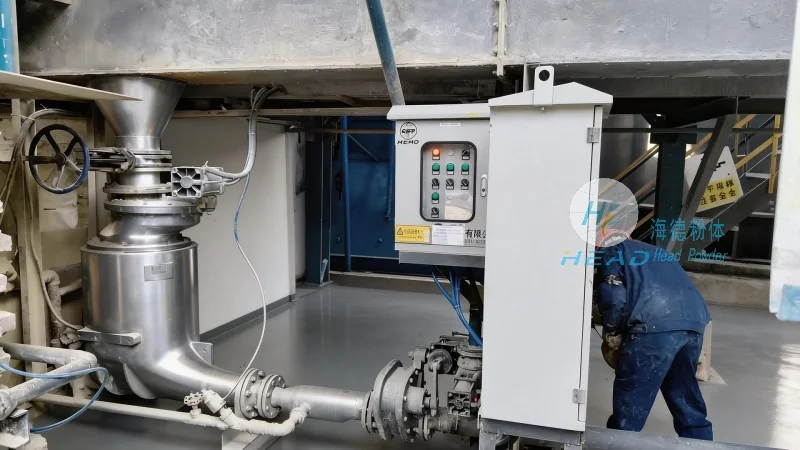
Calcined limestone material conveying lines are highly customizable to meet the specific needs of different industrial applications. Manufacturers can tailor the system's components, such as the type of conveyor (belt or screw), the length and inclination of the system, and the control system features, to suit the unique requirements of a facility. For example, in cement plants, the system may be designed to handle large quantities of calcined limestone from storage silos to the raw material grinding unit. In chemical processing facilities, the system can be adapted to transport calcined limestone to reactors or mixing tanks, ensuring precise material dosing. The flexibility of the system also allows for integration with other production equipment, such as crushers or classifiers, to form a comprehensive material handling solution. This customization ensures that the system operates efficiently and effectively within the specific industrial setting, maximizing productivity and minimizing downtime.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial material handling solutions, specializes in designing and manufacturing calcined limestone material conveying lines tailored to the needs of various industries. With a strong commitment to quality and innovation, the company has established itself as a trusted partner in the field of material handling equipment. HeadPowder's team of experienced engineers and technicians work closely with clients to understand their specific requirements and develop customized solutions that meet their operational needs. The company's facilities are equipped with advanced manufacturing technologies and quality control systems, ensuring that each product meets the highest standards of performance and reliability. HeadPowder's products are known for their durability, efficiency, and ease of maintenance, making them a preferred choice for industrial facilities worldwide. The company's headquarters is located in Shandong, China, where it continues to expand its capabilities and serve a growing number of clients in the global market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top