

Working Principle and Features of Phosphate Powder Pneumatic Conveying Equipment
Phosphate fertilizer powder is a critical raw material in the agricultural industry, and efficient handling of this material is essential for maintaining production efficiency and product quality. Pneumatic conveying systems have become a preferred solution for transporting phosphate powder due to their ability to handle fine powders with minimal dust generation and high transport efficiency. This article explores the working principle and key features of phosphate powder pneumatic conveying equipment, providing insights into how these systems operate and their advantages in industrial applications.
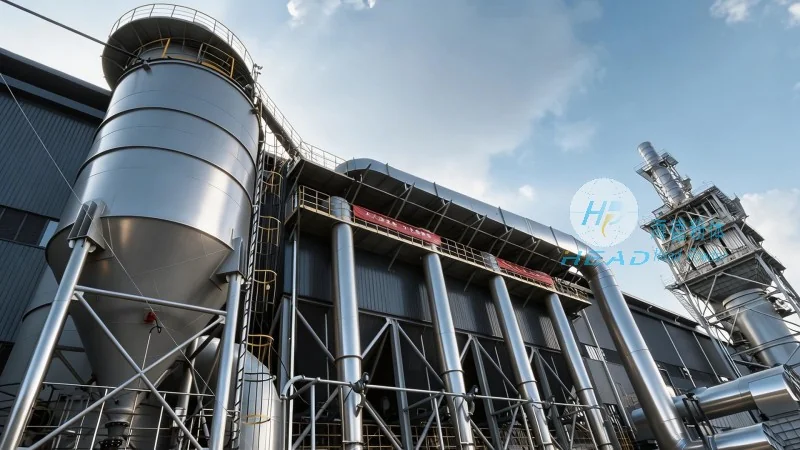
Working Principle of Phosphate Powder Pneumatic Conveying Equipment
The core of a phosphate powder pneumatic conveying system is the use of air as the conveying medium to transport the powder from the source to the destination. The process typically involves several key components, including a material feed hopper, a rotary valve or feeder, a conveying line, and a receiver or discharge point. The working principle can be broken down into the following steps: First, the phosphate powder is fed into the system through the hopper and feeder, which ensures a consistent and controlled flow of material. Next, a fan or blower generates a high-velocity air stream within the conveying line. As the powder is introduced into the air stream, it becomes entrained and is carried along the pipeline to the receiving container. The air and powder mixture is then separated at the receiver, where the powder is deposited and the air is either filtered and recirculated or vented to the atmosphere. This continuous cycle allows for the efficient and reliable transport of phosphate powder over varying distances and heights.
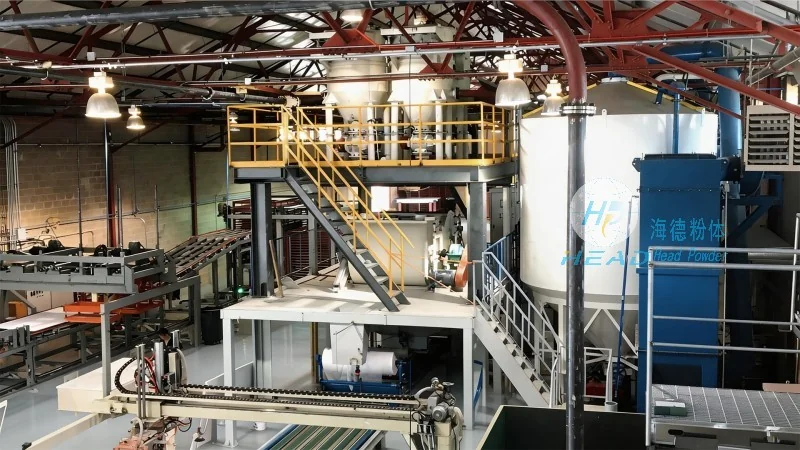
Key Features of Phosphate Powder Pneumatic Conveying Equipment
Phosphate powder pneumatic conveying equipment offers several advantages that make it suitable for industrial applications. One of the primary features is its ability to handle fine and abrasive powders without causing excessive wear on components. The system is designed with materials that resist corrosion and abrasion, ensuring long-term durability. Another important feature is the low dust generation, which is crucial for maintaining a safe and clean working environment. The enclosed system design minimizes the risk of dust exposure and improves overall safety. Additionally, pneumatic conveying systems can transport materials over long distances and at varying elevations, making them versatile for different plant layouts. The flexibility in system design allows for customization based on the specific requirements of the phosphate processing plant, including varying flow rates and material types. The energy efficiency of these systems is also a notable feature, as they can optimize air usage to minimize operational costs while maintaining high transport capacity.
Applications and Benefits in Phosphate Processing
Phosphate powder pneumatic conveying equipment is widely used in various stages of phosphate processing, from raw material handling to finished product packaging. In the raw material handling stage, the system efficiently transports phosphate ore from storage silos to grinding mills, ensuring a continuous supply of material for processing. During the grinding and classification process, the equipment transports the fine phosphate powder to the next stage of production, such as drying or coating. In the final stages, the system conveys the finished phosphate fertilizer to storage silos or packaging lines, maintaining product integrity and preventing contamination. The benefits of using pneumatic conveying systems in these applications include improved process control, reduced downtime due to material blockages, and enhanced safety by minimizing dust exposure. The consistent flow of material also helps in maintaining uniform product quality, which is critical for meeting market standards and customer expectations.
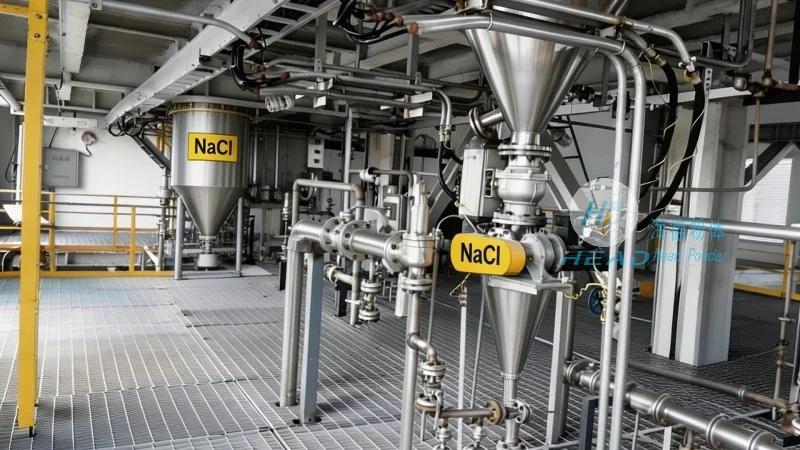
Conclusion
Phosphate powder pneumatic conveying equipment is a sophisticated and efficient solution for handling fine powders in the agricultural and chemical industries. By understanding the working principle and key features of these systems, industries can make informed decisions about implementing such technology to enhance their production processes. The combination of high transport efficiency, low dust generation, and flexibility makes pneumatic conveying an ideal choice for phosphate powder handling. As the demand for phosphate fertilizer continues to grow, the adoption of advanced pneumatic conveying systems will play a crucial role in meeting production needs while maintaining operational efficiency and safety standards. Shandong HeadPowder Engineering Co., Ltd., with its expertise in engineering and manufacturing, provides reliable solutions for phosphate powder pneumatic conveying equipment, supporting the needs of the industry with high-quality and durable systems.