

Working Principle and Features of the Air-Driven Transport Equipment for Manganese Sulfate
When it comes to the efficient and reliable transport of manganese sulfate, the air-driven transport equipment from Shandong HeadPowder Engineering Co., Ltd. stands out as a sophisticated solution. This equipment is designed to handle the unique challenges associated with transporting this chemical, ensuring a smooth and safe operation. The following sections will delve into the working principle and key features of this air-pneumatic transport system.
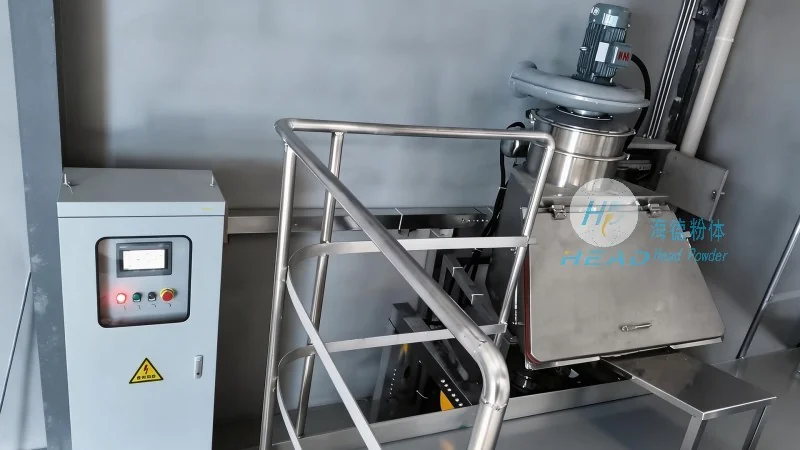
Working Principle of the Air-Driven Transport Equipment
The air-driven transport equipment for manganese sulfate operates on the principle of pneumatic conveying, which utilizes compressed air to move the material through a pipeline system. The process begins with the material being fed into a hopper or feeder, where it is then introduced into the conveying line. Compressed air, typically generated by a blower or compressor, is introduced into the pipeline, creating a flow that propels the material forward. The air flow is carefully controlled to maintain the appropriate velocity and pressure, ensuring that the material is transported without clogging or degradation. The system may include various components such as rotary valves, filters, and dust collectors to manage the flow and maintain air quality. The entire process is automated, allowing for consistent and continuous operation, which is crucial for industrial applications.
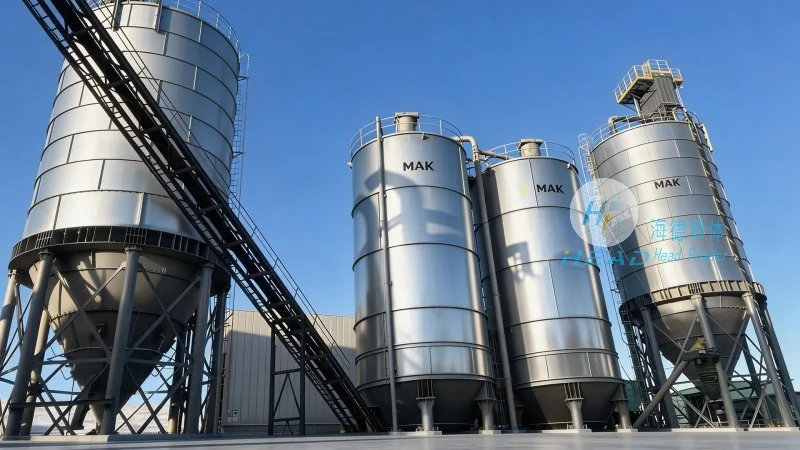
Key Features of the Air-Driven Transport Equipment
The air-driven transport equipment for manganese sulfate from Shandong HeadPowder Engineering Co., Ltd. offers several notable features that enhance its performance and usability. Firstly, it provides a dust-free and enclosed transport solution, which is essential for maintaining a safe and clean working environment, especially when handling fine powders like manganese sulfate. The equipment is designed to minimize material loss and contamination, ensuring that the product remains in its original state throughout the transport process. Additionally, the system is highly flexible and can be easily integrated into existing production lines, allowing for seamless operation and minimal downtime. The air-pneumatic design also enables the equipment to handle a wide range of particle sizes and moisture content, making it suitable for various industrial applications. Furthermore, the equipment is equipped with advanced control systems that allow for precise regulation of air pressure and flow, ensuring optimal performance and energy efficiency. The robust construction of the equipment ensures durability and long-term reliability, reducing maintenance costs and increasing overall productivity.
Application and Benefits in Industrial Settings
In industrial settings, the air-driven transport equipment for manganese sulfate offers significant benefits. It enables the efficient transfer of material from storage to processing units, such as reactors or mixers, without the need for manual handling or traditional conveyor systems. This not only improves operational efficiency but also enhances safety by reducing the risk of accidents and exposure to dust. The enclosed system also helps in maintaining product quality by preventing contamination from external sources. The equipment is particularly useful in applications where the material needs to be transported over long distances or through multiple stages of processing. The ability to handle large volumes of material at a time further contributes to increased productivity and reduced labor costs. Overall, the air-driven transport equipment provides a reliable and cost-effective solution for the transport of manganese sulfate, making it an essential component in many industrial processes.
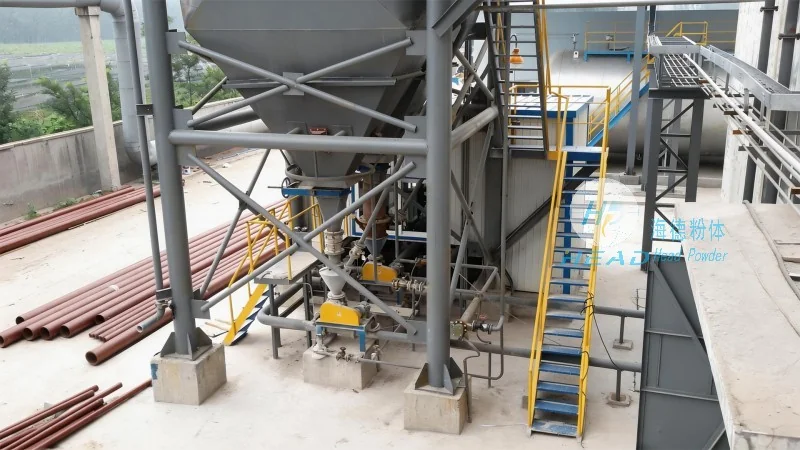
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of advanced powder handling equipment, including air-driven transport systems. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the chemical and industrial sectors. HeadPowder specializes in providing customized solutions tailored to the specific needs of its clients, ensuring that each equipment is designed to meet the unique requirements of the application. The company's commitment to research and development has led to the development of cutting-edge technologies that enhance the performance and efficiency of its products. Based in Shandong, China, HeadPowder leverages its local expertise and resources to deliver high-quality equipment that meets international standards. The company's team of experienced engineers and technicians ensures that each product is manufactured with precision and care, guaranteeing long-term reliability and customer satisfaction.