With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Chocolate processing is a complex and intricate process that involves multiple stages, from the sourcing of raw materials like cocoa beans to the final packaging of finished products. Among these stages, the efficient and reliable transportation of chocolate materials is a critical factor that directly impacts product quality, operational efficiency, and overall production costs. Pneumatic conveying equipment has gained significant traction in the chocolate industry due to its ability to handle fine powders and granules with minimal product degradation, ensuring that the final chocolate products retain their flavor, texture, and visual appeal. This article delves into the fundamental principles of chocolate material pneumatic conveying systems and outlines the key characteristics of their application in various industrial environments.
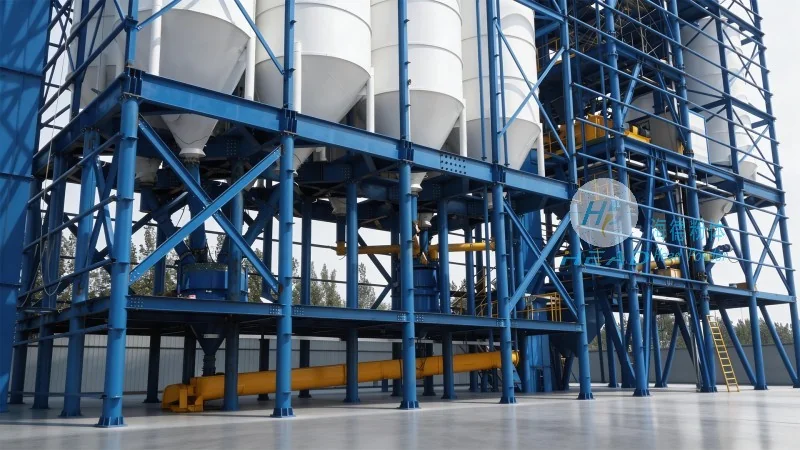
Pneumatic conveying systems operate on the principle of using air or gas to transport bulk materials through a closed pipeline network. For chocolate materials, which typically include cocoa powder, sugar, milk powder, and other flavoring agents, the equipment must be designed to handle materials that are sensitive to moisture, temperature changes, and mechanical stress. The core mechanism involves creating a pressure differential between the conveying line and the ambient environment. This is achieved through either positive pressure (where air is blown into the line to push material forward) or negative pressure (where air is drawn out to pull material into the line). In chocolate processing, positive pressure systems are generally preferred as they offer better control over material flow, reduce the risk of product degradation, and are more suitable for handling fine powders that are prone to caking. The system comprises several essential components: a hopper for material storage, a feeder to regulate the flow rate, a conveyor line (often equipped with bends and filters), and a receiver for the discharged material. The air flow is managed by a blower or vacuum pump, ensuring consistent material transport while maintaining low air velocity to prevent particle breakage. The design of the conveying line is critical; smooth inner surfaces and appropriate bend radii are used to minimize friction and product degradation. Additionally, filtration systems are integrated to capture fine particles and maintain air quality, which is vital for maintaining the hygienic standards required in chocolate production. Some advanced systems may also include vibration or agitation mechanisms within the hopper and feeder to prevent material buildup and ensure consistent flow, which is particularly important for chocolate materials that are prone to caking.
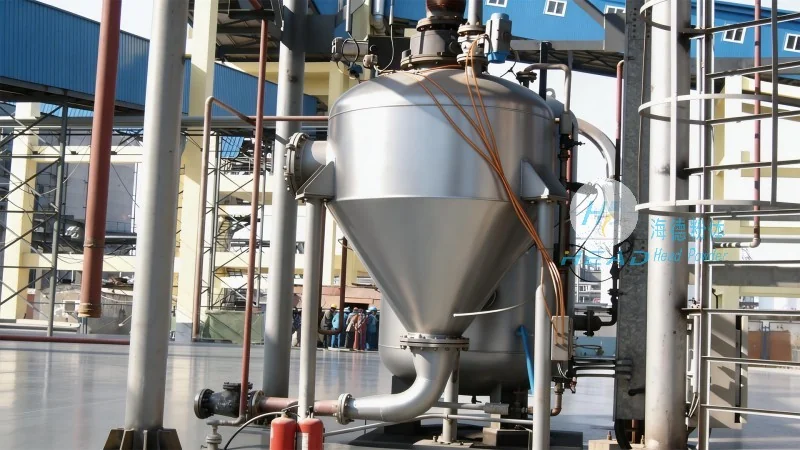
The application of chocolate material pneumatic conveying equipment varies across different industrial settings, each with distinct requirements and operational characteristics. In large-scale chocolate manufacturing plants, these systems are typically integrated into the production line to transport raw materials from storage silos to processing units such as mixers and refiners. The key characteristics in this setting include high throughput capacity, precise flow control, and compatibility with existing production infrastructure. For example, in a major chocolate factory, a positive pressure pneumatic conveyor can transport cocoa powder from a bulk storage silo to a mixing room at a rate of several tons per hour, ensuring a steady supply of raw material without manual handling. The equipment is also designed to handle variations in material density and moisture content, which are common in chocolate processing. Another important characteristic is the ability to operate in a clean and hygienic environment, as chocolate products are subject to strict food safety regulations. The conveying lines are often made of stainless steel, and the system includes self-cleaning mechanisms to prevent product buildup and contamination. In warehouse and storage facilities, pneumatic conveying equipment is used to move chocolate products between different storage areas or to loading docks. In this scenario, the equipment must be capable of handling bulk quantities and ensuring efficient inventory management. The working scene characteristics include durability, low maintenance requirements, and the ability to operate in varying ambient conditions. For instance, a negative pressure system can be employed to transfer finished chocolate products from a warehouse to a packaging line, reducing the need for manual handling and minimizing the risk of product damage. The equipment is also designed to be flexible, allowing for easy reconfiguration of the conveying network to accommodate changes in production volume or product types. Furthermore, in specialized applications such as the transport of chocolate-based ingredients to research and development labs, the equipment must provide precise control over material flow and maintain product purity. This requires advanced control systems and high-quality filtration to ensure that the transported materials meet the stringent quality standards required for experimental use. The equipment in this setting is often equipped with sensors and monitoring systems to track material flow and detect any deviations, ensuring that the process remains under tight control.
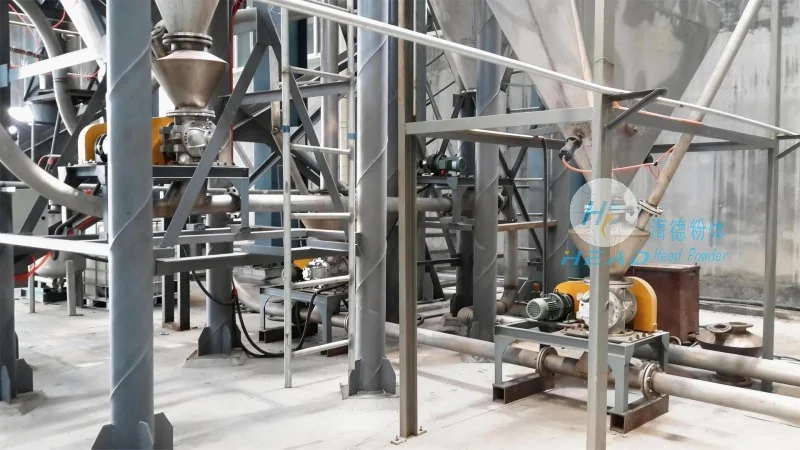
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of pneumatic conveying equipment specifically designed for the food and beverage industry, including the chocolate sector. With a strong focus on innovation and customer-centric solutions, the company has developed a comprehensive range of advanced systems that address the unique challenges of handling chocolate materials. HeadPowder's products are engineered to meet international food safety standards, such as FDA and HACCP, ensuring that the equipment is suitable for the production of high-quality chocolate products. The company's team of experienced engineers and technicians has extensive expertise in the design and implementation of pneumatic conveying systems, providing comprehensive support from initial consultation to on-site installation and maintenance. HeadPowder's manufacturing facilities are equipped with state-of-the-art equipment and rigorous quality control processes, ensuring that each product meets the highest standards of performance, reliability, and durability. The company's commitment to customer satisfaction is reflected in its comprehensive after-sales service, which includes regular maintenance, technical support, and readily available spare parts. By leveraging its deep understanding of material handling and process automation, HeadPowder has established itself as a trusted partner for chocolate manufacturers seeking to enhance their operational efficiency and product quality. The company's strategic location in Shandong, China, allows it to serve a wide range of clients across the country and internationally, providing tailored solutions that meet the specific needs of each customer. Whether for large-scale production lines or small-scale processing facilities, HeadPowder offers a range of pneumatic conveying equipment that is designed to deliver optimal performance and long-term durability, helping chocolate producers maintain their competitive edge in the global market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top