With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced powder conveying systems tailored for the barley malt industry. Our expertise lies in providing efficient and reliable solutions for handling barley malt powder, ensuring optimal performance in various production environments.
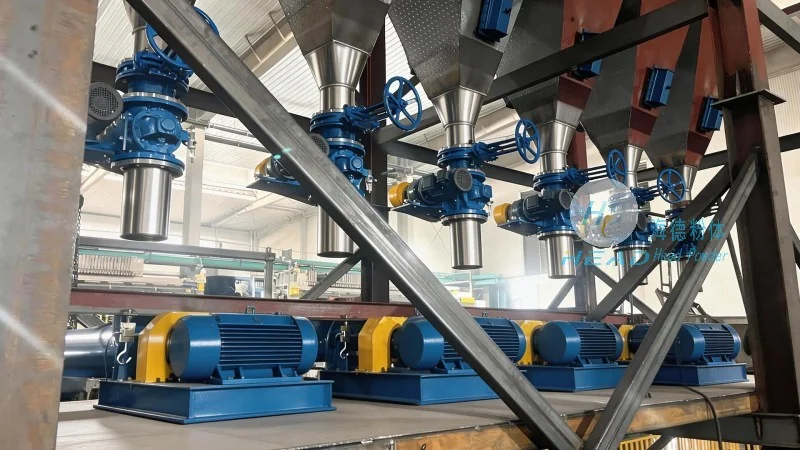
Barley malt powder conveying systems are critical components in the brewing and food processing industries, where the consistent and hygienic transport of malt powder is essential for maintaining product quality and production efficiency. These systems are engineered to handle the unique properties of barley malt, such as its fine particle size, moisture content, and susceptibility to caking or agglomeration. The design of a barley malt powder conveyor must address these challenges to ensure smooth operation and minimal product degradation.
The fundamental principle behind barley malt powder conveyors is the use of mechanical or pneumatic methods to move dry powder materials through a closed system. Mechanical conveyors, like screw conveyors or belt conveyors, utilize rotating components to push or pull the powder along a defined path. Pneumatic conveyors, on the other hand, employ compressed air to create a flow of air and powder, often using venturi or pressure vessels to transport the material. For barley malt, which requires gentle handling to preserve its flavor and texture, mechanical systems are often preferred due to their ability to minimize friction and impact on the powder particles.
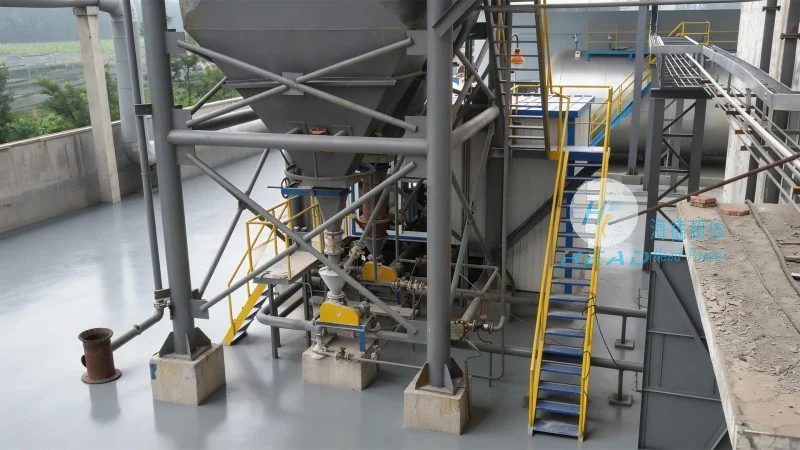
The working scene characteristics of barley malt powder conveyors are shaped by the specific requirements of malt production and processing. These systems are typically integrated into larger production lines, connecting raw material storage, milling, and blending stages. The design must accommodate the varying flow rates and batch sizes common in malt production, ensuring that the conveyor can handle both small-scale laboratory testing and large-scale industrial operations.
Hygiene and sanitation are paramount in the malt industry, as barley malt is used in food and beverage applications. Therefore, the conveyor systems are constructed from materials that are easy to clean and maintain, such as stainless steel, and are designed with smooth surfaces and minimal dead zones to prevent powder accumulation and contamination. Additionally, the systems are often equipped with dust collection and filtration systems to comply with environmental regulations and ensure a safe working environment for operators.
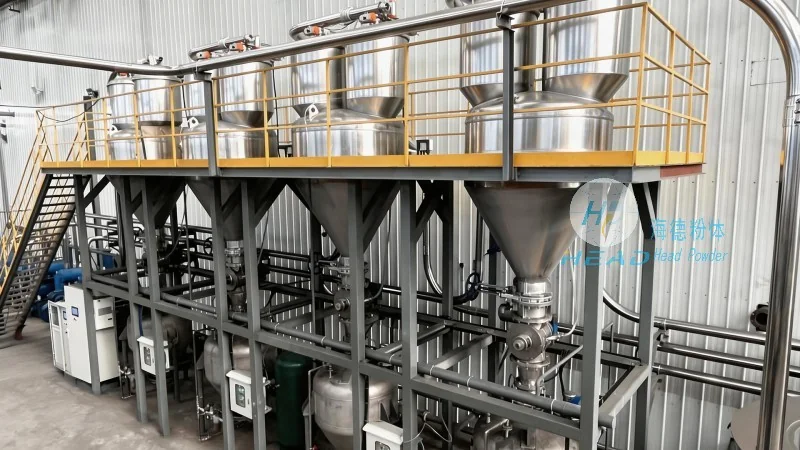
Barley malt powder conveyors are versatile and can be adapted to various working environments, from small-scale microbreweries to large-scale commercial breweries and malt production facilities. In microbreweries, the conveyor may be used to transport malt from storage bins to the mashing tanks, where precise dosing is crucial for achieving the desired wort composition. In commercial breweries, the system may handle larger volumes of malt, requiring higher capacity and more robust construction to meet the demands of continuous production.
In malt production facilities, the conveyor plays a key role in the entire process, from raw barley storage to the final malt product. It may be integrated with other equipment, such as malt mills and classifiers, to form a seamless production line. The ability to adjust the conveyor speed and flow rate allows operators to control the processing parameters, ensuring consistent malt quality and reducing waste.
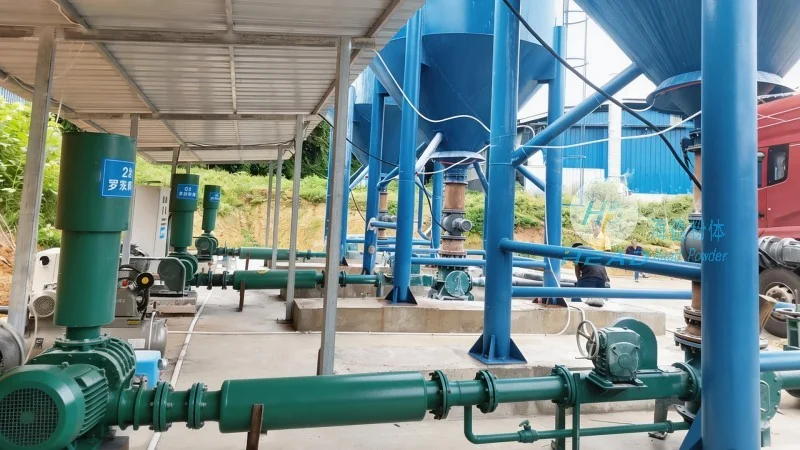
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, offers a range of barley malt powder conveying solutions that are tailored to meet the specific needs of each client. Our products are designed with the principles of efficiency, reliability, and hygiene in mind, ensuring that they can withstand the demands of daily operation in the malt industry. The company's commitment to quality and innovation has made it a trusted partner for breweries and malt producers worldwide.
Our conveyors are equipped with advanced control systems that allow for precise monitoring and adjustment of the conveying process. This includes features such as variable speed drives, flow sensors, and alarm systems to detect any issues and prevent product loss. The use of high-quality materials and robust construction ensures a long service life, reducing maintenance costs and downtime for our clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top