With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Ammonium bicarbonate, a white crystalline powder widely used in the food, pharmaceutical, and chemical industries, presents unique handling challenges due to its hygroscopic nature and fine particle size. Efficient and reliable powder conveying equipment is essential to maintain product quality and operational efficiency. This article explores the principle and working scene characteristics of a specialized conveying machine designed for ammonium bicarbonate, highlighting its design, operational mechanisms, and practical applications.
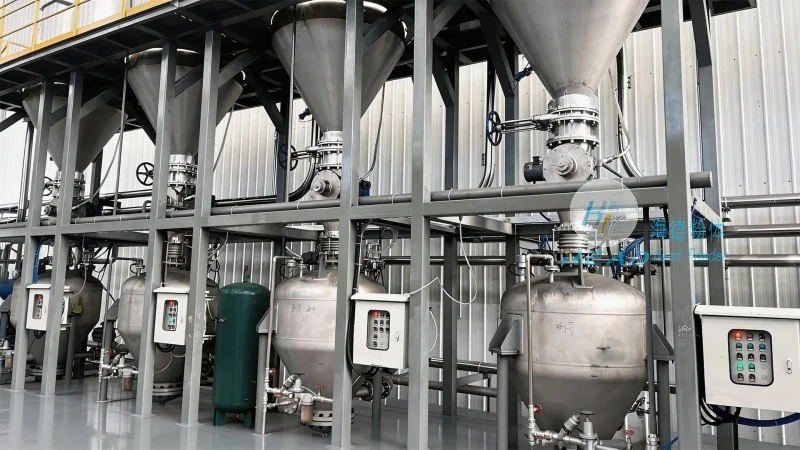
The conveying machine for ammonium bicarbonate operates on the principle of pneumatic or mechanical transport, tailored to address the specific properties of this material. The system typically combines positive displacement and air-assisted technologies to ensure gentle handling and minimal product degradation. Key components include a hopper for material storage, a rotary valve or feeder to control the flow rate, and a conveyor tube equipped with air distribution ports. The machine uses compressed air to create a low-pressure zone that draws the powder into the tube, where it is transported to the destination. This method minimizes friction and impact, which are critical for preserving the purity and stability of ammonium bicarbonate, especially in applications where moisture control is paramount.
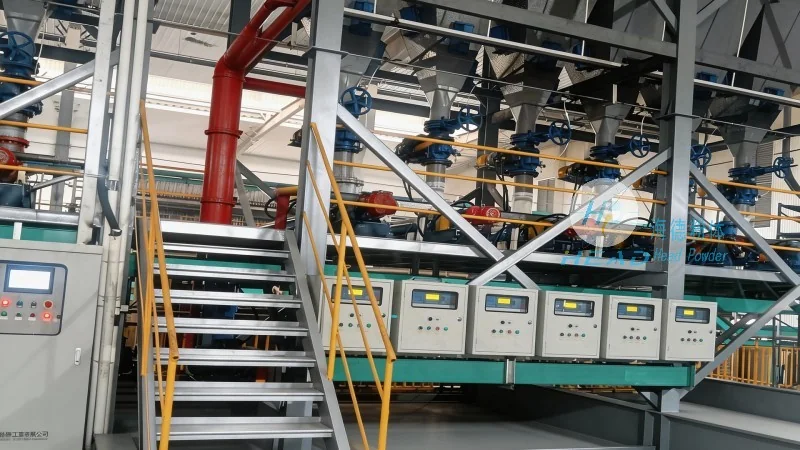
The working scene characteristics of the ammonium bicarbonate powder conveying machine are tailored to meet the demands of various industrial environments. In food processing facilities, the machine is used to transfer ammonium bicarbonate from bulk storage to production lines, ensuring a continuous and hygienic supply. The design incorporates stainless steel construction and food-grade materials to comply with regulatory standards, making it suitable for GMP (Good Manufacturing Practice) environments. In pharmaceutical manufacturing, the system is employed to handle raw materials for tablet and capsule production, where precision and contamination control are non-negotiable. The machine’s ability to maintain a consistent flow rate and prevent material segregation is particularly valuable in these settings. Additionally, in chemical processing plants, the conveying system is used to transport ammonium bicarbonate to reactors or mixing units, supporting processes such as fertilizer production or chemical synthesis. The machine’s adaptability to different operating pressures and flow rates allows it to integrate seamlessly with existing production lines, reducing downtime and increasing overall productivity.
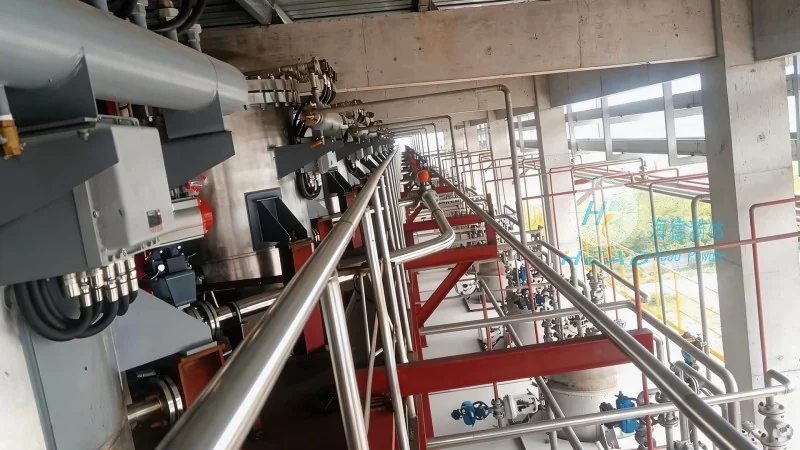
Several technical advantages distinguish the ammonium bicarbonate powder conveying machine from conventional systems. The use of air-assisted transport reduces the risk of material caking and blockages, which are common issues with hygroscopic powders. The machine’s low maintenance requirements, thanks to its robust construction and minimal moving parts, lower operational costs over time. Performance metrics, such as flow rate capacity and material handling efficiency, are optimized for ammonium bicarbonate’s specific characteristics. For example, the system can achieve a flow rate of up to 10 tons per hour while maintaining a particle size uniformity of ±5%, ensuring that the material meets the required specifications for downstream processes. The machine’s energy efficiency, with a power consumption of approximately 0.5 kW per ton of material, also contributes to cost savings and environmental sustainability.
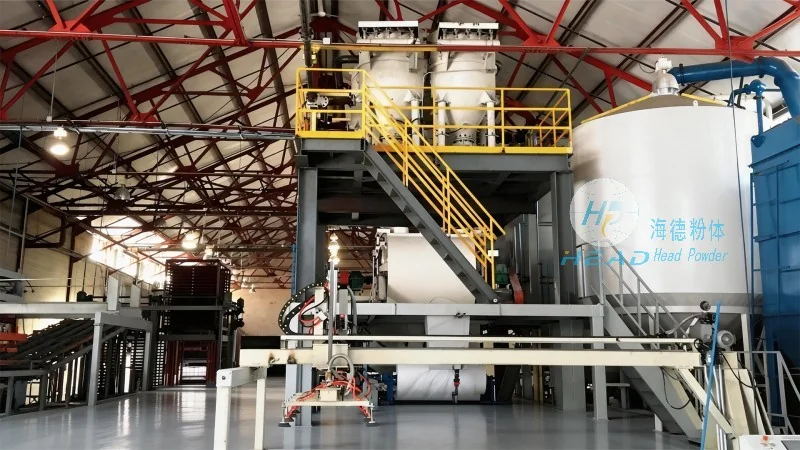
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of specialized powder handling equipment, provides the ammonium bicarbonate powder conveying machine. With a focus on innovation and customer-centric solutions, the company has developed a range of products tailored to the unique needs of the ammonium bicarbonate industry. The company’s headquarters is located in Shandong, China, where its team of engineers and technicians work to ensure the highest quality standards. HeadPowder offers comprehensive support services, including installation, maintenance, and technical training, to help clients maximize the performance of their conveying systems. The company’s commitment to quality and reliability has earned it a reputation as a trusted partner in the powder handling industry, serving clients worldwide with customized solutions that meet their specific requirements.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top